

Working Principle and Features of Intelligent Tonne Bag Loading Station Pneumatic Conveying Systems
Intelligent tonne bag loading stations equipped with pneumatic conveying systems represent a sophisticated solution for material handling in industrial settings. These systems are designed to efficiently transfer bulk materials from bulk bags (tonne bags) into processing equipment, storage silos, or other destinations. The integration of advanced automation and pneumatic technology ensures high efficiency, reliability, and safety in material transfer operations. This article explores the working principle and key features of such systems, highlighting their applications and benefits in modern industrial processes.
Working Principle of Pneumatic Conveying Systems in Tonne Bag Loading Stations
The core of a pneumatic conveying system for tonne bag loading involves the use of air to transport bulk materials. The process typically begins with the opening of a bulk bag, where the material is released into a hopper or feeder. From there, the material is drawn into a conveying line using either positive or negative pressure, depending on the system design. Positive pressure systems use a blower or compressor to push air and material through the pipeline, while negative pressure systems use a vacuum to pull material into the line. The material is then transported to the target location, such as a silo or processing unit, where it is discharged. The system often includes components like rotary valves, filters, and dust collectors to ensure smooth operation and maintain air quality. The control system, often integrated with sensors and automation, manages the entire process, ensuring precise material flow and preventing blockages or overfilling.
Key Features of Intelligent Tonne Bag Loading Station Pneumatic Conveying Systems
Intelligent tonne bag loading stations with pneumatic conveying systems offer several distinct features that enhance operational performance and user experience. One of the primary features is the integration of automation, which allows for unattended operation and reduces the need for manual intervention. This automation includes features like automatic bulk bag opening, material level sensing, and real-time monitoring of the conveying process. Another key feature is the ability to handle a wide range of materials, from powders and granules to bulk solids, with minimal adjustments to the system settings. The systems are also designed for high efficiency, with low energy consumption and minimal material loss during transfer. Safety features are integrated to prevent dust explosions and ensure operator safety, including explosion-proof components and emergency shutdown mechanisms. Additionally, the systems are equipped with maintenance-friendly designs, allowing for easy access to components for cleaning and repair. The user interface, often with a touchscreen display, provides clear monitoring and control options, enabling operators to adjust settings and troubleshoot issues quickly.
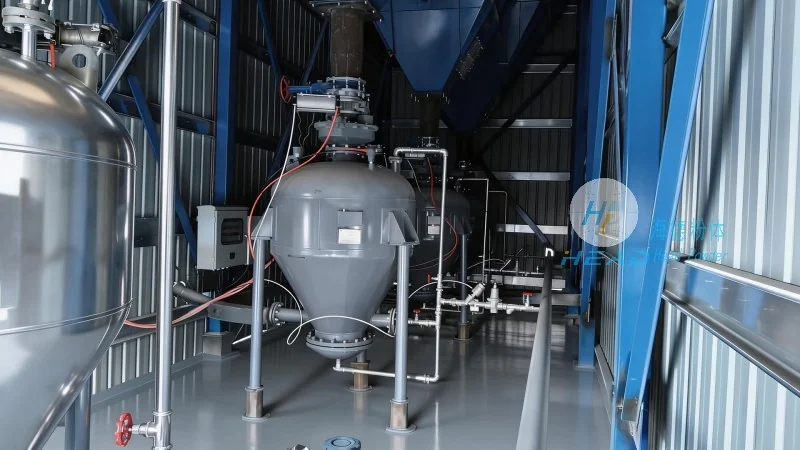
Applications and Benefits in Industrial Settings
Intelligent tonne bag loading stations with pneumatic conveying systems are widely used in various industries, including chemical, food, pharmaceutical, and mining. In the chemical industry, these systems are used to handle hazardous materials safely, with features like explosion-proof designs and sealed conveying lines. In the food industry, the systems are designed to maintain hygiene standards, with stainless steel components and easy-to-clean surfaces. The pharmaceutical industry benefits from the precision and cleanliness of the systems, ensuring that materials are transferred without contamination. The mining industry uses these systems to transport bulk ores and minerals from bulk bags to processing equipment. The primary benefits of these systems include increased productivity, reduced labor costs, improved material handling efficiency, and enhanced safety. The automation features reduce the risk of human error and improve consistency in material transfer. The energy-efficient design helps lower operational costs, making the systems cost-effective in the long run. Additionally, the compact design of some systems allows for installation in limited space, making them suitable for retrofitting in existing facilities.