

Working Principle and Features of Dust Collector Ash Pneumatic Conveying Systems
Efficient material handling is a critical aspect of modern industrial operations, particularly in processes involving dust collection and ash management. The pneumatic conveying system for dust collector ash, offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to enhance operational efficiency and safety. This article delves into the working principle and key features of this system, providing a comprehensive understanding of its functionality and benefits.
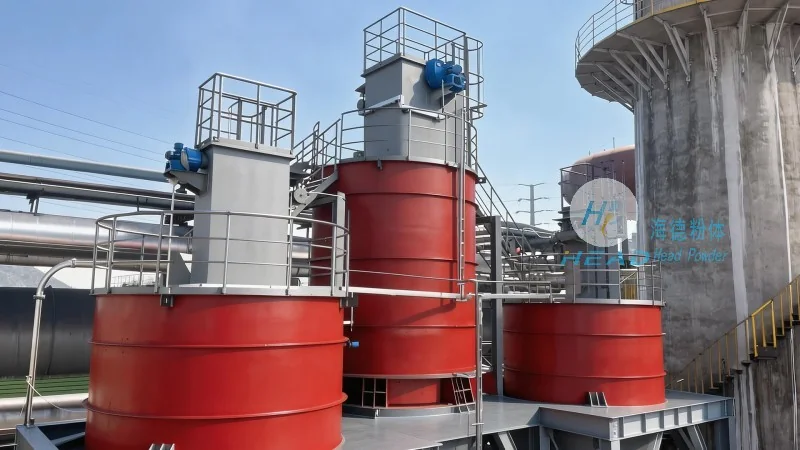
Understanding the Pneumatic Conveying System for Dust Collector Ash
The pneumatic conveying system for dust collector ash is engineered to transport collected ash from dust collectors to designated storage or disposal locations. This process is achieved through the use of compressed air or other gas, which creates a flow that moves the particulate material through a pipeline network. The system is designed to handle fine to medium-sized ash particles, ensuring reliable and consistent transport without the need for mechanical components like belts or buckets.
The Working Principle of the Pneumatic Conveying System
The core mechanism of the pneumatic conveying system involves the generation of a high-velocity air stream within the pipeline. This air stream is typically produced by a blower or compressor, which supplies the necessary pressure and volume to move the ash particles. As the ash enters the pipeline, it is entrained by the air flow, forming a suspension that travels through the system. The system may incorporate various components such as inlets, filters, and control valves to regulate the flow and ensure optimal performance. The ash is then discharged at the receiving end, where it can be collected and processed further.
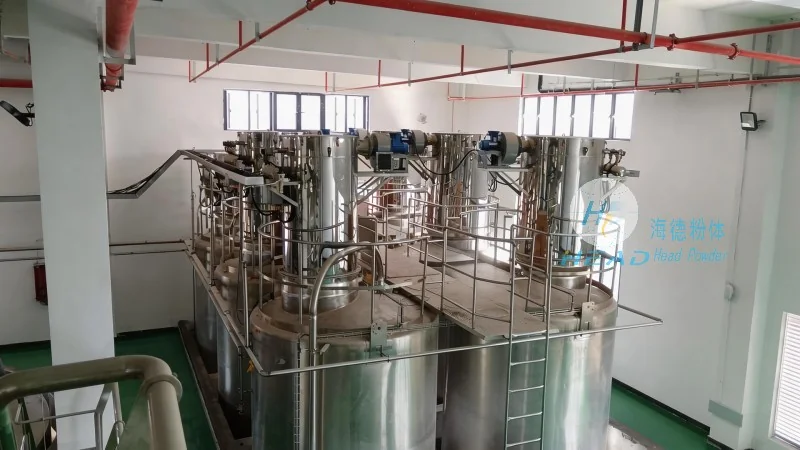
Key Features of the Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd. has developed several distinctive features that set their pneumatic conveying system apart in the industry. One of the primary advantages is the system's ability to handle abrasive and corrosive ash materials without significant wear or damage to components. This is achieved through the use of high-quality materials, such as stainless steel or specialized coatings, which enhance durability and longevity. Additionally, the system is equipped with advanced control systems that allow for precise regulation of air pressure and flow rates, ensuring consistent and efficient transport.
Another notable feature is the system's compact design, which minimizes space requirements and integrates seamlessly into existing industrial layouts. This design also contributes to reduced energy consumption, as the system operates efficiently with minimal power input. The system is further enhanced by its low maintenance requirements, thanks to the absence of moving parts that are prone to wear and tear. This results in lower operational costs and increased reliability over time.
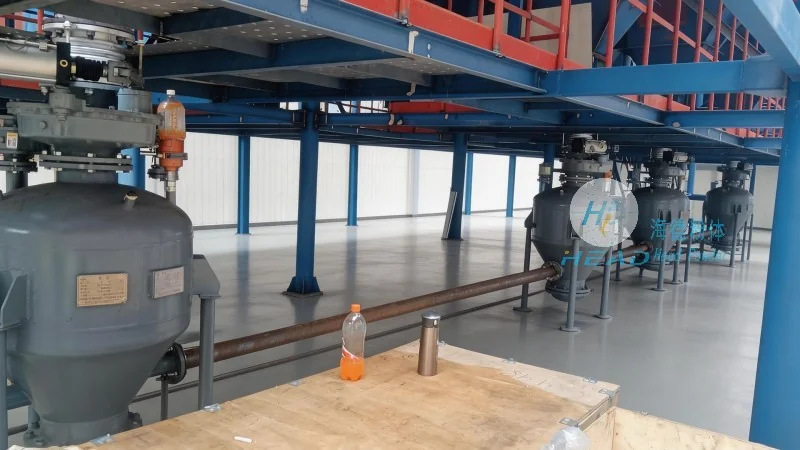
Benefits of Implementing a Pneumatic Conveying System
Adopting a pneumatic conveying system for dust collector ash offers numerous benefits for industrial operations. Firstly, it significantly improves safety by eliminating the need for manual handling of ash, which can be hazardous due to its fine particle size and potential for dust explosions. The system also reduces the risk of cross-contamination, as the ash is contained within the pipeline and does not come into contact with the external environment. Furthermore, the system enhances operational efficiency by automating the transport process, allowing for continuous and uninterrupted ash removal from dust collectors.
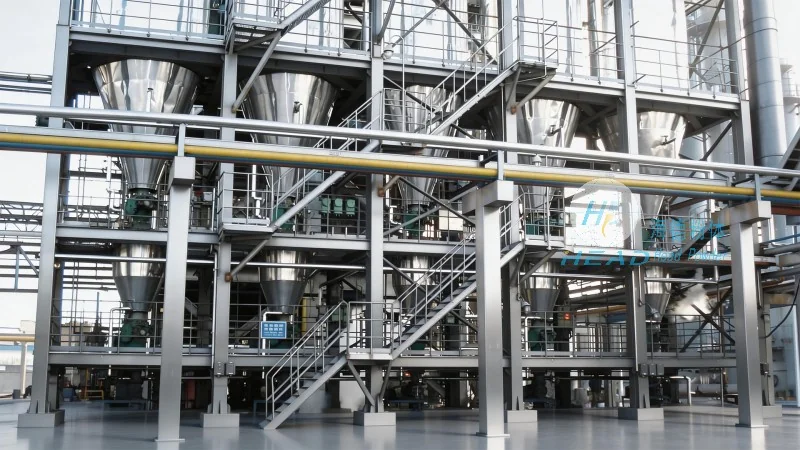
From an environmental perspective, the pneumatic conveying system helps to minimize dust emissions during the transport process, contributing to better air quality and compliance with environmental regulations. The system also facilitates better ash management by ensuring that the material is transported to designated storage or disposal facilities in a controlled manner. This leads to improved overall waste management practices and reduced environmental impact.
Conclusion
The pneumatic conveying system for dust collector ash, developed by Shandong HeadPowder Engineering Co., Ltd., represents a cutting-edge solution for efficient ash handling in industrial settings. By understanding its working principle and key features, businesses can make informed decisions about implementing this technology to enhance their operational performance and safety standards. With its robust design, advanced control systems, and environmental benefits, this system is a valuable asset for any facility dealing with dust collector ash management.