

What is a Coal Coke Powder Pneumatic Conveyor? What Are Its Design Principles?
For industrial applications that involve the handling of coal and coke powders, efficient and reliable material transport is crucial. A key piece of equipment in this field is the coal coke powder pneumatic conveyor, which utilizes air pressure to move powders through a pipeline system. This article will explore what a coal coke powder pneumatic conveyor is and delve into its fundamental design principles.
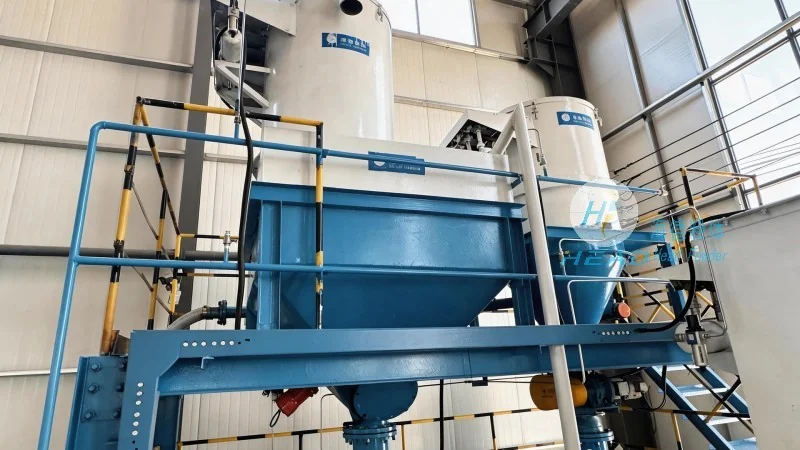
Understanding the Coal Coke Powder Pneumatic Conveyor
The coal coke powder pneumatic conveyor is a specialized pneumatic conveying system designed for transporting fine powders such as coal and coke. Unlike traditional mechanical conveyors that rely on belts or screws, this system employs compressed air as the primary means of material transport. This approach offers several advantages, including the ability to move materials over long distances, the prevention of dust contamination, and the reduction of material degradation due to friction. The system is particularly suitable for applications where dust control is essential, such as in coal processing plants or coke production facilities.
Design Principles of the Coal Coke Powder Pneumatic Conveyor
The design of a coal coke powder pneumatic conveyor is based on several core principles to ensure optimal performance and efficiency. The primary principle is the use of differential pressure to move the powder. Compressed air is introduced into the system, creating a pressure difference between the inlet and outlet of the pipeline. This pressure difference propels the powder particles forward, while the air acts as a carrier medium. The system typically consists of a blower, a hopper for material storage, a pipeline network, and a discharge point. The blower generates the necessary air pressure, and the hopper feeds the powder into the pipeline. The pipeline is designed with appropriate diameters and bends to minimize pressure loss and maintain a consistent flow rate.
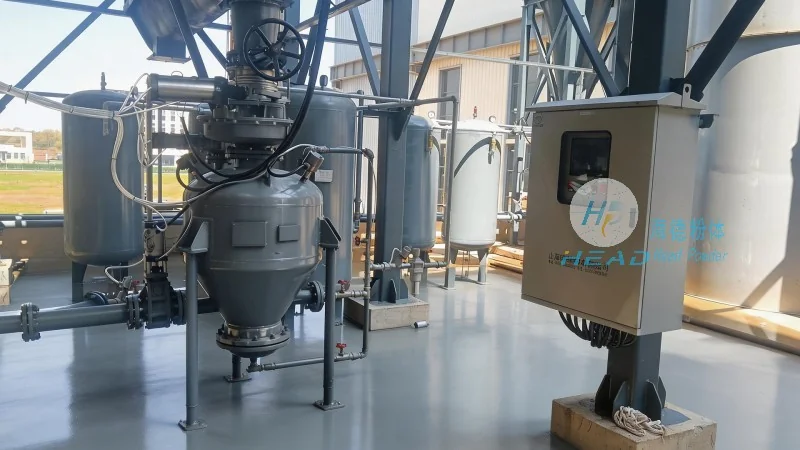
Key Components and Their Functions
Several key components work together to ensure the smooth operation of the coal coke powder pneumatic conveyor. The blower is the heart of the system, responsible for generating the compressed air that drives the material flow. It is typically a positive displacement blower or a centrifugal blower, chosen based on the required air volume and pressure. The hopper, or material feeder, is where the coal or coke powder is stored before being introduced into the pipeline. It is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, to control the flow rate of the material. The pipeline network connects the hopper to the discharge point and is constructed from materials that are resistant to corrosion and wear, such as stainless steel or special alloys. The discharge point is where the material is released from the system, often into a storage bin or processing equipment. Airlocks or rotary valves are used at the discharge point to control the flow and prevent backflow.
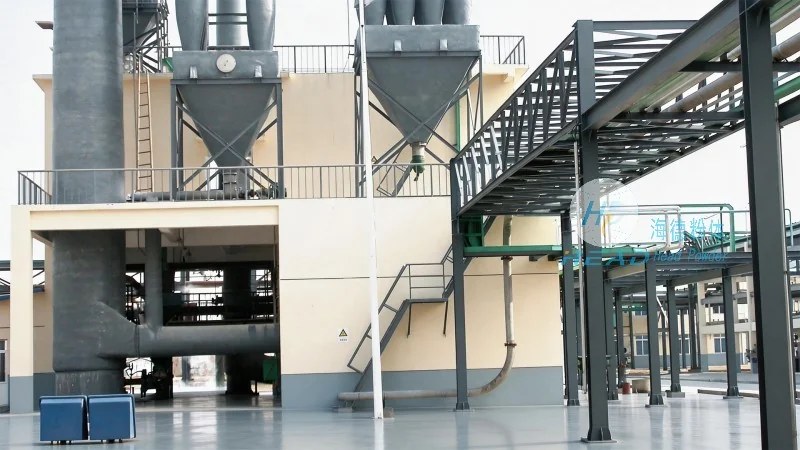
System Control and Operation
The operation of a coal coke powder pneumatic conveyor involves precise control of air pressure and material flow. The blower is typically equipped with a variable speed drive, allowing operators to adjust the air pressure according to the material being conveyed. This flexibility ensures that the system can handle different types of powders with varying properties, such as moisture content and particle size. The system also includes sensors and monitoring devices to track parameters like pressure, flow rate, and material level. These sensors provide real-time data to the control system, enabling operators to make adjustments and maintain optimal performance. The control system is designed to be user-friendly, with intuitive interfaces that allow for easy operation and maintenance.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the company name suggests, specializes in engineering solutions for powder handling and material transport. With a focus on providing high-quality equipment like the coal coke powder pneumatic conveyor, HeadPowder has established itself as a reliable partner in the industrial sector. The company is headquartered in Shandong, China, where it operates from its facilities, ensuring access to local resources and expertise. HeadPowder's commitment to quality and innovation is reflected in the design and manufacturing of its products, which are tailored to meet the specific needs of various industrial applications. The company adheres to strict quality control standards and uses advanced manufacturing techniques to ensure that its products meet or exceed industry requirements. HeadPowder also provides technical support and after-sales service to its customers, ensuring that the equipment operates efficiently and reliably throughout its service life.