

What is a Sugar Powder Pneumatic Conveying Machine? And What Are Its Design Principles?
In the sugar processing industry, efficient and reliable material handling is crucial for maintaining production efficiency and product quality. A key piece of equipment that addresses these needs is the sugar powder pneumatic conveying machine. This equipment is specifically designed to transport sugar powder through a pneumatic system, ensuring safe and effective movement of the material from one location to another within a processing facility.
Design Principles of Pneumatic Conveying Systems
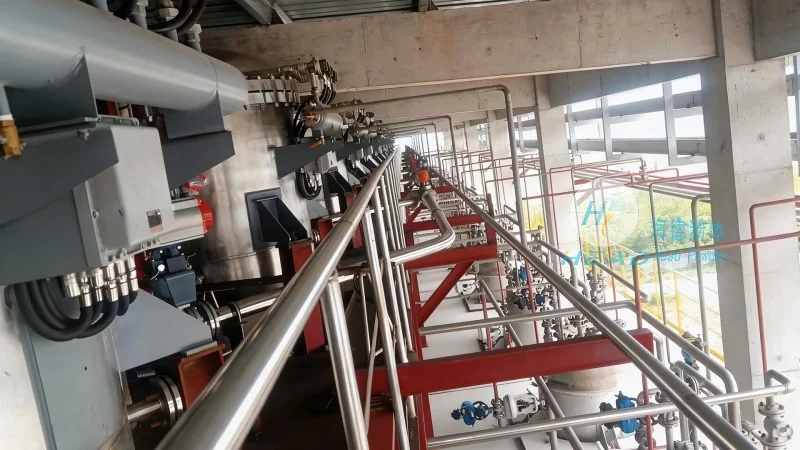
The design of a sugar powder pneumatic conveying machine is based on fundamental principles of fluid dynamics and material handling. At its core, the system uses compressed air or other gases to create a flow that propels the sugar powder through a pipeline. This approach eliminates the need for mechanical components like belts or screws, which can be prone to wear and maintenance issues. The design typically includes a hopper for material storage, a feeder to control the flow rate, and a pipeline network that connects the source and destination points. The choice of air velocity and pressure is critical, as it directly impacts the conveying capacity and the risk of material degradation or blockages.
Key Components and Their Functions
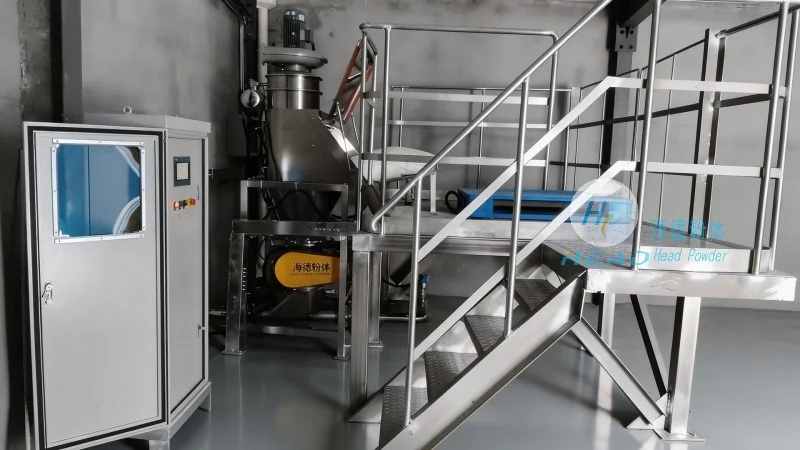
Several key components work together to ensure the smooth operation of a sugar powder pneumatic conveying machine. The hopper serves as the storage vessel, holding the sugar powder and providing a consistent feed to the system. The feeder, often a rotary valve or a metering device, regulates the flow of material into the pipeline, preventing overfeeding and ensuring a steady stream. The pipeline itself is usually made of materials like stainless steel or plastic, chosen for their resistance to corrosion and the ability to handle fine powders without clogging. The air compressor or blower generates the necessary pressure to move the material, while the control system monitors and adjusts the flow parameters to maintain optimal performance.

Advantages of Using Pneumatic Conveying for Sugar Powder
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages in the sugar industry. One of the most significant benefits is the ability to handle fine powders without the risk of segregation or bridging, which can occur with mechanical systems. This ensures that the sugar powder remains uniformly mixed and prevents the formation of clumps that could damage equipment or affect product quality. Additionally, pneumatic systems are more hygienic and easier to clean, which is essential in food processing environments. They also provide flexibility in terms of layout, as the pipeline can be arranged in various configurations to suit the specific needs of a facility, allowing for efficient use of space.
Application in Sugar Processing Facilities
Sugar powder pneumatic conveying machines are widely used in various stages of sugar processing, from raw material handling to final product packaging. In the raw material stage, they can transport sugar beets or cane juice concentrates to processing plants. During the refining process, they are used to move sugar crystals and powders between different processing units, such as crystallizers, centrifuges, and drying equipment. In the final packaging stage, they can transport finished sugar products to storage silos or shipping containers. The versatility of these machines makes them an essential part of modern sugar processing operations, enabling companies to streamline their production processes and improve overall efficiency.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
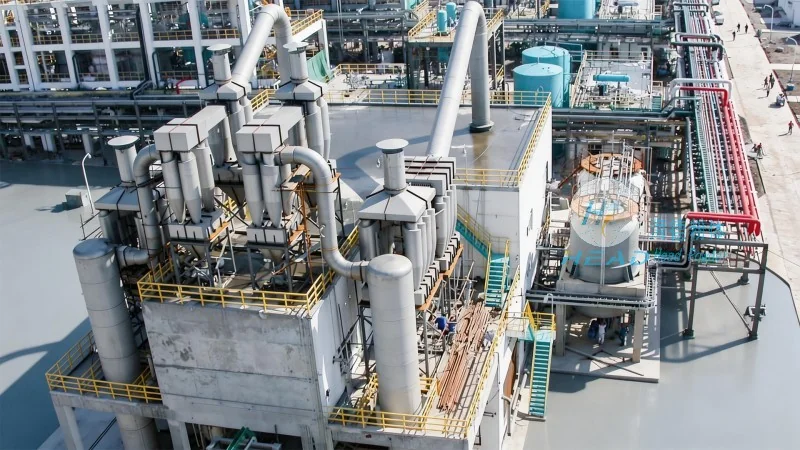
As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality sugar powder pneumatic conveying machines. With years of experience and a commitment to innovation, the company has developed advanced solutions that meet the specific needs of the sugar industry. Their products are engineered to ensure reliable performance, durability, and compliance with industry standards. The company’s headquarters is located in Shandong, China, where they have a team of skilled engineers and technicians dedicated to research and development. By partnering with HeadPowder, sugar processing facilities can benefit from cutting-edge technology and expert support to enhance their material handling capabilities.