

What is a Sintered Dust Ash Powder Pneumatic Conveying Line? And What Are Its Design Principles?
Sintered dust ash, also known as sintered fly ash, is a byproduct generated during the sintering process in steel and non-ferrous metal production. This material, rich in fine particles, poses challenges for handling and transportation due to its dusty nature and potential environmental impact. To address these challenges, industrial facilities employ specialized equipment known as sintered dust ash powder pneumatic conveying lines. These systems are designed to efficiently transport the fine powder over long distances while maintaining dust control and operational efficiency.
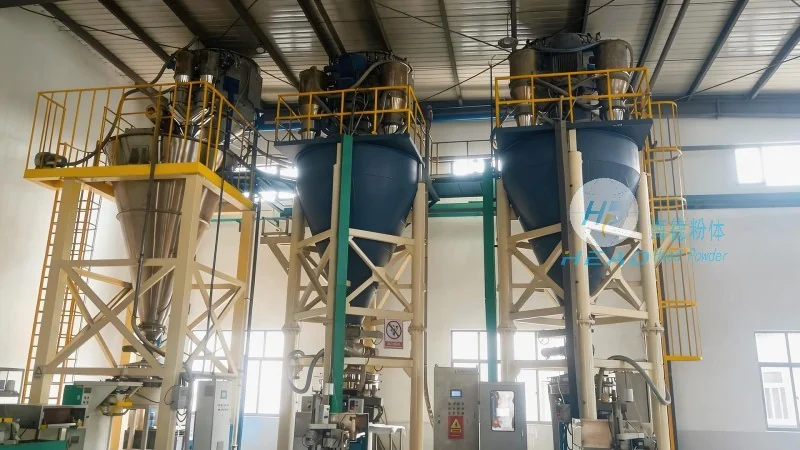
Understanding the Core Components of Pneumatic Conveying Systems
A typical sintered dust ash powder pneumatic conveying line consists of several key components that work in tandem to achieve effective material transport. The primary elements include a dust collector to capture and prepare the ash for transport, a conveying pipeline system (often made of stainless steel or other corrosion-resistant materials to handle the abrasive nature of the ash), a blower or compressor to generate the necessary air pressure, and a series of valves and controls to regulate the flow. Each component plays a critical role in ensuring the system operates smoothly and safely.
Design Principles for Efficient Material Handling
The design of a sintered dust ash powder pneumatic conveying line is guided by several fundamental principles aimed at optimizing performance and minimizing operational issues. First, the system must be capable of handling the high moisture content and abrasive properties of sintered dust ash without causing excessive wear or blockages. This often involves selecting appropriate materials for the pipeline and components, such as high-quality stainless steel or special alloys. Second, the system must maintain a consistent air flow rate to prevent material settling or clogging in the pipeline. Variable frequency drives (VFDs) and advanced control systems are commonly used to adjust the air pressure and flow dynamically based on the material load. Third, dust control is a critical design consideration. The system incorporates filtration and separation mechanisms to capture fine particles and prevent their release into the environment, ensuring compliance with environmental regulations.
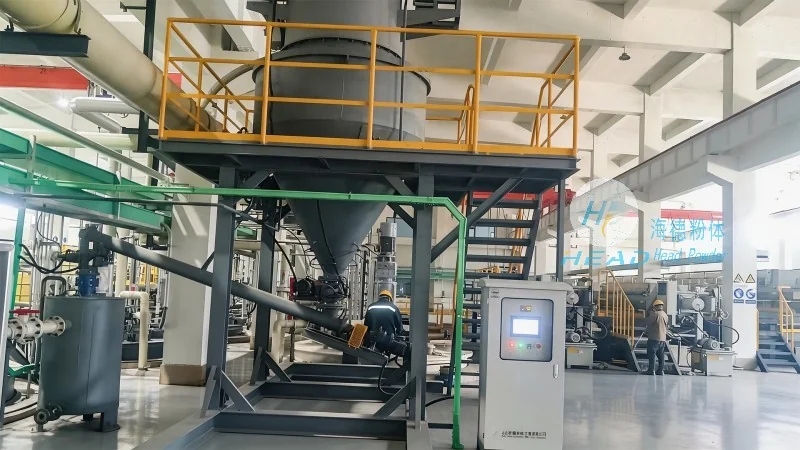
Key Advantages of Pneumatic Conveying for Sintered Dust Ash
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages for handling sintered dust ash. One of the most significant benefits is the ability to transport the material over long distances without the need for intermediate transfer points or manual handling. This reduces the risk of material loss and contamination. Additionally, pneumatic systems can handle materials with high moisture content and varying particle sizes, which is common in sintered dust ash. The enclosed pipeline design also minimizes dust emissions, improving workplace safety and reducing environmental impact. Furthermore, the flexibility of pneumatic conveying allows for easy integration with existing industrial processes, making it a cost-effective solution for many facilities.
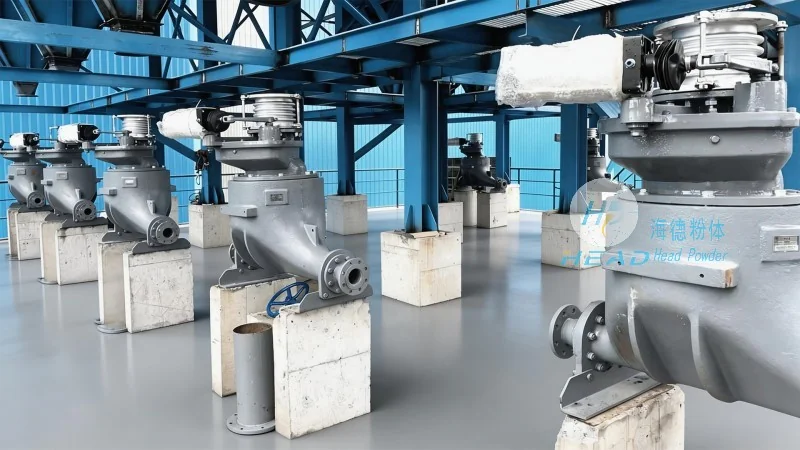
HeadPowder's Expertise in Sintered Dust Ash Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, specializes in designing and manufacturing customized sintered dust ash powder pneumatic conveying lines. With years of experience in the field, HeadPowder understands the unique challenges associated with handling sintered dust ash and has developed innovative solutions to address them. The company's team of engineers and technicians works closely with clients to assess their specific needs, from the volume of ash to be transported and the distance to the destination, and designs a system that meets all operational and regulatory requirements. HeadPowder's products are known for their durability, efficiency, and compliance with international standards, ensuring reliable performance in demanding industrial environments.
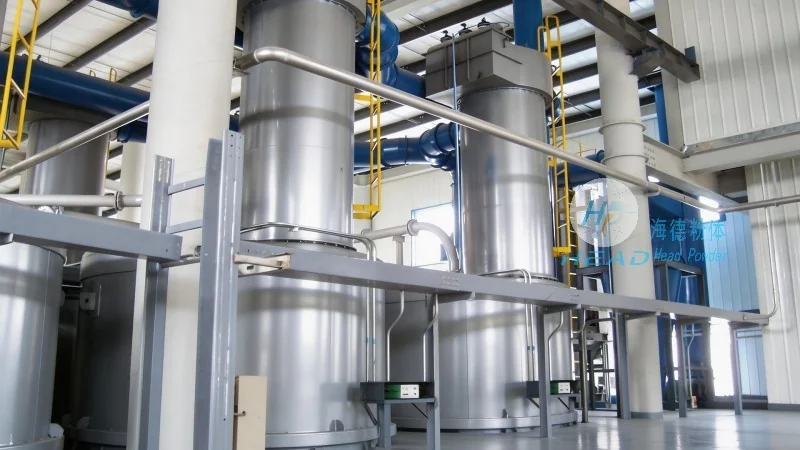
Customization and Integration Capabilities
HeadPowder recognizes that each industrial facility has unique requirements when it comes to sintered dust ash handling. Therefore, the company offers comprehensive customization options to tailor the pneumatic conveying line to the specific application. This includes selecting the appropriate blower type (positive displacement or centrifugal), determining the optimal pipeline diameter and length, and integrating additional features such as dust filtration systems or material storage tanks. The company also provides installation and commissioning services to ensure that the system is set up correctly and operates at peak efficiency from the start. By working closely with clients, HeadPowder ensures that the final solution not only meets but exceeds their expectations in terms of performance, reliability, and cost-effectiveness.
Conclusion: Enhancing Efficiency and Sustainability in Sintered Dust Ash Management
In conclusion, sintered dust ash powder pneumatic conveying lines are essential equipment for modern industrial facilities seeking to handle fine materials efficiently and safely. By understanding the design principles and advantages of these systems, companies can improve their operational efficiency, reduce environmental impact, and ensure compliance with regulatory standards. With its expertise and commitment to quality, Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner for businesses looking to implement effective sintered dust ash handling solutions. Whether for new installations or system upgrades, HeadPowder's customized pneumatic conveying lines provide reliable and sustainable solutions for the challenges of sintered dust ash management.