

What is Dust-Free Enclosed Powder Pneumatic Conveying? What Are Its Design Principles?
For industries dealing with bulk powders, maintaining a clean and safe working environment is paramount. Dust-Free Enclosed Powder Pneumatic Conveying systems offer an effective solution by transporting powders in a sealed, controlled environment, minimizing dust emissions and ensuring operational safety. This technology is crucial for sectors such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and worker health are critical. The design of these systems is tailored to handle various powder characteristics, ensuring efficient and reliable material transport while adhering to stringent industry standards.
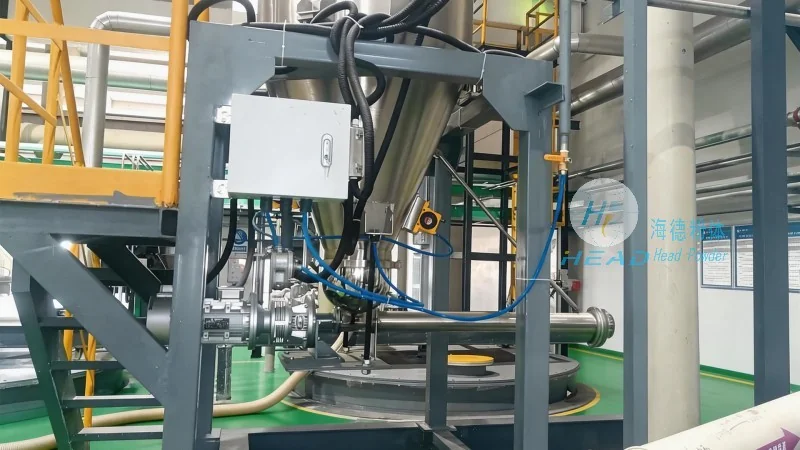
Key Design Principles of Dust-Free Enclosed Powder Pneumatic Conveying Systems
The core design principles of dust-free enclosed pneumatic conveying systems revolve around creating a closed loop that prevents powder leakage and airborne contamination. These systems typically operate under positive or negative pressure, depending on the application requirements. The key components include a hopper for powder storage, a conveyor line (often flexible or rigid), and a receiver for the discharged material. The design must consider factors like powder flowability, particle size distribution, and moisture content to optimize system performance. Additionally, the system incorporates filtration and cleaning mechanisms to maintain air quality and prevent dust accumulation, ensuring long-term operational efficiency.
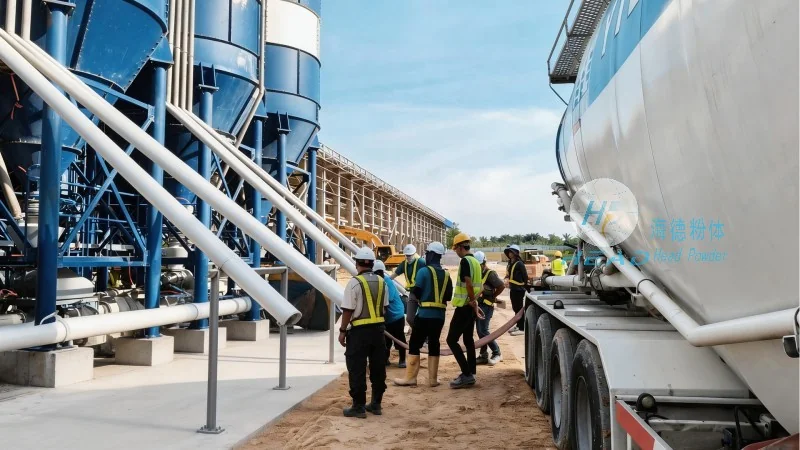
How the System Works: A Detailed Operational Overview
The operation of a dust-free enclosed powder pneumatic conveying system involves several critical steps. First, the powder is fed from the hopper into the conveyor line using a feeder, which may be a rotary valve or a screw feeder, depending on the powder's properties. The conveyor line then transports the powder to the receiver under controlled pressure. In positive pressure systems, the air is pressurized and carries the powder particles through the system, while negative pressure systems use suction to draw the powder into the line. The system's design ensures that all components are sealed to prevent any dust from escaping, with filters installed at the receiver and discharge points to capture any residual particles. This closed-loop operation not only enhances safety but also improves product quality by preventing contamination from external sources.
Benefits of Implementing Dust-Free Enclosed Powder Pneumatic Conveying
Adopting dust-free enclosed pneumatic conveying systems offers numerous advantages for industrial operations. Firstly, it significantly reduces dust exposure, improving workplace safety and compliance with environmental regulations. This is particularly important in industries where dust can pose health risks or cause product contamination. Secondly, the enclosed design enhances product purity, as it prevents cross-contamination between different batches of powder. This is critical in pharmaceutical and food industries where product integrity is non-negotiable. Thirdly, the system improves operational efficiency by minimizing downtime due to cleaning and maintenance, as the enclosed structure reduces the need for frequent cleaning of the entire system. Additionally, the flexibility of these systems allows for easy integration into existing production lines, making them a cost-effective solution for upgrading or modernizing material handling processes.
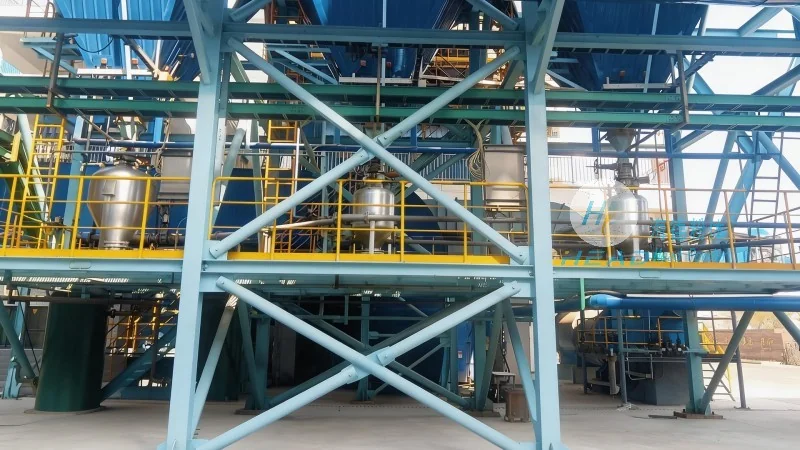
HeadPowder: Your Expert Partner in Dust-Free Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in designing and manufacturing high-quality dust-free enclosed powder pneumatic conveying systems. With years of experience in the industry, HeadPowder understands the unique challenges faced by different sectors and provides customized solutions tailored to specific needs. The company's team of engineers and technicians work closely with clients to assess their material handling requirements, ensuring that the final system meets all operational and safety standards. HeadPowder's products are known for their durability, efficiency, and compliance with international standards, making them a trusted choice for businesses seeking reliable and effective powder transport solutions. Whether for new installations or system upgrades, HeadPowder offers comprehensive support, from design and installation to maintenance and after-sales service, ensuring long-term satisfaction and operational success.