

What is a Floor Hopper Material Handling System? And Its Design Principles
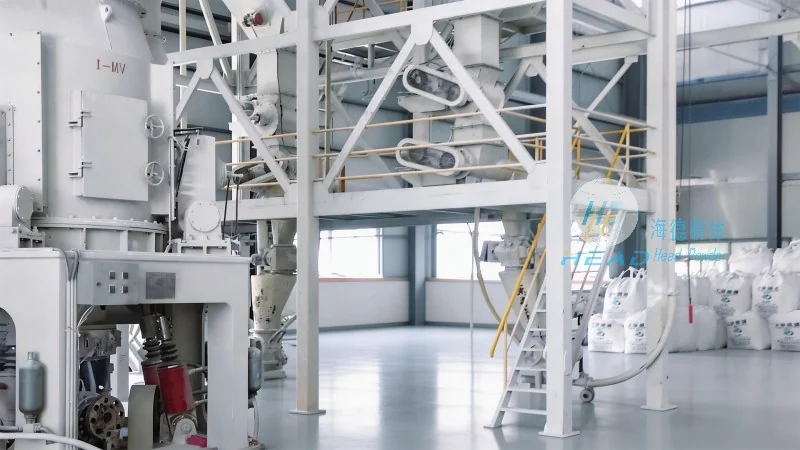
The floor hopper material handling system is a specialized industrial solution designed to efficiently manage and transport bulk materials within storage facilities. This system is particularly valuable in environments where large volumes of raw materials or finished goods need to be moved between different stages of production or storage. By integrating a hopper at the floor level, the system enables seamless material flow, reducing the need for manual handling and improving overall operational efficiency.
Key Components of a Floor Hopper Material Handling System
At the core of a floor hopper material handling system are several critical components that work in concert to ensure smooth material transfer. The primary component is the floor hopper itself, which is typically constructed from durable materials such as stainless steel or high-strength plastic to withstand heavy loads and harsh operating conditions. The hopper is designed with a sloped or conical shape to facilitate the natural flow of materials, minimizing the risk of clogging or material buildup. Additionally, the system includes a conveyor or transfer mechanism, such as a belt conveyor or screw conveyor, that connects the hopper to the next processing or storage area. This conveyor is often equipped with adjustable speed controls and safety features to ensure precise material movement and operator safety. Another essential component is the control system, which may include sensors, valves, and a programmable logic controller (PLC) to automate the material handling process. The control system allows for real-time monitoring and adjustment of the conveyor speed, ensuring that the flow of materials is optimized based on production demands.
Design Principles for Effective Material Handling
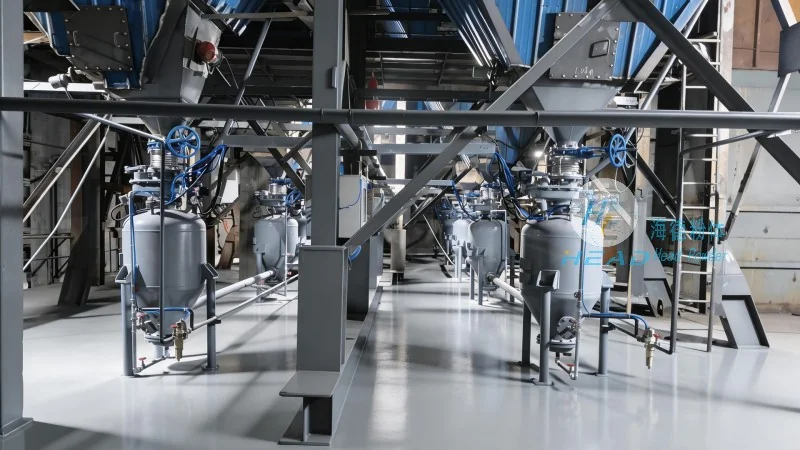
The design of a floor hopper material handling system follows several key principles to maximize efficiency and reliability. First, the system is engineered to minimize the need for manual intervention, reducing labor costs and the risk of human error. The hopper's design, with its self-contained material flow, ensures that materials move from the floor level directly into the conveyor, eliminating the need for manual loading or lifting. Second, the system prioritizes durability and longevity, with components constructed from materials that can withstand heavy usage and exposure to dust, moisture, or other environmental factors. This durability is crucial for maintaining consistent performance over time, especially in high-volume production environments. Third, the design emphasizes flexibility and adaptability, allowing the system to be integrated with existing production lines or modified to accommodate different material types or processing requirements. The modular nature of the components enables easy upgrades or changes without disrupting the entire operation. Fourth, the system incorporates safety features to protect both materials and personnel. This includes sensors that detect obstructions or overloads, emergency stop buttons, and enclosed conveyor sections to prevent accidental contact with moving parts. These safety measures are essential for maintaining a secure working environment and complying with industrial safety regulations.
Applications and Benefits of Floor Hopper Material Handling Systems
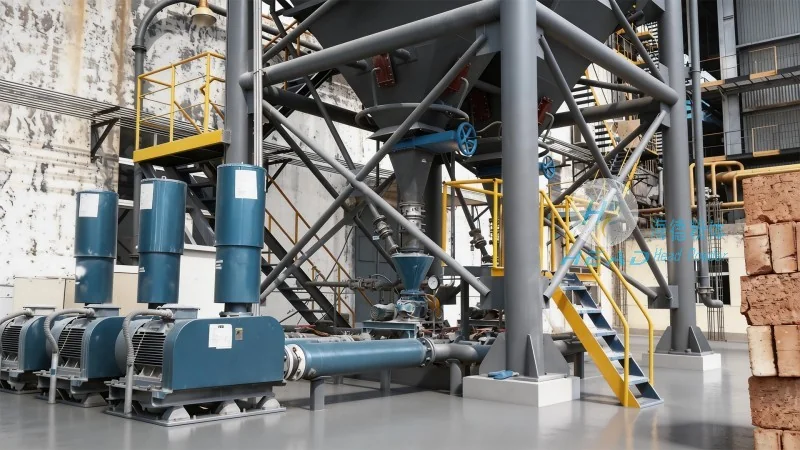
Floor hopper material handling systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and manufacturing. In the food industry, for example, these systems are used to transport bulk ingredients such as grains, powders, or spices from storage silos to production lines, ensuring a clean and efficient flow of materials. In pharmaceutical manufacturing, the system helps maintain strict hygiene standards by handling raw materials in a controlled environment, reducing the risk of contamination. The benefits of using a floor hopper material handling system extend beyond efficiency and safety. By automating material transfer, the system reduces labor costs and increases production throughput. It also minimizes material waste by ensuring that materials are transferred with minimal spillage or loss. Additionally, the system improves inventory management by providing a clear and consistent flow of materials, allowing for better tracking and control of stock levels. Overall, the floor hopper material handling system is a cost-effective and reliable solution for managing bulk materials in industrial settings.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the name suggests, is a leading provider of industrial material handling solutions, specializing in the design and manufacturing of floor hopper systems. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality, reliable equipment tailored to the needs of various industries. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and safe material handling solutions. HeadPowder's products are designed to meet international standards and are backed by a team of experienced engineers and technicians who provide comprehensive support, from installation to maintenance.