

What is a Bin Pump Powder Handling System? What is its Design Principle?
Bin pump powder handling systems are specialized industrial equipment designed to transport bulk powders over long distances with high efficiency and reliability. These systems are widely used in various industries, including chemical, pharmaceutical, food processing, and mining, where the safe and effective movement of powders is critical for operational success.
Understanding the Core Components of a Bin Pump System
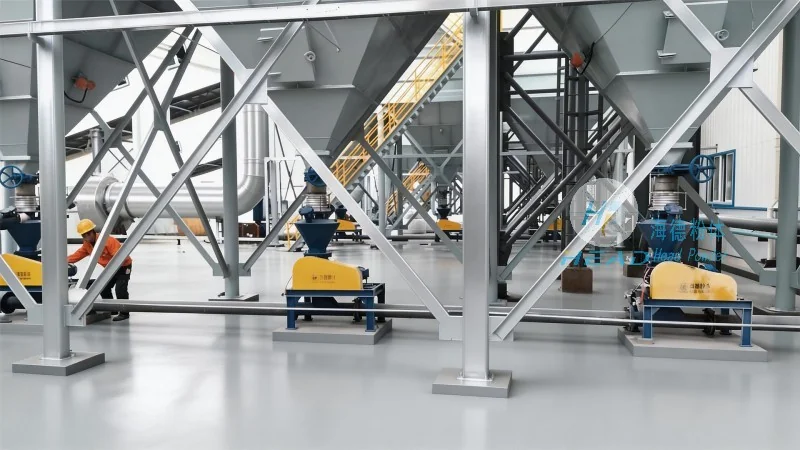
The bin pump system typically consists of several key components that work in tandem to achieve efficient powder transport. The primary elements include a storage hopper or bin, a pump mechanism, a conveying pipeline, and control systems. The storage hopper serves as the source of the powder, providing a consistent feed to the pump. The pump itself is the heart of the system, responsible for creating the pressure needed to move the powder through the pipeline. The conveying pipeline transports the powder from the source to the destination, often using flexible or rigid tubing depending on the application requirements. Control systems ensure the smooth operation of the pump, regulating flow rates and pressure to maintain optimal performance.
The Design Principle Behind Bin Pump Technology
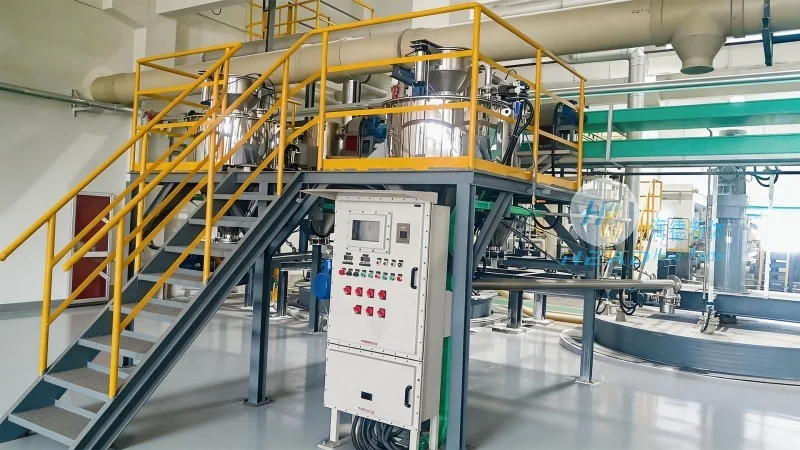
The design principle of a bin pump is centered on the concept of fluidization and pneumatic transport. Unlike traditional conveyor systems that rely on mechanical movement, bin pumps use compressed air or other gases to create a fluidized state within the powder. This fluidization allows the powder to behave like a fluid, enabling it to be pumped through the pipeline under pressure. The design incorporates several key factors to ensure effective operation: the hopper design to prevent material bridging or caking, the pump's ability to handle different powder characteristics (such as density, flowability, and moisture content), and the pipeline's configuration to minimize pressure drop and maintain consistent flow. Engineers carefully calculate the air-to-powder ratio, pipeline diameter, and pump speed to achieve the desired transport efficiency and minimize energy consumption.
Applications and Benefits of Bin Pump Systems
Bin pump systems are particularly advantageous in applications where traditional conveying methods are impractical or inefficient. For example, in the chemical industry, they are used to transport reactive powders over long distances without exposure to external contaminants. In the pharmaceutical sector, they ensure sterile and hygienic powder handling, meeting stringent regulatory requirements. The benefits of bin pump systems include high transport capacity, the ability to handle abrasive or corrosive powders, reduced maintenance compared to mechanical conveyors, and the flexibility to transport powders vertically, horizontally, or at various angles. These advantages make bin pump systems a preferred choice for industries requiring reliable and efficient bulk powder transport solutions.
About Shandong HeadPowder Engineering Co., Ltd.
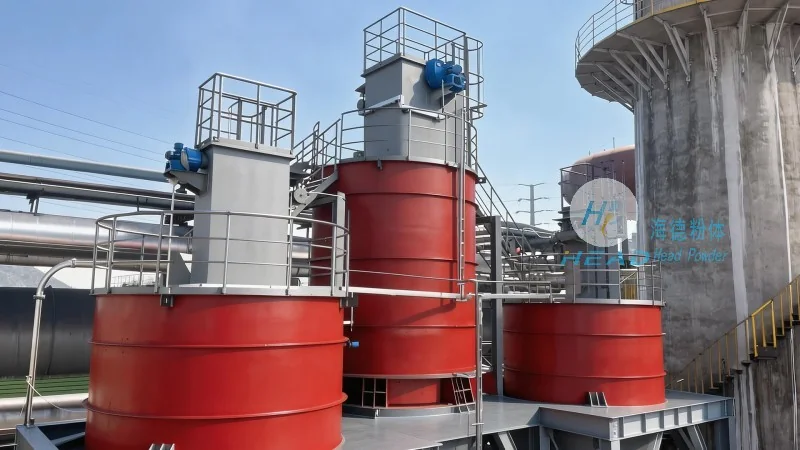
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling equipment. With a focus on innovation and quality, the company specializes in designing and producing bin pump systems tailored to the specific needs of various industries. HeadPowder's products are engineered to meet international standards and are known for their durability, efficiency, and user-friendly operation. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center. HeadPowder's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the global powder handling industry.