

What is a Multi-point Feeding Powder Conveying Machine? What are its Design Principles?
When it comes to efficient and reliable powder handling in industrial settings, the multi-point feeding powder conveying machine has emerged as a critical solution. This specialized equipment is designed to transport bulk powders from multiple feeding points to a central processing or storage location, ensuring smooth and consistent material flow. Understanding the functionality and design principles of such a machine is essential for industries that rely on precise powder management, including pharmaceuticals, food processing, and chemical manufacturing.
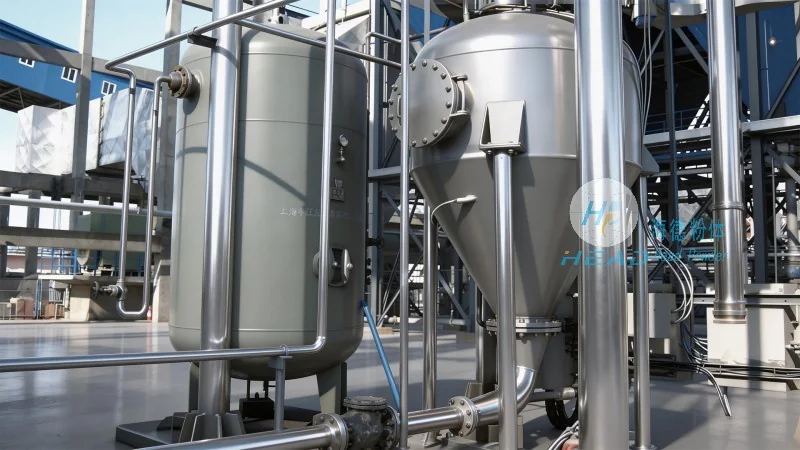
Introduction to Multi-point Feeding Powder Conveying Machines
A multi-point feeding powder conveying machine is a sophisticated system engineered to handle the transportation of powders from several source points simultaneously. Unlike traditional single-point feeding systems, this technology allows for the integration of multiple feed hoppers or silos, enabling the machine to draw material from various locations and combine them into a single conveying stream. This capability is particularly valuable in large-scale operations where multiple raw material sources are present, as it optimizes material usage and reduces downtime associated with material transfer.
Key Components and Design Principles
The design of a multi-point feeding powder conveying machine is built upon several key components that work in harmony to ensure efficient operation. The primary components include feed hoppers, a conveying system (such as a screw or pneumatic conveyor), a control unit, and a discharge mechanism. Each component plays a vital role in the overall functionality of the machine.
Feed hoppers are strategically positioned at each source point to collect and store the bulk powder. These hoppers are typically equipped with level sensors to monitor the material volume, ensuring that the machine can adjust its feeding rate based on the available material. The conveying system, which may be a screw conveyor or a pneumatic system, is responsible for transporting the powder from the feed hoppers to the central processing area. The control unit acts as the brain of the system, coordinating the operation of all components and maintaining the desired flow rate. Finally, the discharge mechanism delivers the combined powder to the next stage of the production process, such as a mixer or a storage silo.
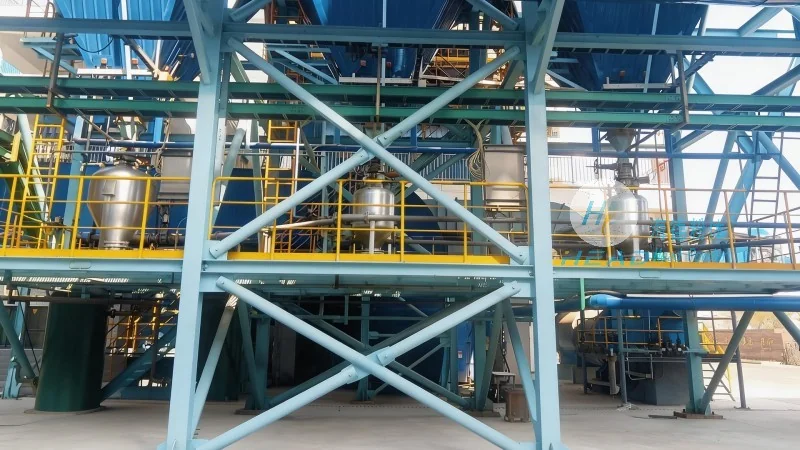
How the Design Principles Enhance Performance
The design principles of a multi-point feeding powder conveying machine are centered on maximizing efficiency, reliability, and flexibility. One of the core principles is the ability to handle multiple feed sources simultaneously, which reduces the need for manual intervention and minimizes the risk of material bottlenecks. This is achieved through advanced control systems that can monitor and adjust the feeding rate from each hopper in real-time, ensuring that the overall flow rate remains consistent.
Another critical design principle is the integration of material flow control mechanisms. These mechanisms, such as variable speed drives and flow regulators, allow the machine to adapt to changes in material characteristics, such as density or moisture content. This adaptability is crucial in industries where powder properties can vary, as it prevents clogging and ensures smooth operation. Additionally, the design emphasizes the use of high-quality materials for the construction of the feed hoppers and conveying components, which enhances durability and reduces maintenance requirements.
Applications and Benefits in Industrial Settings
The multi-point feeding powder conveying machine is widely used in various industrial applications due to its versatility and efficiency. In the pharmaceutical industry, for example, this equipment is essential for handling sensitive powders, as it ensures that the material is transferred without contamination or degradation. The precise control over the feeding rate and flow rate helps maintain the quality of the final product, which is critical in pharmaceutical manufacturing.
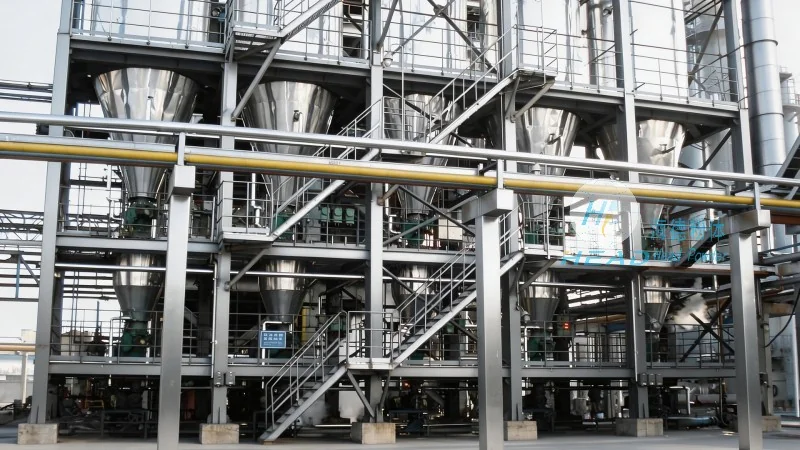
In the food processing industry, the machine is used to transport ingredients such as flour, sugar, and spices from multiple storage locations to a central mixing area. This not only improves the efficiency of the production line but also ensures that the ingredients are mixed in the correct proportions, resulting in consistent product quality. Similarly, in the chemical industry, the machine is used to handle bulk chemicals, which may be hazardous or reactive. The design of the machine, with its sealed and enclosed components, minimizes the risk of exposure and ensures safe operation.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and supply of high-quality multi-point feeding powder conveying machines. With years of experience in the industry, our team of engineers and technicians has developed a deep understanding of the needs of various industries, allowing us to provide customized solutions that meet specific requirements. Our company is committed to using advanced technology and high-quality materials to ensure that our products are reliable, efficient, and durable.
HeadPowder is dedicated to providing our customers with the best possible service, from initial consultation to after-sales support. We understand that each industrial setting is unique, and our team works closely with clients to develop solutions that address their specific challenges. Whether you are in the pharmaceutical, food processing, or chemical industry, we are here to help you optimize your powder handling processes and improve overall efficiency.