

What is a Food Powder Handling System? What are the Design Principles?
Understanding the fundamentals of food powder handling systems is crucial for industries that rely on efficient and safe transportation of powdered ingredients. These systems are designed to move bulk food powders from one location to another, ensuring optimal flow, minimal product degradation, and compliance with food safety regulations. In this article, we explore the key components, design principles, and applications of such systems, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
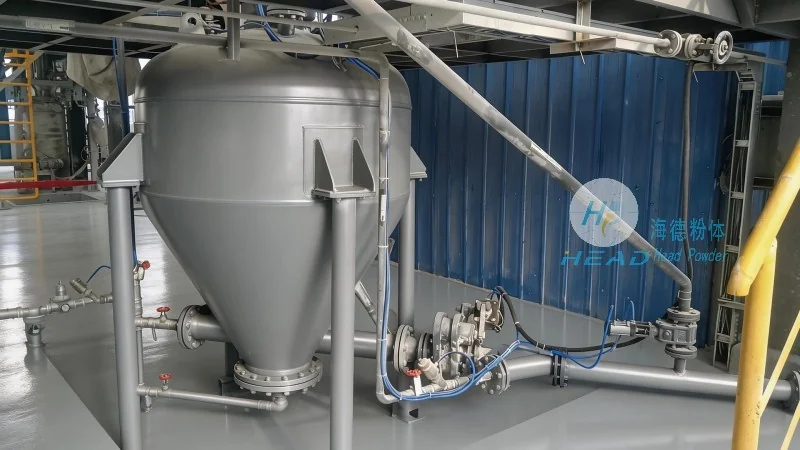
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for the food processing industry. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in designing and manufacturing efficient food powder handling systems. HeadPowder’s headquarters are located in Shandong, China, where the company leverages its local expertise and resources to deliver tailored solutions that meet the unique needs of food manufacturers worldwide.
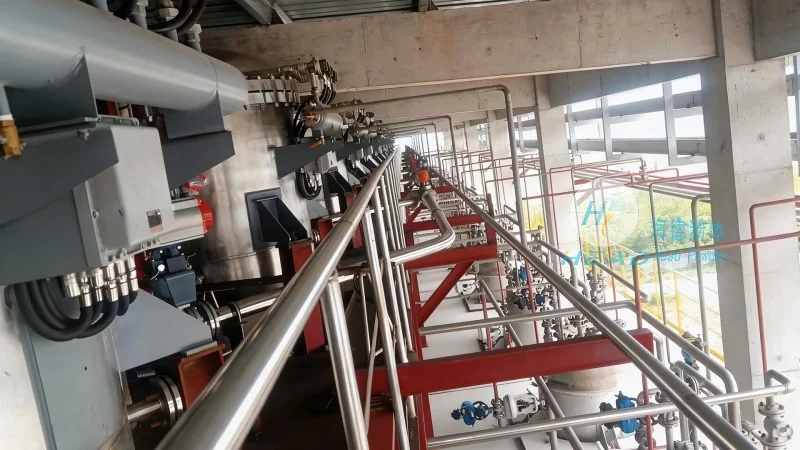
Design Principles of Food Powder Handling Systems
The design of a food powder handling system involves several critical principles aimed at ensuring reliable operation and product integrity. One of the primary considerations is the prevention of product segregation and agglomeration, which can occur due to variations in particle size, density, or moisture content. To address this, systems often incorporate features such as aeration, vibration, or air-assisted conveying to maintain a uniform flow. Additionally, the materials used in the construction of the system components must be food-grade and resistant to corrosion, ensuring that they do not contaminate the product or pose health risks. Another key design principle is the minimization of pressure drops and energy consumption, as this directly impacts operational costs and efficiency. HeadPowder’s engineers employ advanced computational fluid dynamics (CFD) and material science knowledge to optimize system designs, resulting in solutions that are both effective and cost-efficient.
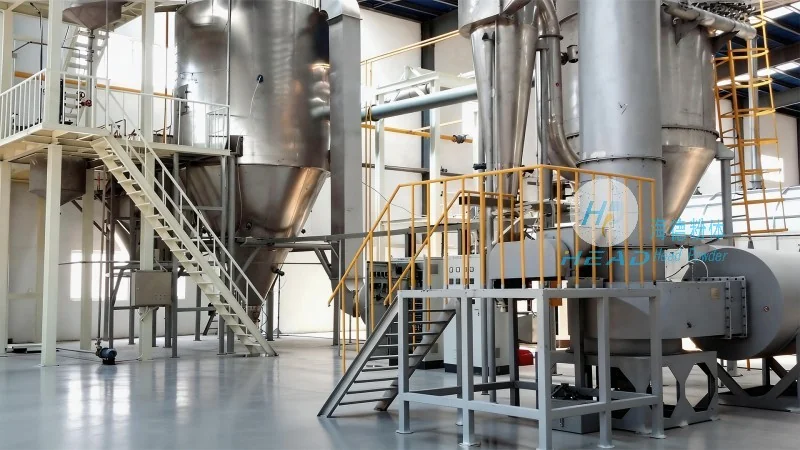
Key Components of Food Powder Handling Systems
Food powder handling systems typically consist of several interconnected components that work together to achieve seamless material transfer. The primary components include a hopper or feeder, which serves as the initial storage and feeding unit, ensuring a consistent supply of powder. The feeder may be equipped with a rotary valve or a vibratory feeder to control the flow rate and prevent blockages. The conveying section, which can be pneumatic or mechanical, transports the powder from the feeder to the discharge point. Pneumatic systems use air pressure to move the powder through a pipeline, while mechanical systems rely on screws, belts, or augers to push the material forward. The discharge unit, such as a rotary valve or a metering device, regulates the outflow of the powder to the next processing stage. HeadPowder’s systems are designed with these components in mind, ensuring that each part is optimized for the specific powder characteristics and operational requirements of the client.
Applications in the Food Industry
Food powder handling systems are widely used across various sectors of the food industry, including dairy, bakery, confectionery, and pharmaceuticals. In dairy processing, these systems are essential for transporting milk powders, whey powders, and other dairy ingredients to production lines. In the bakery industry, they help move flour, sugar, and other dry ingredients to mixing and baking equipment. For confectionery manufacturers, the systems ensure the efficient handling of cocoa, sugar, and flavorings. Even in the pharmaceutical sector, where product purity is paramount, food-grade powder handling systems are employed to maintain quality standards. HeadPowder’s solutions are tailored to meet the specific demands of each industry, ensuring that the systems are not only functional but also compliant with industry regulations and standards.
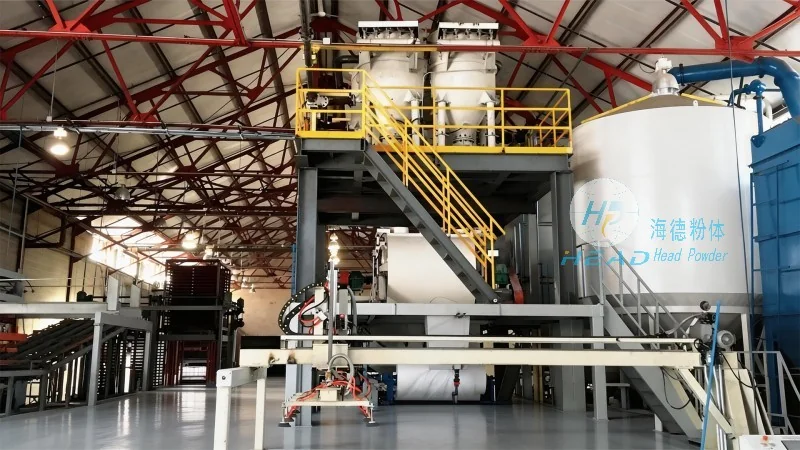
Ensuring System Performance and Reliability
Regular maintenance and proper operation are crucial for maximizing the lifespan and efficiency of food powder handling systems. HeadPowder provides comprehensive support services, including installation, commissioning, and ongoing maintenance, to ensure that the systems operate at peak performance. The company’s technical team conducts regular inspections to identify potential issues, such as blockages, wear and tear, or air leaks, and provides timely solutions to prevent downtime. Additionally, HeadPowder’s systems are designed with easy access points for cleaning and maintenance, reducing the time and effort required for routine upkeep. By prioritizing reliability and performance, HeadPowder helps food manufacturers maintain consistent production schedules and minimize operational costs.