

What is a Dust-Free Metering Pneumatic Conveying System? What are its Design Principles?
Understanding the technology behind dust-free metering pneumatic conveying systems is crucial for industries that require precise material handling while maintaining a clean environment. These systems are engineered to transport powders and bulk materials efficiently, ensuring minimal contamination and accurate dosing. The core of such systems lies in their ability to combine pneumatic conveying with precise metering mechanisms, making them ideal for applications in pharmaceuticals, food processing, and high-purity manufacturing.
Key Components and Design Principles
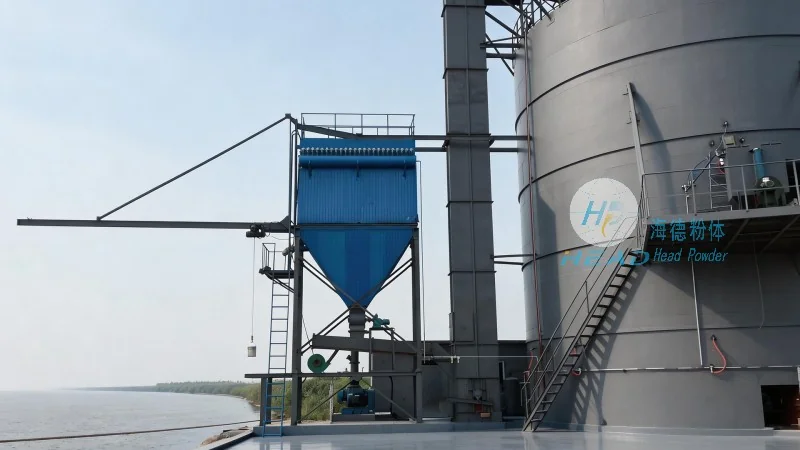
The design of a dust-free metering pneumatic conveying system involves several critical components, each playing a vital role in the overall operation. The system typically includes a hopper for material storage, a metering device to control the flow rate, a pneumatic conveyor to transport the material, and a dust collection system to maintain a clean environment. The metering component, often a rotary valve or a positive displacement pump, ensures that the material is delivered at a consistent rate, preventing over- or under-dosing. The pneumatic conveyor uses compressed air to move the material through a pipeline, with the design of the pipeline and air flow carefully optimized to minimize pressure drop and ensure smooth transport. The dust collection system, such as a cyclone or bag filter, captures any particles that may escape, maintaining a dust-free operation and protecting the environment.
How the System Works: A Step-by-Step Explanation
When the system is activated, material is drawn from the hopper into the metering device. The metering device regulates the flow rate, ensuring a precise amount of material is released into the pneumatic conveyor. Compressed air is then introduced into the conveyor, creating a flow that propels the material through the pipeline. The material travels through the pipeline, which is designed with smooth transitions and minimal bends to reduce friction and maintain consistent air flow. At the destination, the material is discharged into a receiving container. The dust collection system continuously operates, capturing any particles that may be generated during the process, ensuring that the entire system remains clean and free from contamination. This integrated approach ensures that the system operates efficiently while maintaining the highest standards of cleanliness and precision.
Benefits of Using a Dust-Free Metering Pneumatic Conveying System
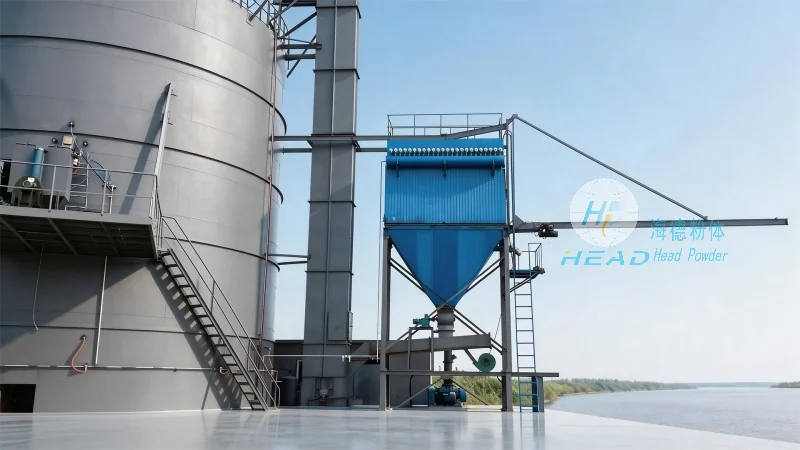
Implementing a dust-free metering pneumatic conveying system offers numerous advantages for industries that handle sensitive materials. One of the primary benefits is the ability to maintain a clean environment, which is essential for applications in pharmaceuticals and food processing where contamination can have severe consequences. The precise metering capabilities of these systems ensure accurate dosing, reducing waste and improving product consistency. Additionally, the pneumatic conveying method is more hygienic than traditional mechanical conveyors, as it eliminates the need for moving parts that can accumulate dust and debris. The system also offers flexibility in material handling, allowing for the transport of a wide range of materials, from fine powders to bulk solids. Furthermore, the dust collection system helps to comply with environmental regulations, reducing the risk of fines and improving the overall safety of the operation.
Applications and Industries
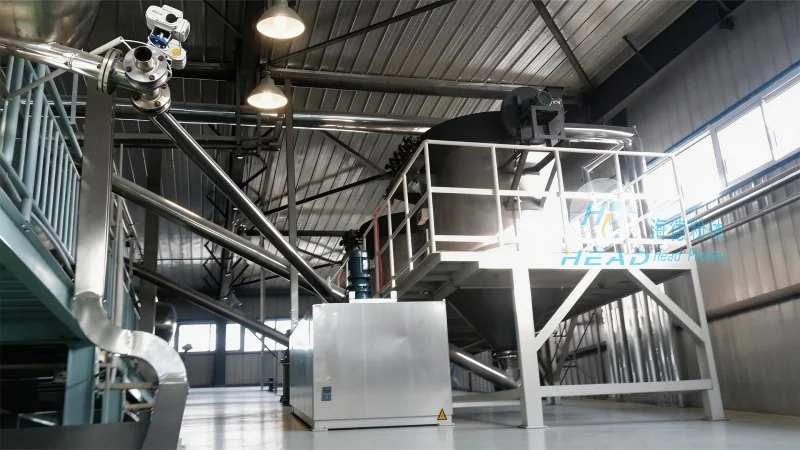
Dust-free metering pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are handled with the utmost care to prevent contamination. In the food processing industry, they are used to convey ingredients such as flour, sugar, and spices, maintaining the purity and quality of the products. The chemical industry also benefits from these systems, as they can handle a variety of chemicals, including those that are hazardous or require a controlled environment. Additionally, the systems are used in the cosmetics industry to transport powders and pigments, ensuring that the final products are free from impurities. The consistent performance of these systems makes them suitable for any application where precision and cleanliness are paramount.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of dust-free metering pneumatic conveying systems, providing industries with reliable and efficient solutions for material handling. By combining advanced technology with a focus on precision and cleanliness, these systems offer a superior alternative to traditional conveying methods. The design principles and components of these systems are carefully engineered to meet the highest standards of performance and safety, ensuring that they are suitable for a wide range of applications. With their ability to maintain a clean environment and deliver precise dosing, dust-free metering pneumatic conveying systems are an essential component of modern industrial operations.