

Design of a Negative Pressure Pneumatic Conveying System for Dust Removal Ash
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and implementation of advanced industrial systems, including negative pressure pneumatic conveying solutions for handling dust removal ash. Our company, commonly known as HeadPowder, is headquartered in Shandong, China, and has built a reputation for delivering efficient and reliable equipment tailored to the needs of various industrial sectors.
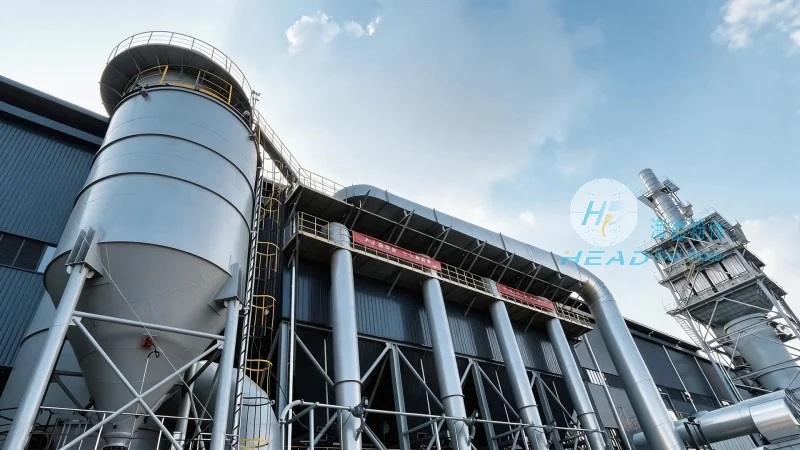
Overview of the Negative Pressure Pneumatic Conveying System
The negative pressure pneumatic conveying system is engineered to transport dust removal ash from collection points to storage or processing facilities with minimal environmental impact and operational efficiency. This technology utilizes a vacuum environment to draw material through a network of pipes, ensuring a clean and controlled transfer process. The system is designed to handle fine particulate materials, making it ideal for applications in power plants, cement factories, and other industries where ash management is critical.
Key Design Principles and Technical Specifications
At the core of our system design is the integration of robust vacuum pumps and high-efficiency filtration components. The vacuum pump generates a consistent negative pressure that pulls ash particles through the conveying line, while the filtration system ensures that air is cleaned before being released back into the environment. Our systems typically feature adjustable flow rates, allowing for precise control over the material transfer process. The pipe network is constructed from corrosion-resistant materials, such as stainless steel, to withstand the abrasive nature of ash and extend the service life of the equipment.
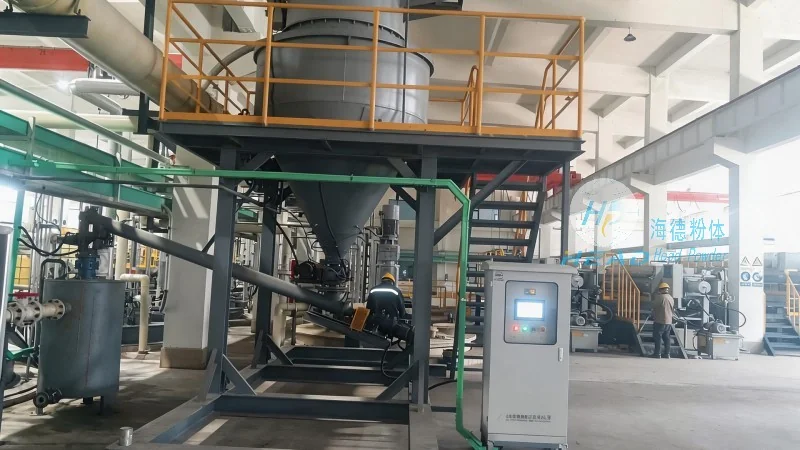
System Components and Operational Workflow
The negative pressure pneumatic conveying system consists of several key components, each playing a crucial role in the overall operation. The primary components include a vacuum pump, dust collection hoppers, conveying pipes, and a filtration unit. The process begins with ash accumulating in the collection hopper, where it is drawn into the system by the vacuum pump. The material travels through the pipes, which may include bends and elbows, to the destination storage or processing unit. The filtration system captures any fine particles, ensuring that the exhaust air meets environmental standards before being discharged.
Advantages of the Negative Pressure Pneumatic Conveying System
Compared to traditional positive pressure systems, the negative pressure approach offers several advantages. It minimizes dust emissions during the transfer process, reducing the risk of environmental contamination and improving workplace safety. The system also requires less energy to operate, as the vacuum pump draws material rather than forcing it through the pipes. Additionally, the design allows for longer conveying distances and can handle multiple collection points, making it a versatile solution for large-scale ash management. The low maintenance requirements and long service life of the equipment further enhance its economic viability for industrial applications.
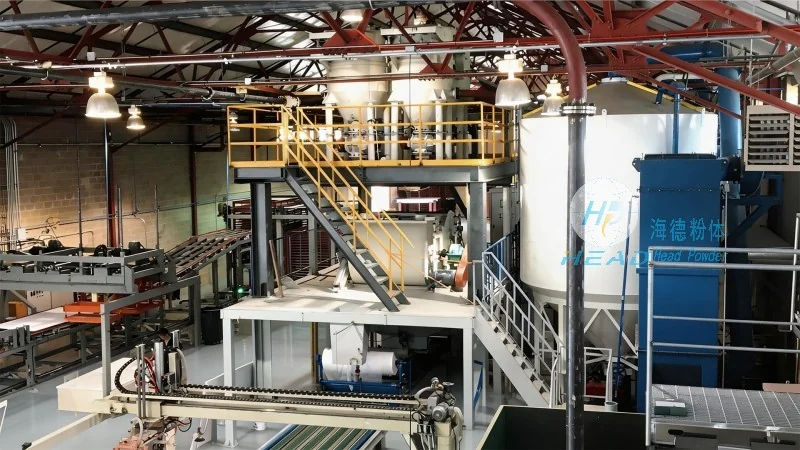
Application Scenarios and Customization Options
Our negative pressure pneumatic conveying systems are adaptable to a wide range of industrial applications. In power plants, the system can efficiently transport fly ash from electrostatic precipitators to storage silos. In cement factories, it helps manage raw material ash and byproducts. The system can also be customized to handle different ash types, including coal ash, slag, and other industrial residues. Clients can choose from various pipe diameters, pump capacities, and filtration configurations to meet their specific operational requirements. HeadPowder provides comprehensive engineering support, including site assessments and system integration, to ensure that the solution is tailored to the client's unique needs.
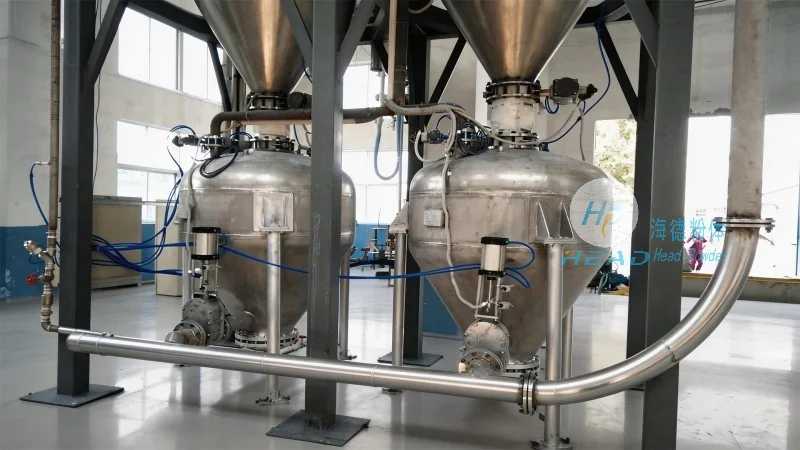
Environmental and Safety Considerations
Environmental compliance is a top priority in the design of our negative pressure pneumatic conveying systems. The filtration units are designed to capture over 99% of particulate matter, ensuring that emissions are well within regulatory limits. The system's enclosed design prevents dust from escaping into the environment, reducing the risk of air pollution and health hazards for workers. Safety features, such as pressure relief valves and emergency shut-off mechanisms, are integrated into the design to protect personnel and equipment during operation. Regular maintenance and monitoring are recommended to maintain optimal performance and ensure long-term environmental and safety compliance.
Conclusion and Service Commitment
Shandong HeadPowder Engineering Co., Ltd. is committed to providing innovative and reliable negative pressure pneumatic conveying solutions for dust removal ash. Our team of experienced engineers and technicians ensures that each system is designed and manufactured to meet the highest standards of quality and efficiency. By leveraging advanced technology and a customer-centric approach, we help industrial clients achieve effective ash management while minimizing environmental impact and operational costs. HeadPowder remains dedicated to advancing the field of industrial material handling, delivering solutions that meet the evolving needs of the industry.