

Design of a Negative Pressure Pneumatic Conveying System for Dust Collection Ash
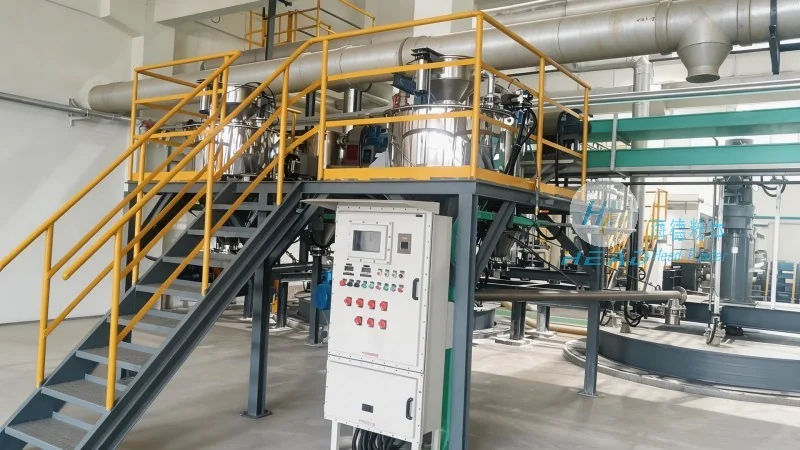
Shandong HeadPowder Engineering Co., Ltd. introduces a cutting-edge negative pressure pneumatic conveying system specifically designed for the efficient and safe transportation of dust collection ash. This advanced equipment represents a significant advancement in material handling technology, addressing the challenges faced by industries that rely on dust and ash management for their operations. The system is engineered to deliver high performance, reliability, and environmental compliance, making it an ideal solution for power plants, cement factories, and other industrial facilities where large volumes of fine particulate matter need to be moved from collection points to storage or disposal sites.
Core Design Features and Technical Advantages
The negative pressure pneumatic conveying system utilizes a sophisticated vacuum-based conveying mechanism that ensures consistent and controlled material flow. Key components include high-capacity suction units, flexible hoses or pipelines, and efficient dust filtration systems. The design incorporates advanced air purification technology, which captures and filters out fine particles, preventing dust emissions and maintaining air quality in the operational environment. The system’s modular construction allows for easy installation and integration with existing infrastructure, while its robust materials and components are selected to withstand the abrasive and corrosive nature of dust collection ash, ensuring long-term durability and minimal maintenance requirements.

Company Background and Expertise
HeadPowder, the manufacturer behind this innovative system, has built a strong reputation in the engineering and manufacturing sector over the years. With a focus on research and development, the company specializes in creating customized solutions for material handling and environmental control. The team at HeadPowder comprises experienced engineers, technicians, and project managers who bring a wealth of knowledge and expertise to each project. Their commitment to quality and customer satisfaction has enabled them to serve a diverse range of industries, including power generation, cement production, and chemical processing, providing tailored equipment that meets specific operational needs and regulatory standards.

Application Scenarios and Operational Benefits
The negative pressure pneumatic conveying system is particularly suitable for applications in power plants where fly ash is collected from boilers and needs to be transported to storage silos or disposal sites. In cement factories, it efficiently handles raw material dust and finished product ash, streamlining the production process. Additionally, in chemical and industrial facilities, the system aids in the transportation of various fine powders and dust, enhancing overall operational efficiency. The operational benefits of this system are substantial: it reduces labor costs by automating the material handling process, minimizes material loss during transport, and enhances workplace safety by eliminating manual handling of dust-laden materials. Furthermore, the negative pressure design effectively controls dust emissions, contributing to a cleaner and healthier working environment and helping facilities comply with environmental regulations.
Customization and Integration Capabilities
HeadPowder understands that each industrial facility has unique requirements, and thus offers comprehensive customization options for the negative pressure pneumatic conveying system. Clients can specify parameters such as conveying distance, material flow rate, and system capacity to match their operational needs. The company’s engineering team works closely with clients to assess their specific challenges and design a system that optimizes performance and efficiency. Integration with existing control systems and automation is also possible, ensuring seamless operation with the facility’s overall workflow. Whether for new installations or retrofitting existing systems, HeadPowder provides tailored solutions that enhance productivity and reduce operational costs.
Quality Assurance and After-Sales Support
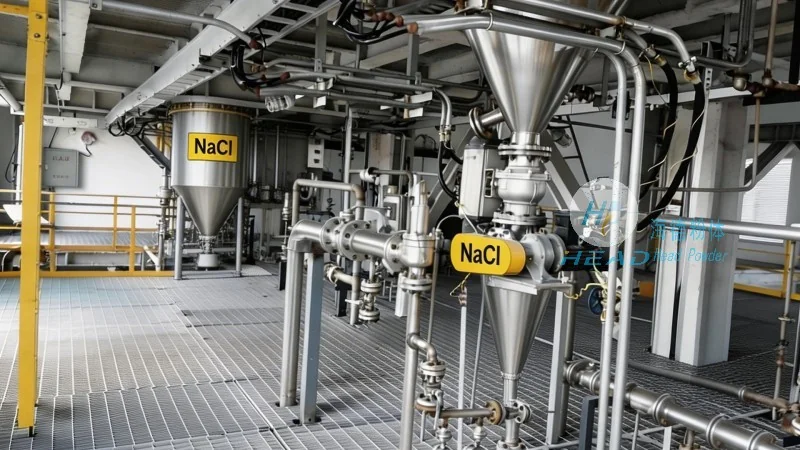
Shandong HeadPowder Engineering Co., Ltd. places a high priority on quality assurance throughout the product lifecycle. From design and manufacturing to testing and delivery, each stage is meticulously monitored to ensure compliance with industry standards and client specifications. The negative pressure pneumatic conveying system undergoes rigorous testing to validate its performance, durability, and safety features. Post-installation, the company offers comprehensive after-sales support, including regular maintenance services, availability of spare parts, and technical assistance. This commitment to customer support ensures that clients receive reliable and long-lasting equipment, with minimal downtime and maximum operational efficiency. The company’s dedication to quality and service has earned it a reputation as a trusted partner in providing effective dust and ash handling solutions.