

Introduction to Equipment and Structural Principles of Mineral Particle Pneumatic Conveying Systems
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier specializing in pneumatic conveying equipment for mineral particles. The company is headquartered in Shandong, China, and has established itself as a key player in the field of bulk material handling solutions. With a focus on innovation and precision engineering, HeadPowder provides comprehensive systems tailored to the unique demands of mineral processing industries.
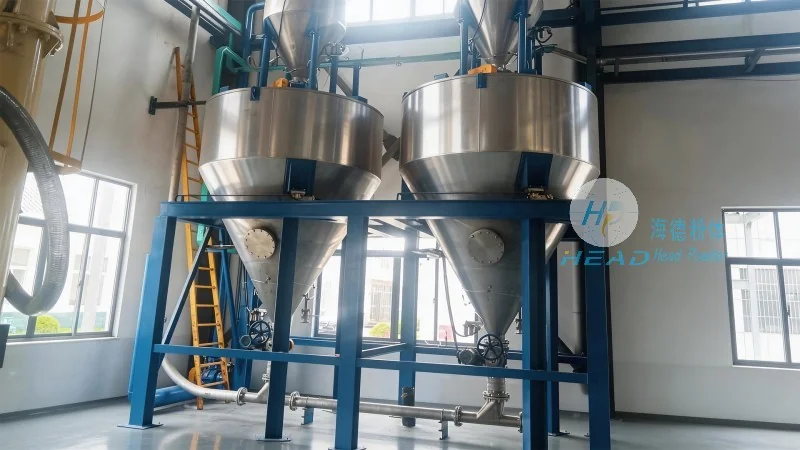
Overview of Pneumatic Conveying Equipment for Mineral Particles
Pneumatic conveying systems are essential for the efficient transport of dry mineral particles over short to medium distances. These systems utilize air or gas as the conveying medium to move materials from one location to another, eliminating the need for mechanical components like belts or buckets. The equipment typically includes a hopper for material storage, a blower or compressor to generate the air flow, and a pipeline network that directs the material through the system. HeadPowder’s equipment is designed to handle a wide range of mineral types, including powders, granules, and fine particles, ensuring reliable and consistent performance in various industrial applications.
Structural Principles and Working Mechanism
The core of a pneumatic conveying system lies in its structural design, which is optimized for both efficiency and durability. The system consists of several key components, each playing a critical role in the overall operation. The hopper, often equipped with a feeder or valve, serves as the material source, ensuring a steady supply of particles. The blower or compressor generates the necessary air pressure to create a flow that propels the material through the pipeline. The pipeline network, made from materials resistant to corrosion and wear, is designed to minimize pressure loss and maintain material integrity. Additionally, the system may include features such as cyclone separators or filters to separate the conveyed material from the air, allowing for clean material discharge and air recycling. HeadPowder’s systems are engineered to balance these components, ensuring smooth operation and minimal maintenance.
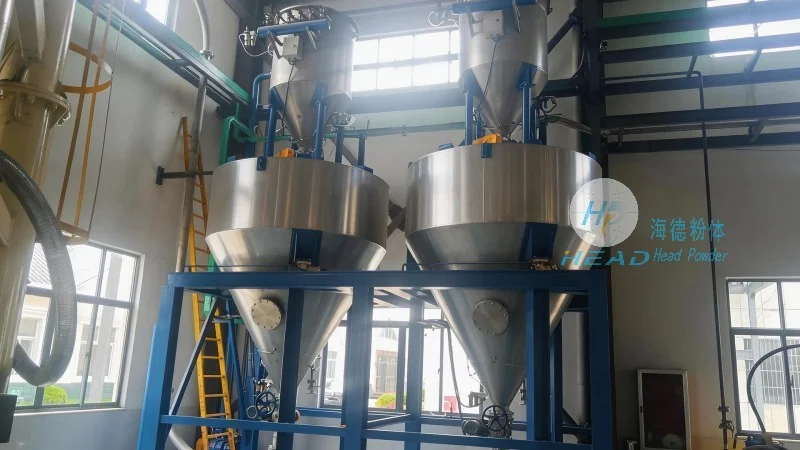
Applications in Mineral Processing Industries
Mineral particle pneumatic conveying systems are widely used in various industries, including mining, cement, chemical, and food processing. In mining operations, these systems are crucial for transporting ore from crushers to storage silos or processing plants. In the cement industry, they facilitate the movement of raw materials like limestone and clinker. The chemical industry utilizes them for transporting powders such as pigments and additives, while food processing applications involve the handling of dry ingredients like flour and sugar. HeadPowder’s equipment is adaptable to these diverse applications, providing customized solutions that meet specific operational requirements and material characteristics.
Technical Advantages and Innovation
HeadPowder’s pneumatic conveying systems offer several technical advantages that set them apart in the market. The company employs advanced materials and manufacturing techniques to ensure high durability and resistance to wear and corrosion. The design incorporates features such as adjustable air flow control, which allows for precise regulation of material transport speed and pressure. This flexibility enables operators to optimize the system for different material types and processing conditions. Additionally, the systems are equipped with monitoring and control systems that provide real-time data on performance, enabling proactive maintenance and reducing downtime. HeadPowder’s commitment to research and development ensures that their products remain at the forefront of industry standards, delivering reliable and efficient solutions for mineral particle handling.
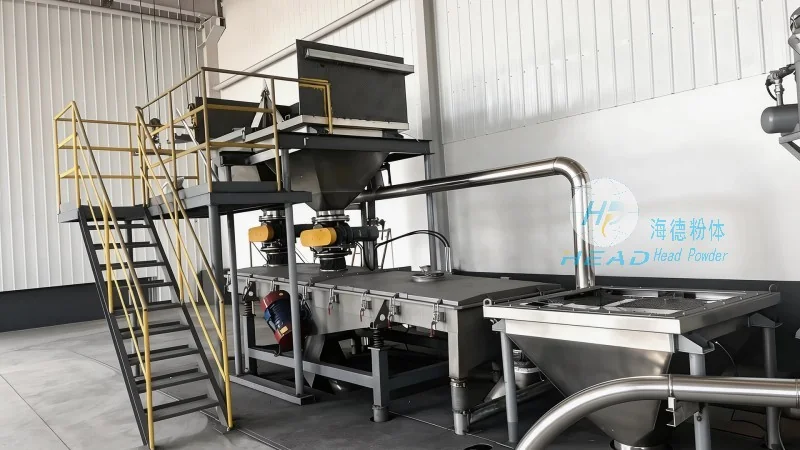
Maintenance and Reliability
Reliability is a key consideration in industrial operations, and HeadPowder’s pneumatic conveying systems are built to deliver consistent performance over extended periods. The company emphasizes the use of high-quality components and rigorous quality control processes to minimize the risk of failures. Regular maintenance, including inspections of the hopper, blower, and pipeline, is recommended to ensure optimal operation. HeadPowder provides comprehensive support, including technical guidance and spare parts availability, to assist customers in maintaining their equipment. The robust design of the systems, combined with proper maintenance, ensures long service life and low operational costs, making them a cost-effective solution for mineral particle transport.
Conclusion
HeadPowder Engineering Co., Ltd. from Shandong, China, specializes in the design and manufacturing of pneumatic conveying systems for mineral particles. Their equipment is engineered to provide efficient, reliable, and durable solutions for various industrial applications. By combining advanced structural principles with innovative technology, HeadPowder meets the diverse needs of the mineral processing industry, ensuring smooth and consistent material transport. With a focus on quality and customer satisfaction, the company continues to be a trusted partner in bulk material handling solutions.