

Operation Process and Working Principle of Small Stone Powder Pneumatic Conveying System
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in the design, production, and installation of advanced pneumatic conveying systems. The small stone powder pneumatic conveying system is a critical solution for efficiently transporting fine powders and granular materials over short to medium distances. This system is particularly suitable for applications involving small stone powders, such as in construction, mining, and chemical industries, where reliable and low-cost material transport is essential.
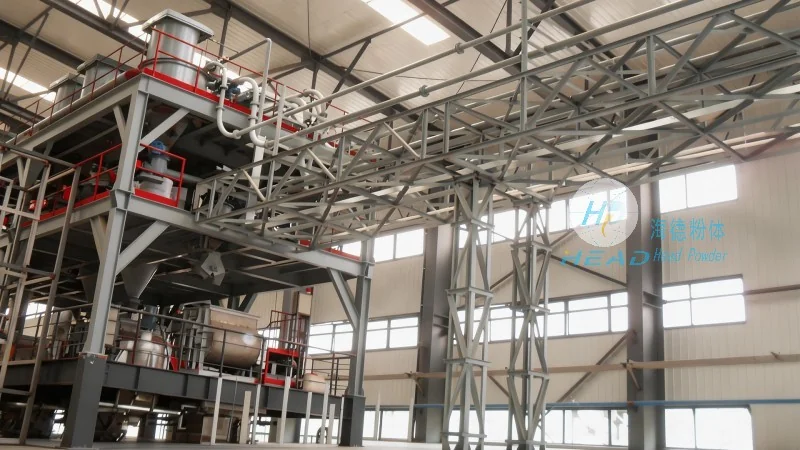
Key Components of the Pneumatic Conveying System
The small stone powder pneumatic conveying system consists of several key components that work in tandem to ensure efficient material transport. These components include the material hopper, which serves as the storage and feeding unit; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying line, typically made of stainless steel or plastic, which carries the material and air mixture; the control valve, which regulates the flow of material and air; and the receiving hopper or discharge point, where the material is deposited. Each component plays a vital role in maintaining the system's performance and ensuring the safe and efficient transport of small stone powders.
Operation Process of the Pneumatic Conveying System
The operation of the small stone powder pneumatic conveying system involves a series of steps that ensure the smooth and continuous transport of material. The process begins with the material being fed from the hopper into the conveying line. The air compressor then generates a high-pressure air stream, which is introduced into the conveying line. As the air flows through the line, it creates a negative pressure or positive pressure environment, depending on the system design, to draw the small stone powder particles into the air stream. The mixture of air and material then travels through the conveying line to the receiving hopper. The control valve may be used to adjust the flow rate or pressure, ensuring optimal transport conditions. The system is designed to handle various particle sizes and moisture contents of small stone powders, making it versatile for different industrial applications.
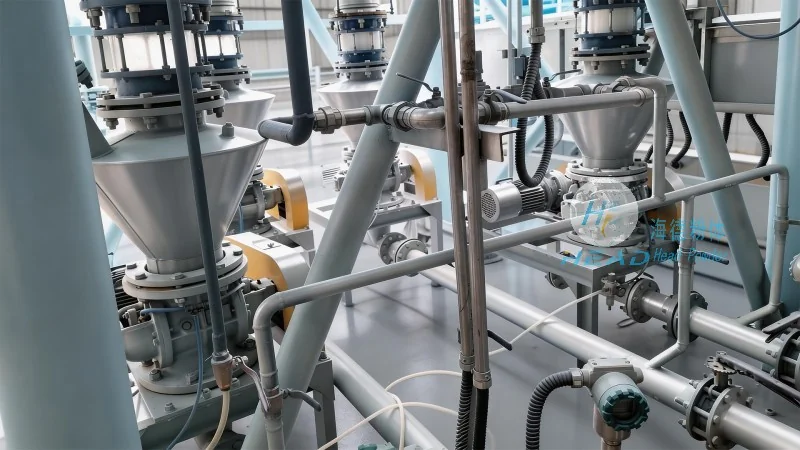
Working Principle of the Pneumatic Conveying System
The working principle of the small stone powder pneumatic conveying system is based on the principles of fluid dynamics and particle transport. The system utilizes compressed air to create a flow that carries the small stone powder particles through the conveying line. In a positive pressure system, the air compressor supplies high-pressure air that pushes the material through the line, while the receiving hopper is under a slightly lower pressure to create a pressure differential. In a negative pressure (or suction) system, the air is drawn from the conveying line by a vacuum pump, creating a negative pressure that pulls the material into the line. The small stone powder particles are suspended in the air stream due to the drag force exerted by the air, allowing them to be transported efficiently. The system's design ensures that the material is not damaged during transport, and the air is filtered to prevent dust from escaping into the environment. This working principle makes the small stone powder pneumatic conveying system an effective and reliable solution for material handling in various industries.
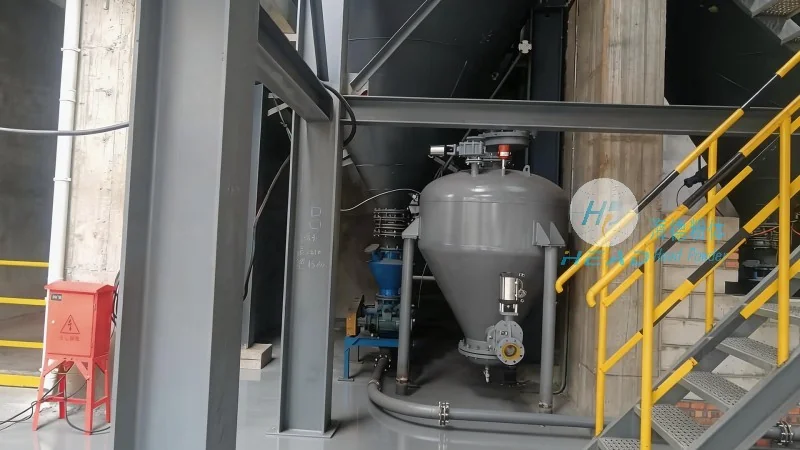
Advantages of the Small Stone Powder Pneumatic Conveying System
Compared to traditional mechanical conveying methods, the small stone powder pneumatic conveying system offers several advantages that make it a preferred choice for many industries. One of the key advantages is its ability to transport materials over long distances with minimal maintenance. The system is also suitable for transporting materials that are difficult to handle with mechanical systems, such as those with high moisture content or abrasive properties. Additionally, the system is compact and can be installed in confined spaces, making it ideal for applications where space is limited. The small stone powder pneumatic conveying system also provides a hygienic and dust-free environment, which is crucial for industries that require clean handling of materials. Furthermore, the system is energy-efficient, as it uses compressed air, which can be sourced from existing air systems in many facilities. These advantages make the small stone powder pneumatic conveying system a cost-effective and efficient solution for material transport in various applications.
Applications of the Small Stone Powder Pneumatic Conveying System
The small stone powder pneumatic conveying system is widely used in various industries due to its versatility and efficiency. In the construction industry, it is used to transport small stone powders such as cement, sand, and gravel from storage to mixing plants or construction sites. In the mining industry, it is used to transport ore powders from processing plants to storage facilities or for further processing. In the chemical industry, it is used to transport various chemical powders, including those with high moisture content or abrasive properties. The system is also used in the food and pharmaceutical industries for transporting powders that require a hygienic and dust-free environment. The small stone powder pneumatic conveying system is suitable for both batch and continuous material transport, making it adaptable to different production requirements. Its ability to handle various particle sizes and moisture contents makes it a reliable solution for a wide range of applications.