

Operation Process and Working Principle of Metering Bin Pump Powder Pneumatic Conveying
HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and application of metering bin pumps for pneumatic conveying systems. This article provides a detailed overview of the operation process and working principle of these critical equipment, highlighting their efficiency, reliability, and versatility in handling various types of powders.
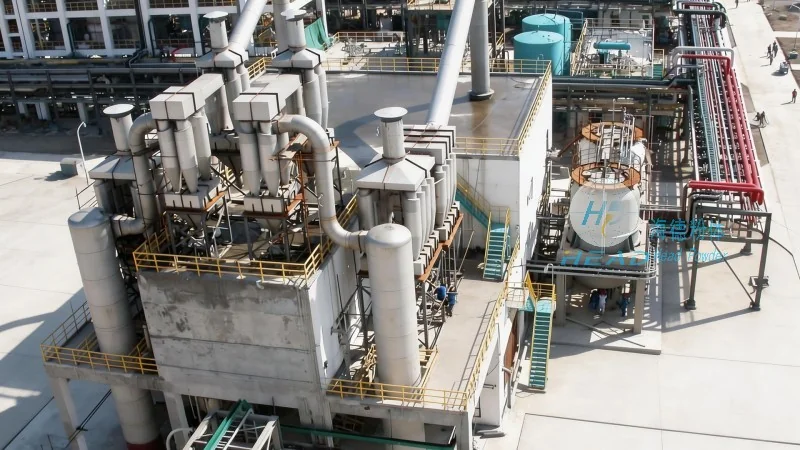
Company Profile
HeadPowder, officially known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted name in the industry, delivering high-quality solutions tailored to the specific needs of clients in diverse sectors such as chemical, pharmaceutical, food, and industrial manufacturing.
Introduction to Metering Bin Pumps
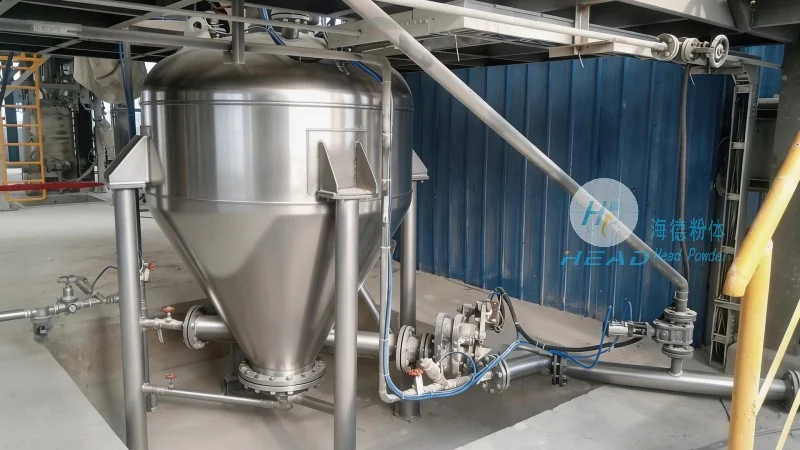
Metering bin pumps are essential components in pneumatic conveying systems, designed to accurately measure and transport bulk powders through a pressurized air stream. These pumps combine the functions of a hopper, a metering device, and a pneumatic conveyor, making them ideal for applications requiring precise control over powder flow rates and consistent material handling.
Working Principle of Metering Bin Pumps
The operation of a metering bin pump is based on the principle of creating a pressure differential between the hopper and the discharge line. The pump operates by drawing air into the hopper through an inlet valve, while simultaneously maintaining a positive pressure within the system. As the air flows into the hopper, it lifts the powder from the bottom of the hopper and transports it through the discharge line to the destination point. The metering mechanism ensures that the powder is discharged at a controlled rate, preventing overloading or underloading of the system.
Key Components and Their Functions
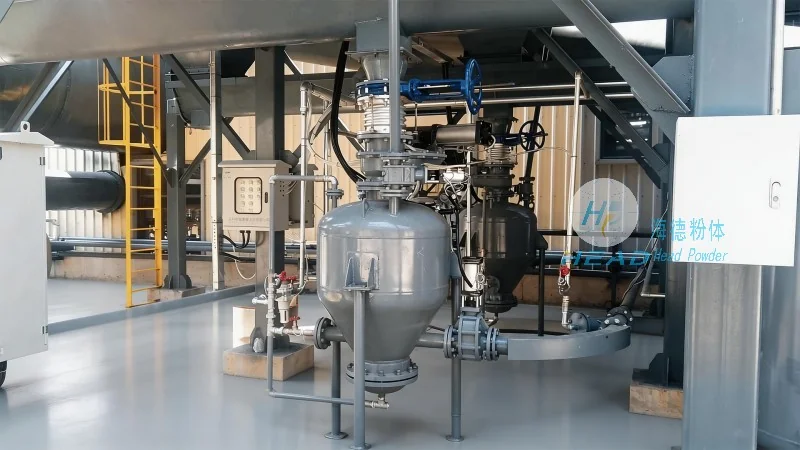
Several key components work in tandem to ensure the smooth operation of a metering bin pump. These include the hopper, which stores the powder; the air inlet valve, which controls the air flow into the hopper; the discharge valve, which regulates the powder discharge; and the pressure regulator, which maintains the system pressure at a consistent level. Additionally, the pump may incorporate a filter system to prevent dust and particles from entering the air stream, ensuring clean and efficient operation.
Operation Process of Metering Bin Pumps
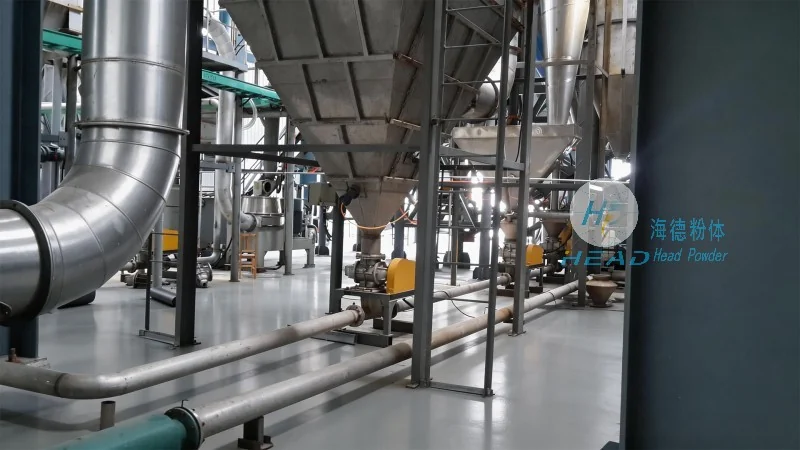
The operation process of a metering bin pump typically involves several steps. First, the hopper is filled with the powder to be conveyed. Next, the air inlet valve is opened, allowing air to enter the hopper and create a pressure differential. The powder is then lifted and transported through the discharge line as the air continues to flow. The metering mechanism adjusts the flow rate based on the system requirements, ensuring that the powder is delivered at the desired rate. Finally, the system is monitored to ensure that the pressure and flow rates are within the optimal range, and adjustments are made as needed to maintain efficiency.
Advantages of Metering Bin Pumps
Metering bin pumps offer several advantages over traditional conveying methods. They provide precise control over powder flow rates, reducing waste and improving product quality. The pressurized air system ensures that the powder is conveyed in a clean and hygienic manner, making them suitable for applications in the food and pharmaceutical industries. Additionally, these pumps are compact and easy to install, requiring minimal space and maintenance. They also offer high efficiency and reliability, with low energy consumption and long service life.
Applications of Metering Bin Pumps
Metering bin pumps are widely used in various industries, including chemical, pharmaceutical, food, and industrial manufacturing. They are particularly suitable for conveying powders that are difficult to handle, such as fine powders, cohesive powders, and powders with high moisture content. The precise control over flow rates makes them ideal for applications that require accurate dosing, such as in the production of powders for pharmaceuticals, food products, and industrial chemicals.
Conclusion
In conclusion, metering bin pumps are a critical component in modern pneumatic conveying systems, offering efficient and reliable solutions for handling bulk powders. With their precise control over flow rates and ability to handle a wide range of materials, these pumps are essential for industries that require high-quality and consistent powder handling. HeadPowder, with its expertise and commitment to quality, continues to provide innovative solutions that meet the evolving needs of its clients.