

Operation Process and Working Principle of Tonne Bag Packing Powder Conveying Machine
For industries dealing with bulk powders, efficient and reliable material handling is crucial. The tonne bag packing powder conveying machine, a specialized equipment designed by Shandong HeadPowder Engineering Co., Ltd. from China, offers a comprehensive solution for transporting and packaging powders in large quantities. This article delves into the operation process and working principle of this machine, highlighting its key features and benefits. Such equipment is essential for businesses that need to manage high volumes of powders, ensuring that the material is handled safely, hygienically, and with minimal loss.
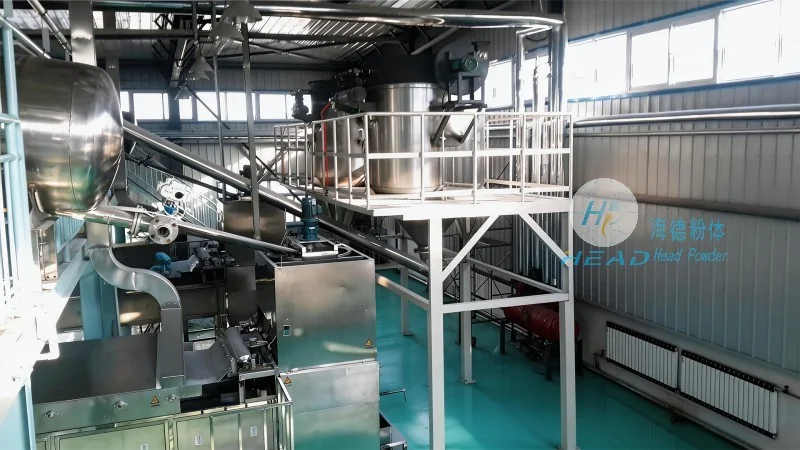
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the company is commonly known, is a leading manufacturer of powder handling equipment based in Shandong, China. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses in various sectors, including food, chemical, and pharmaceutical industries. The company’s headquarters is located in Shandong, China, where its team of experts develops and manufactures advanced powder conveying systems tailored to meet the specific needs of clients worldwide. The company adheres to international standards and continuously invests in research and development to improve the performance and efficiency of its products.
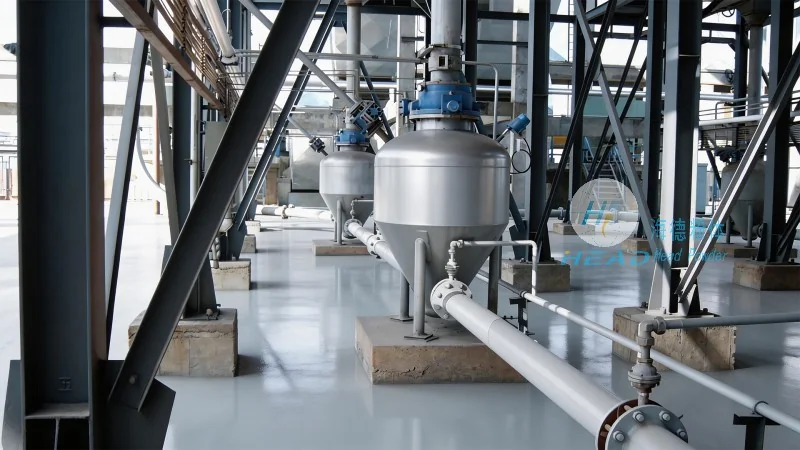
Key Components and Structure of the Tonne Bag Packing Powder Conveying Machine
The tonne bag packing powder conveying machine consists of several key components that work in harmony to ensure smooth operation. The main parts include a hopper for material storage, a conveyor system for transporting powders, a packing unit for filling tonne bags, and a control panel for monitoring and adjusting the process. The machine is typically constructed with durable materials, such as stainless steel, to withstand the demands of high-volume powder handling and ensure long-term reliability. The hopper is designed to hold large quantities of raw powders, often with a sloped bottom to facilitate material flow. The conveyor system, which may include screws, belts, or pneumatic lines, ensures a consistent and controlled movement of the powder from the hopper to the packing unit. The packing unit is equipped with a filling mechanism that precisely measures and dispenses the powder into tonne bags, typically using a weighing or volumetric system. The control panel integrates sensors and actuators to regulate the entire process, providing real-time feedback and adjustments as needed. Additionally, the machine may include features such as bag sealing and strapping systems to secure the filled bags before they are discharged.
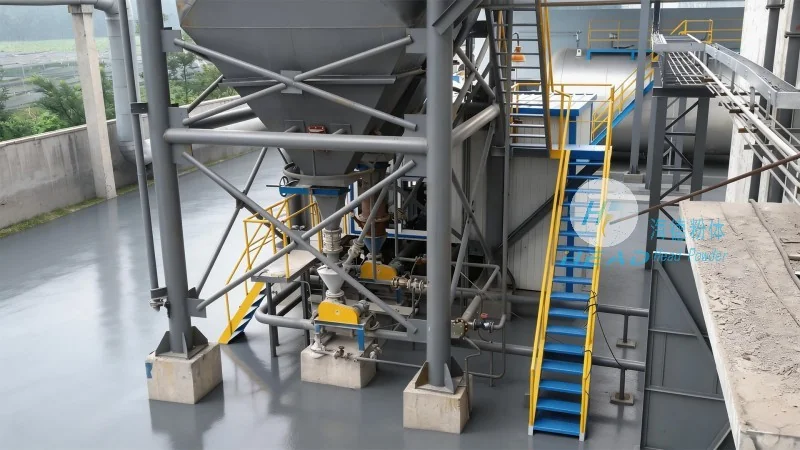
Operation Process of the Tonne Bag Packing Powder Conveying Machine
The operation of the tonne bag packing powder conveying machine involves several sequential steps, each designed to optimize efficiency and accuracy. The process begins with the loading of raw powders into the hopper. The material is then fed into the conveyor system, which transports it to the packing unit. The packing unit is equipped with a filling mechanism that precisely measures and dispenses the powder into tonne bags. The machine may also include a sealing and strapping system to secure the filled bags before they are discharged. Throughout the operation, the control panel allows operators to monitor parameters such as flow rate, filling level, and bag count, ensuring that the process runs smoothly and meets quality standards. The operator can start or stop the machine, adjust the filling speed, and check the status of the system at any time. The machine is designed to handle various types of powders, including fine powders, granules, and bulk materials, with minimal adjustments needed for different products.