

Operation Process and Working Principle of Sodium Phosphate Powder Conveying System
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for the efficient handling and transportation of sodium phosphate powders. The company, known as headpowder, has developed a sophisticated conveying system designed to ensure reliable and safe operation in industrial applications. This system is particularly important for industries that rely on consistent and high-quality powder transport, such as chemical manufacturing, food processing, and pharmaceutical production.
Key Components of the Conveying System
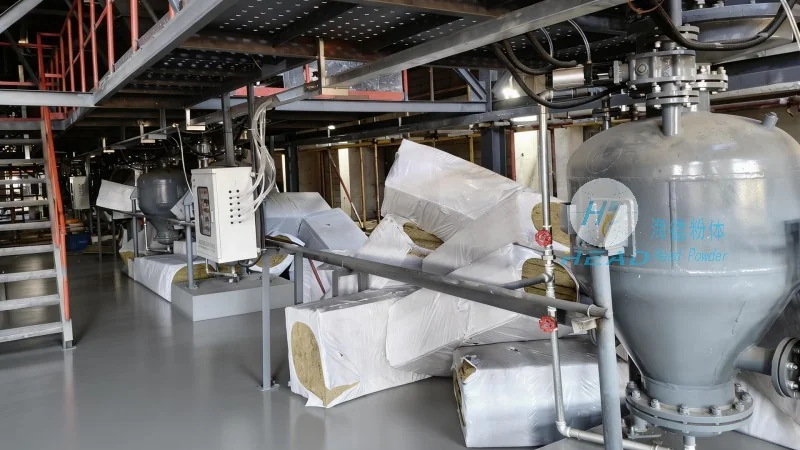
The sodium phosphate powder conveying system consists of several critical components that work in tandem to achieve optimal performance. The main elements include a hopper for material storage, a feeder to control the flow rate, a conveyor (either pneumatic or mechanical) for transporting the powder, and a control system to monitor and adjust operations. Each component is carefully designed to handle the specific characteristics of sodium phosphate, including its density, flowability, and potential for dust generation.
Working Principle of the System
The operation of the sodium phosphate powder conveying system begins with the loading of the powder into the hopper. The feeder then regulates the amount of material released into the conveyor system. In a typical pneumatic conveying setup, compressed air is used to create a flow that moves the powder through the pipeline. The control system continuously monitors parameters like pressure, flow rate, and temperature to ensure the process runs smoothly and safely. This closed-loop system helps maintain consistent material delivery while minimizing the risk of contamination or spillage.
Operation Process Step-by-Step
1. **Material Loading**: The sodium phosphate powder is fed into the hopper from a storage silo or bulk container. The hopper is equipped with a lid and a discharge valve to control the initial flow.
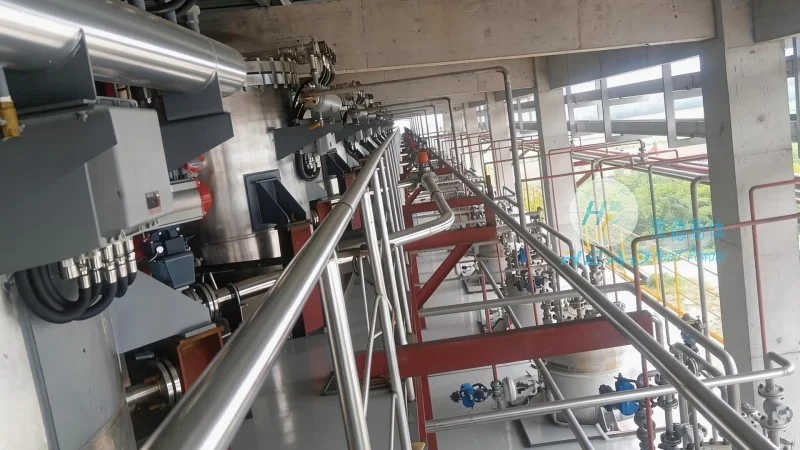
2. **Feeder Activation**: The feeder, often a rotary valve or a screw feeder, starts to rotate, releasing a controlled quantity of powder into the conveyor line. This step ensures a steady and uniform flow, preventing overloading or underflow.
3. **Conveying Phase**: The powder is then transported through the pipeline. In pneumatic systems, the compressed air creates a positive pressure that pushes the powder forward. The pipeline is designed with appropriate bends and fittings to minimize pressure loss and maintain the flow velocity.
4. **Destination Unloading**: At the end of the pipeline, the powder is discharged into a receiving vessel or processing unit. The control system adjusts the air pressure or conveyor speed to ensure accurate and complete unloading.
Advantages of the System
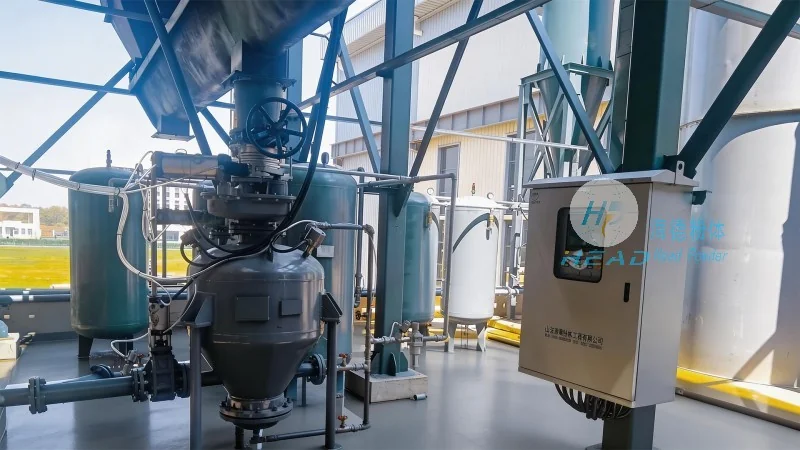
The sodium phosphate powder conveying system offers several advantages that make it a preferred choice for industrial applications. First, it provides a dust-free and enclosed environment, which is crucial for maintaining product quality and safety. Second, the system is highly efficient, with minimal material loss and consistent flow rates. Third, it can handle a wide range of powder characteristics, including varying particle sizes and moisture content. Additionally, the automated control system reduces the need for manual intervention, improving operational safety and reducing labor costs.
Applications and Industries
The sodium phosphate powder conveying system is widely used in various industries that require reliable powder transport. In the chemical industry, it is used for transporting raw materials and finished products. In food processing, it helps in the handling of food-grade sodium phosphate, ensuring compliance with safety and quality standards. The pharmaceutical industry also benefits from this system, as it provides a sterile and controlled environment for transporting active pharmaceutical ingredients (APIs) and excipients.
Contact Information
Shandong HeadPowder Engineering Co., Ltd. is located in Shandong, China, and serves clients globally with its advanced conveying solutions. The company’s expertise in powder handling technology ensures that customers receive tailored systems that meet their specific operational needs.