

The Operation Process and Working Principle of Urea Powder Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and implementation of efficient urea powder conveying systems. With a strong presence in China, the company leverages advanced engineering solutions to address the unique challenges associated with handling urea powder, a critical fertilizer and industrial chemical.
The Core Components of Urea Powder Conveying
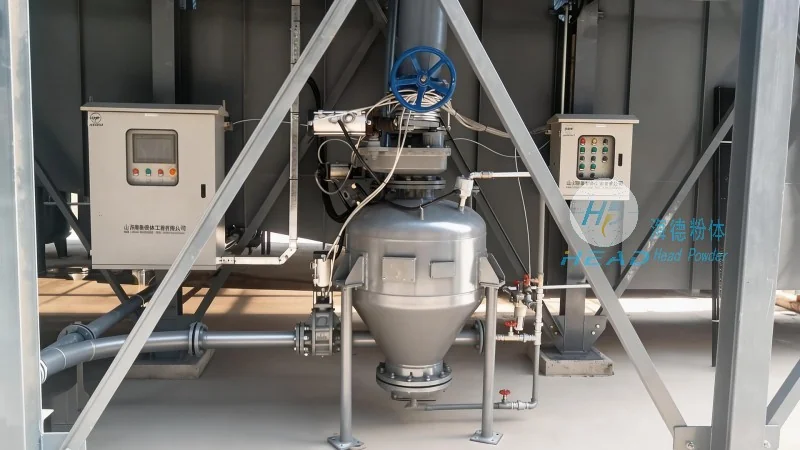
At the heart of any urea powder conveying system are several key components that work in tandem to ensure reliable and efficient material transport. These include feeders, conveying lines, and control systems. The feeders, typically rotary or vibratory types, are designed to handle the bulk urea powder and regulate the flow rate, preventing blockages and ensuring consistent material delivery. The conveying lines, often made of corrosion-resistant materials like stainless steel or special polymers, are engineered to withstand the abrasive nature of urea powder and maintain airtight integrity to prevent dust emissions. Control systems, equipped with sensors and automation technology, monitor the entire process, adjusting parameters in real-time to optimize performance and safety.
The Operation Process of Urea Powder Conveying
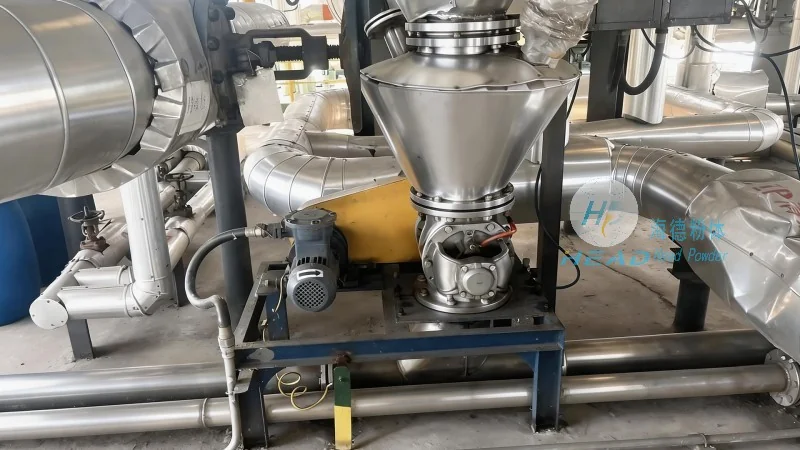
The operation process of a urea powder conveying system begins with the loading of urea powder into the hopper or storage silo. From there, the feeder mechanism activates, drawing the powder into the conveying line. As the powder moves through the line, it is propelled by air or mechanical forces, depending on the system design. The system ensures that the powder is transported smoothly from the source to the destination, such as a storage tank, processing facility, or shipping container. Throughout the process, the control system continuously monitors pressure, flow rate, and temperature to maintain optimal conditions and prevent any operational issues.
Working Principle of Urea Powder Conveying Systems
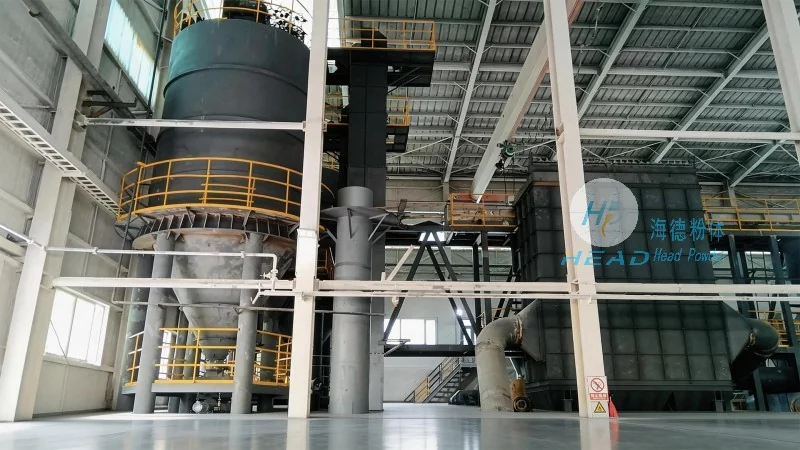
The working principle of urea powder conveying systems revolves around the fundamental concept of material transport through a pressurized or vacuum environment. For pneumatic conveying systems, which are commonly used for urea powder, compressed air is introduced into the conveying line, creating a flow that carries the powder particles. The air velocity is carefully controlled to ensure that the powder is suspended and transported without causing excessive wear on the system components. Mechanical conveying systems, on the other hand, use rotating screws or belts to move the powder, providing a more direct and continuous transport method. Both systems are designed to handle the specific properties of urea powder, including its high moisture content and potential for caking, ensuring reliable operation and minimal downtime.
Advantages of Efficient Urea Powder Conveying
Efficient urea powder conveying systems offer numerous advantages for industrial and agricultural applications. By minimizing material loss and dust emissions, these systems enhance safety and compliance with environmental regulations. The consistent flow rates and reduced downtime improve overall productivity and reduce operational costs. Additionally, the advanced control systems provide real-time monitoring and data analysis, enabling proactive maintenance and optimization of the conveying process. These benefits make urea powder conveying systems a critical component in modern fertilizer and chemical processing operations.
Conclusion and Company Overview
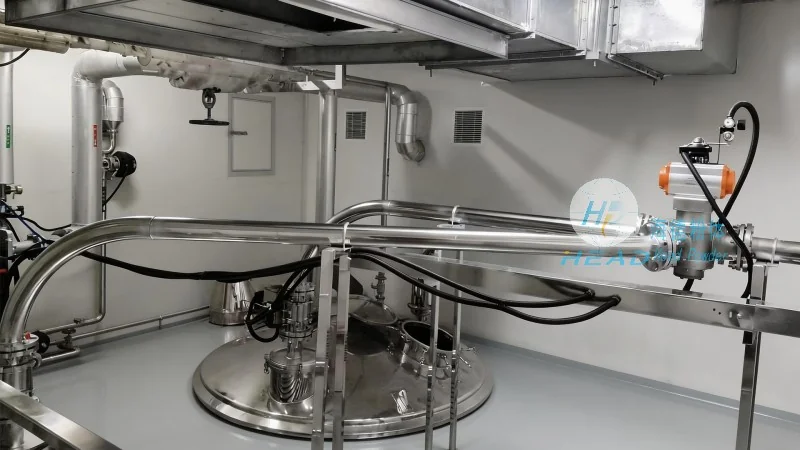
Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of urea powder conveying technology, delivering innovative solutions that meet the evolving needs of the industry. With a commitment to quality, reliability, and customer satisfaction, the company continues to provide cutting-edge systems that enhance operational efficiency and safety. Based in China, the company leverages its local expertise and global standards to serve clients worldwide, ensuring that urea powder is handled with precision and care. As the demand for efficient and sustainable material transport grows, HeadPowder remains dedicated to advancing the technology and providing solutions that drive success in the fertilizer and chemical sectors.