

Principle and Working Scene Characteristics of Micropellet Powder Material Pneumatic Conveying Equip
HeadPowder, a prominent enterprise in the material handling industry, specializes in the design and manufacturing of advanced pneumatic conveying equipment tailored for micropellet powders. This article delves into the fundamental principles of these systems and outlines the key working scene characteristics that define their effectiveness in industrial applications. By understanding the core mechanisms and practical scenarios, readers can appreciate the advantages of adopting such technology for efficient material transport.
The Core Principle of Pneumatic Conveying for Micropellet Powders
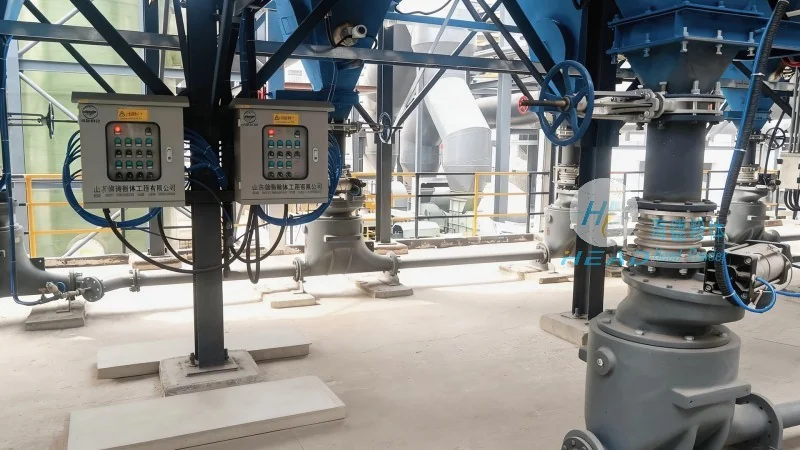
The pneumatic conveying system operates on the principle of using compressed air to transport micropellet powders through a closed pipeline system. Unlike mechanical conveyors that rely on moving parts like belts or screws, pneumatic systems eliminate direct contact between the material and machinery, thereby reducing wear and extending equipment lifespan. The process begins with the micropellet powder being fed into a hopper, where it is then drawn into the conveying line by the air flow generated by a blower or compressor. The air velocity within the pipeline is carefully controlled to ensure that the micropellet particles are suspended and carried to the discharge point without settling or clogging. Key parameters such as air pressure, flow rate, and particle size significantly impact the system's performance. For instance, higher air velocities may be required for finer particles to maintain suspension, while larger particles may need lower velocities to prevent abrasion on the pipeline walls. The system's efficiency is further enhanced by the use of appropriate air filters and moisture control measures, which maintain the quality of the conveyed material.
Key Working Scene Characteristics and Applications
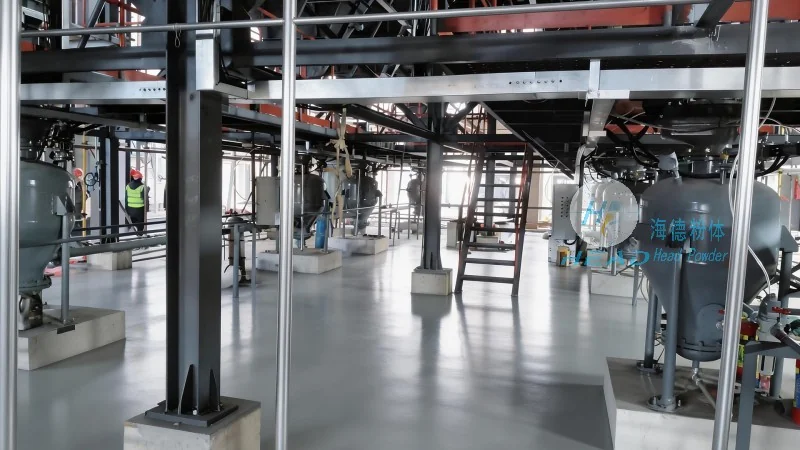
Micropellet powder pneumatic conveying systems are widely utilized across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. The working scene characteristics that make these systems particularly suitable for such applications include: 1. Space Optimization: These systems are ideal for environments with limited horizontal or vertical space, as they can be installed in compact configurations without the need for extensive floor or overhead infrastructure. This makes them suitable for retrofitting into existing facilities or for new installations where space is at a premium. 2. Material Handling Flexibility: The systems can handle a broad spectrum of micropellet powders, ranging from fine powders with particle sizes as small as 10 microns to larger pellets up to several millimeters in diameter. This versatility allows for the transport of diverse materials, including those that are abrasive, corrosive, or sensitive to moisture, without compromising the material's integrity. 3. Process Integration and Automation: Pneumatic conveying systems can be easily integrated with automated production lines, enabling seamless material transfer from storage to processing units. This integration enhances overall operational efficiency by reducing manual handling and minimizing downtime. For example, in pharmaceutical manufacturing, the system can transport active pharmaceutical ingredients (APIs) from bulk storage to filling machines with precision and minimal contamination. 4. Environmental and Safety Advantages: Compared to traditional methods like bucket elevators or belt conveyors, pneumatic systems offer significant environmental benefits. They minimize dust emissions, which is crucial for maintaining a clean and safe working environment, especially in industries where dust is a health hazard. Additionally, the enclosed pipeline design reduces the risk of material spillage and contamination, ensuring compliance with regulatory standards. 5. Customization and Scalability: HeadPowder, as a leading manufacturer, offers customized pneumatic conveying solutions tailored to specific application requirements. Whether it's a small-scale system for laboratory use or a large-scale system for industrial production, the company provides flexible options that can be scaled up or down as needed. This customization ensures that the system meets the exact needs of the client, optimizing performance and cost-effectiveness.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
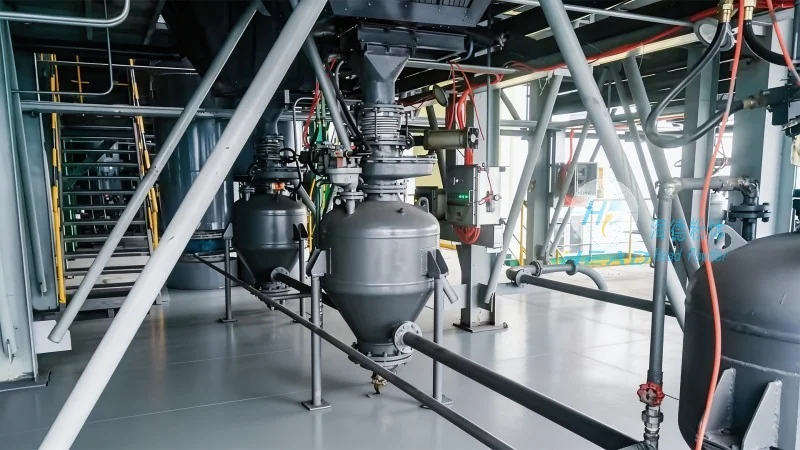
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in Shandong, China. With a strong commitment to innovation and quality, the company has established itself as a trusted provider of pneumatic conveying equipment for micropellet powders. The company's team of experienced engineers and technicians focuses on developing advanced solutions that address the unique challenges of material handling in various industries. By leveraging cutting-edge technology and rigorous quality control processes, HeadPowder ensures that its products meet the highest standards of performance, reliability, and durability. The company's dedication to customer satisfaction and technical support has earned it a strong reputation in the market, making it a preferred choice for businesses seeking efficient and reliable material transport solutions.