

Principle and Working Scene Characteristics of Dust-Free Closed Material Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of dust-free closed pneumatic conveying systems. These systems represent a sophisticated approach to transporting bulk materials while maintaining stringent environmental and operational standards. This article delves into the fundamental principles underlying such systems and highlights the key working scene characteristics that make them indispensable in modern industrial applications.
Core Principle of Dust-Free Closed Pneumatic Conveying Systems
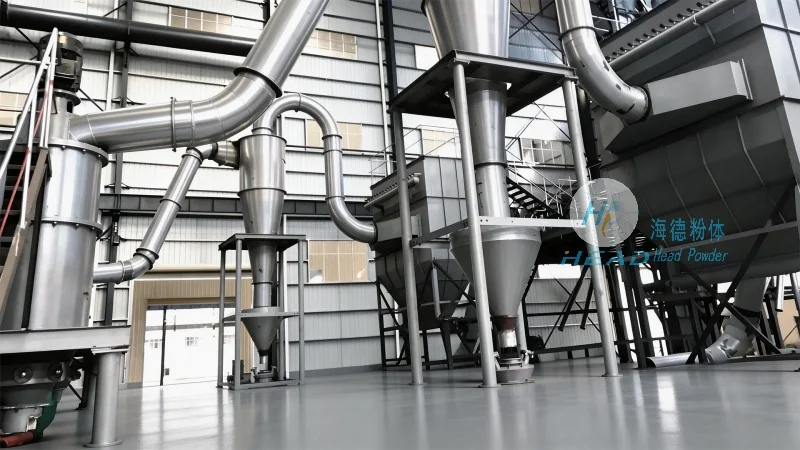
The fundamental principle of dust-free closed pneumatic conveying systems is the use of compressed air or other gases to transport bulk materials through a sealed pipeline network. Unlike traditional open systems that expose materials to the environment, closed systems ensure that all material handling occurs within a contained environment, preventing dust emissions and maintaining material integrity. The system typically consists of a series of components, including a material feeder, a conveying line, a separation unit, and a discharge device. The compressed air acts as the driving force, creating a pressure differential that propels the material through the pipeline. The closed design, often incorporating positive pressure or vacuum, ensures that no dust escapes into the surrounding environment, making it ideal for applications where air quality and material purity are critical.
Working Scene Characteristics and Application Environments
Dust-free closed pneumatic conveying systems are particularly suited for a wide range of industrial working scenes, each demanding specific material handling solutions. The following characteristics define their suitability across different operational contexts:
1. Pharmaceutical and Food Processing Industries
In the pharmaceutical and food processing sectors, maintaining a sterile and dust-free environment is non-negotiable. These industries require systems that prevent cross-contamination and preserve the quality of sensitive materials. HeadPowder's dust-free closed systems are engineered to meet stringent regulatory standards, such as those outlined by the FDA and GMP. The sealed pipelines and air filtration systems ensure that no particulate matter enters the product stream, while the gentle handling of materials minimizes product degradation. For example, in pharmaceutical manufacturing, these systems are used to transport active pharmaceutical ingredients (APIs), excipients, and finished dosage forms without compromising their purity or efficacy.
2. Chemical and Petrochemical Plants
Chemical and petrochemical plants often handle hazardous or reactive materials that require secure and enclosed transportation. The dust-free closed pneumatic conveying systems from HeadPowder are designed to handle corrosive, abrasive, or toxic powders, ensuring worker safety and environmental compliance. The system's ability to maintain positive pressure prevents the release of harmful substances into the workplace, while the robust construction withstands the harsh conditions typical of chemical processing environments. Applications include the transport of catalysts, pigments, and other chemical intermediates, where containment is paramount.
3. Mining and Mineral Processing
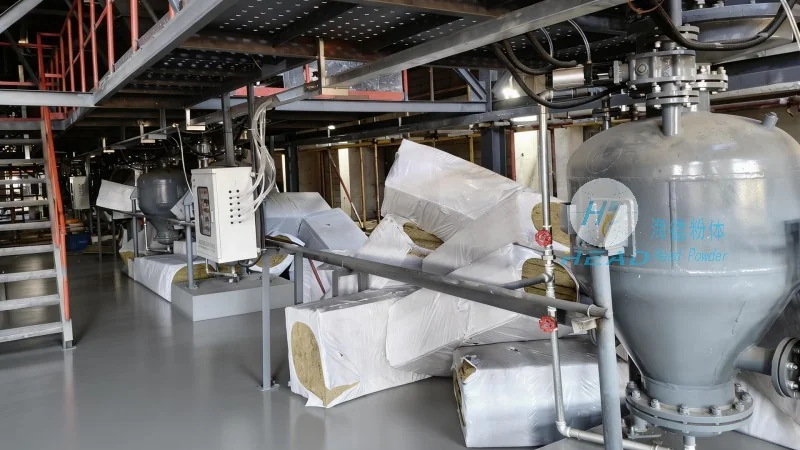
In the mining and mineral processing industry, large volumes of bulk materials, such as ores and minerals, need to be moved efficiently from extraction sites to processing facilities. HeadPowder's systems are adapted to handle the high throughput and abrasive nature of these materials. The closed design minimizes dust generation during transport, reducing the risk of respiratory hazards for workers and preventing material loss. The systems are often integrated with dust collection and filtration units to comply with environmental regulations. For instance, in coal mining operations, these systems are used to convey coal from mines to power plants, ensuring a continuous and clean supply chain.
4. Cement and Construction Materials
The cement and construction materials industry relies on the efficient transport of raw materials like limestone, clinker, and additives. Dust-free closed pneumatic conveying systems are particularly effective in this sector due to their ability to handle large volumes and abrasive materials. The sealed pipelines prevent dust from contaminating the surrounding environment, which is crucial in urban or residential areas near cement plants. The systems also reduce the need for manual handling, improving operational efficiency and worker safety. Applications include the transport of raw materials to cement kilns and the distribution of finished cement products to construction sites.
5. Plastics and Polymer Manufacturing
In the plastics and polymer industry, the transport of powders and granules requires systems that prevent material degradation and contamination. HeadPowder's dust-free closed systems are designed to handle a variety of polymers, including polyethylene, polypropylene, and PVC. The gentle conveying action minimizes particle breakage, preserving the material's properties for downstream processing. The sealed environment prevents moisture and dust from entering the material stream, which is critical for maintaining product quality. These systems are commonly used in the production of plastic pellets, resins, and other polymer-based materials.
Key Advantages and Operational Benefits
HeadPowder's dust-free closed pneumatic conveying systems offer several advantages that make them a preferred choice in diverse industrial settings. These include:
1. Environmental Compliance and Safety
The primary advantage of closed systems is their ability to prevent dust emissions, which aligns with environmental regulations and enhances workplace safety. By containing all material handling within a sealed environment, these systems reduce the risk of airborne contaminants, protecting both workers and the surrounding community. This is particularly important in industries where air quality standards are strict, such as pharmaceuticals and food processing.
2. Material Integrity and Purity
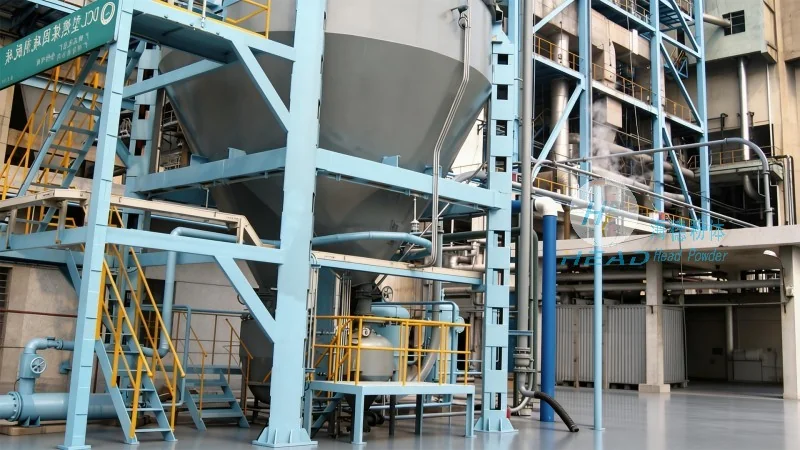
The sealed design of the system ensures that materials remain uncontaminated throughout the conveying process. This is critical for products that require high purity, such as pharmaceuticals, food ingredients, and chemicals. The gentle handling and lack of exposure to external elements preserve the material's properties, ensuring consistent quality in the final product.
3. Operational Efficiency and Cost Savings
Dust-free closed systems are designed for high throughput and low maintenance, leading to operational efficiency and cost savings. The sealed pipelines reduce the need for cleaning and maintenance compared to open systems, as there is no accumulation of dust or material on external surfaces. Additionally, the systems can be integrated with automated controls, allowing for precise material flow and reducing labor costs.
4. Flexibility and Adaptability
HeadPowder's systems are customizable to meet the specific needs of different industries and applications. Whether handling fine powders or bulk granules, the systems can be adjusted to accommodate varying material characteristics, flow rates, and distances. This flexibility makes them suitable for a wide range of working scenes, from small-scale laboratory applications to large-scale industrial operations.
Conclusion
HeadPowder's dust-free closed material pneumatic conveying systems represent a cutting-edge solution for modern industrial material handling. By combining the fundamental principles of pneumatic transport with a sealed, enclosed design, these systems offer unparalleled benefits in terms of environmental compliance, material purity, and operational efficiency. The working scene characteristics highlighted in this article demonstrate the versatility and adaptability of these systems across various industries, making them an essential component of contemporary industrial operations. With a strong commitment to quality and innovation, HeadPowder continues to provide reliable and effective solutions for businesses seeking to optimize their material handling processes.