

Principle and Working Scene Characteristics of Sintered Ash Powder Pneumatic Conveying Equipment
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems for sintered ash powders. With a strong focus on innovation and industrial application, the company provides efficient solutions for handling and transporting sintered ash, a byproduct commonly found in industrial processes such as sintering and waste management.
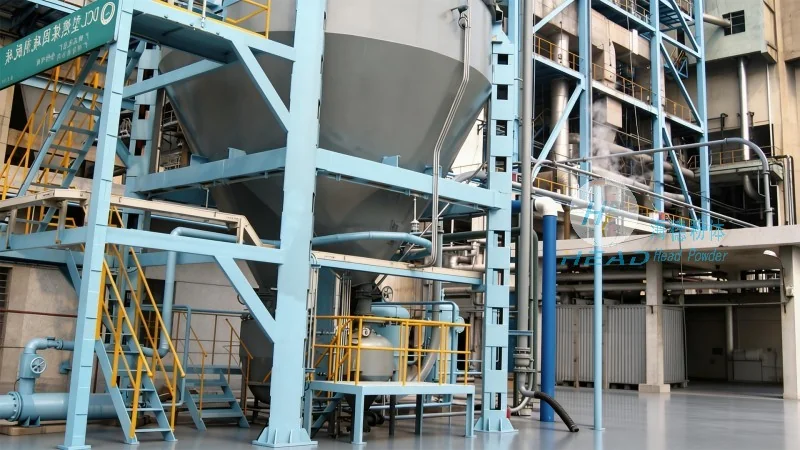
Company Profile and Core Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is dedicated to delivering high-performance pneumatic conveying equipment tailored for sintered ash powder applications. The company's headquarters is located in Shandong, China, where it leverages local industrial resources and expertise to develop cutting-edge solutions. HeadPowder's team of engineers and technicians possess extensive experience in material handling technologies, ensuring that each product meets stringent industry standards and customer requirements.
The Principle of Pneumatic Conveying for Sintered Ash Powders
Pneumatic conveying, as a non-contact material transport method, operates by utilizing pressurized or suction air to move powders through a pipeline. For sintered ash powders, which are typically fine and abrasive, the equipment must be designed to handle these characteristics effectively. The core principle involves creating a flow of air that lifts and transports the powder particles, preventing blockages and ensuring consistent performance. Key components of the system include a feeding unit, a conveying pipeline, a separation and collection system, and a control unit. The feeding unit ensures the sintered ash is introduced into the pipeline at a controlled rate, while the conveying pipeline transports the mixture of air and powder. The separation system then separates the powder from the air, allowing the ash to be collected for further processing or disposal. This process is typically automated, with sensors and controls monitoring pressure, flow rate, and particle size to maintain optimal operation.
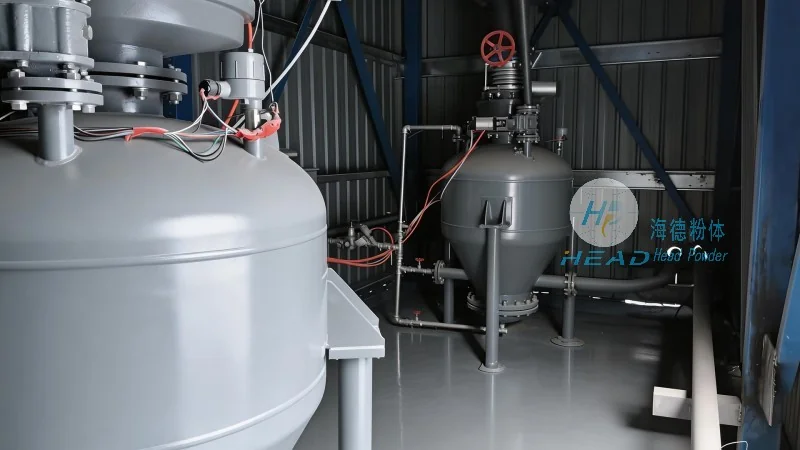
Working Scene Characteristics and Application Scenarios
The working scene characteristics of sintered ash powder pneumatic conveying equipment are tailored to meet the demands of various industrial environments. These systems are commonly used in sintering plants, where the ash is generated as a byproduct of the sintering process. The equipment is designed to handle high volumes of fine powders over varying distances, from short-range internal transport to long-distance external delivery. One key characteristic is the ability to operate in both positive and negative pressure modes, providing flexibility in different application settings. For example, in a sintering plant, the equipment may be used to transport ash from the sintering furnace to a storage silo or to an off-site disposal facility. The working scene also considers environmental factors, such as dust control and noise reduction, as sintered ash can be a fine particulate that requires proper handling to comply with environmental regulations. Additionally, the equipment is designed for durability and low maintenance, as it operates in harsh conditions with abrasive materials. The working scene characteristics highlight the importance of system efficiency, reliability, and adaptability to meet the diverse needs of industrial clients.
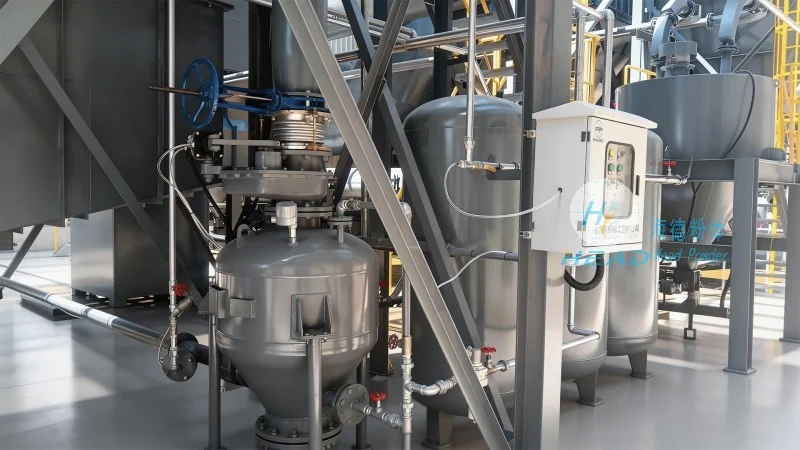
Advantages and Technical Features
HeadPowder's sintered ash powder pneumatic conveying equipment offers several advantages that make it a preferred choice in industrial applications. The primary advantage is the efficiency in transporting fine powders without the need for mechanical components like belts or buckets, reducing wear and maintenance costs. The system is also highly flexible, allowing for changes in flow rate and distance without significant modifications. Another key feature is the ability to handle abrasive materials like sintered ash, which can cause wear on traditional equipment. The equipment incorporates materials such as stainless steel and wear-resistant coatings to extend the lifespan of components. Furthermore, the system is equipped with advanced control technologies, including real-time monitoring and automatic adjustments, ensuring stable operation and minimizing downtime. These technical features contribute to the overall reliability and performance of the equipment, making it suitable for continuous industrial operations.
Conclusion and Future Outlook
In summary, the sintered ash powder pneumatic conveying equipment developed by HeadPowder combines advanced engineering principles with practical application considerations. By understanding the unique properties of sintered ash and the demands of industrial working scenes, the company has created a reliable and efficient solution for material handling. As industrial processes continue to evolve, the demand for specialized equipment like this will likely increase, and HeadPowder is positioned to meet these needs with its expertise and commitment to innovation. The company's focus on customer-specific solutions and continuous improvement ensures that its products remain at the forefront of material handling technology, providing long-term value to clients in the sintering and related industries.