

Principle and Working Scene Characteristics of Bentonite Powder Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. The company is headquartered in Shandong, China, and has established a strong reputation for delivering reliable and efficient solutions tailored to the unique needs of various industrial sectors. This article provides an in-depth exploration of the principles underlying bentonite powder pneumatic conveying systems, as well as the key characteristics of their operational scenarios.
Understanding the Core Principles of Bentonite Powder Pneumatic Conveying
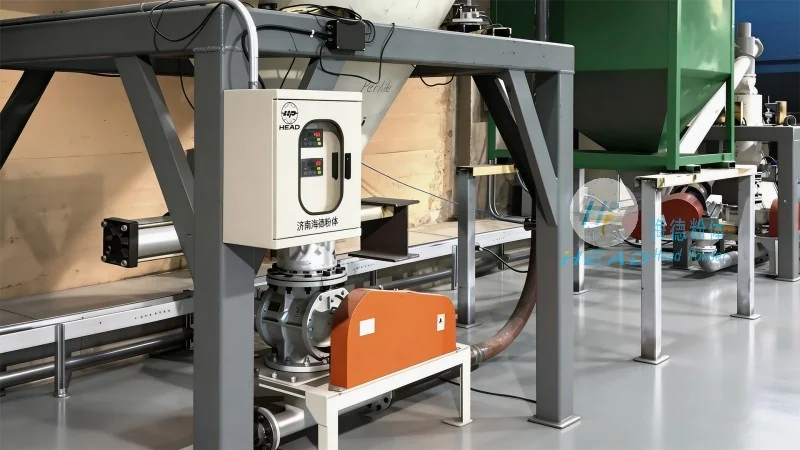
Bentonite powder pneumatic conveying systems operate on the fundamental principle of transporting dry powders through a pipeline using a stream of air or other gas. The process involves several critical components, including a material feeder, a pressure or vacuum source, a conveying line, and a separation or collection unit. The material feeder, often a rotary valve or a screw feeder, introduces the bentonite powder into the system at a controlled rate. This is followed by the introduction of air or gas, which creates a flow that carries the powder particles through the pipeline. The velocity of the air-gas mixture is carefully managed to ensure that the powder remains suspended and transported without clogging or degradation. The separation unit, typically a cyclone or a bag filter, then separates the powder from the air stream, allowing the bentonite to be collected in a designated container while the air is either recirculated or vented. This method offers significant advantages over traditional mechanical conveying methods, such as reduced equipment wear, lower maintenance requirements, and the ability to handle powders with varying properties, including those that are abrasive or prone to agglomeration.
Key Working Scene Characteristics of Bentonite Powder Pneumatic Conveying Systems
The operational characteristics of bentonite powder pneumatic conveying systems are highly dependent on the specific application and the environment in which they are deployed. Several key factors define their performance and suitability in different working scenarios:
1. Efficiency and Throughput in Industrial Production
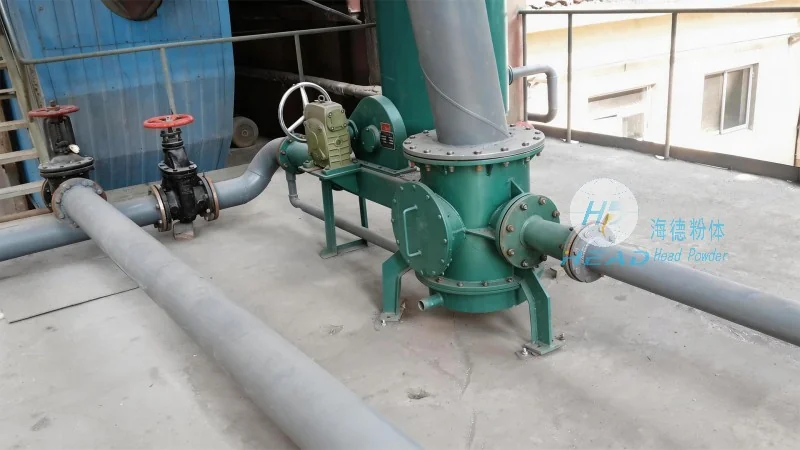
In industrial settings, such as chemical manufacturing or construction material production, the efficiency of material transport is paramount. Bentonite powder pneumatic conveying systems are designed to achieve high throughput rates, often ranging from several tons per hour to tens of tons per hour, depending on the system configuration. The continuous and unobstructed flow of powder ensures that production lines operate smoothly, minimizing downtime and maximizing productivity. The system's ability to handle large volumes of bentonite powder without the need for manual handling or intermediate storage makes it an ideal choice for high-volume production environments.
2. Versatility Across Diverse Powder Properties
Bentonite powders can exhibit a wide range of physical properties, including varying particle sizes, moisture content, and flowability. The pneumatic conveying system's adaptability to these variations is a critical characteristic. For instance, systems can be adjusted to handle fine powders that require high air velocities to remain suspended, or coarser powders that can be conveyed at lower velocities. Additionally, the system can accommodate powders with different moisture levels, as the air-gas mixture helps to maintain the powder's dryness during transport, preventing clumping or caking. This versatility allows the system to be applied across multiple industries, from pharmaceuticals to mining, where bentonite is used as a processing aid or a final product.
3. Space Efficiency and Layout Flexibility
One of the notable advantages of pneumatic conveying systems is their ability to transport materials over long distances and through complex layouts without the need for extensive mechanical infrastructure. This is particularly beneficial in facilities where space is limited or where the layout requires the powder to be moved from one location to another in a non-linear path. The system's compact design, with components such as the feeder and separator often integrated into a single unit, reduces the footprint required for installation. Furthermore, the flexibility in pipeline routing allows for easy integration with existing production lines or equipment, minimizing the need for major structural modifications. This characteristic makes the system suitable for both new installations and retrofits in existing facilities.
4. Environmental and Safety Considerations
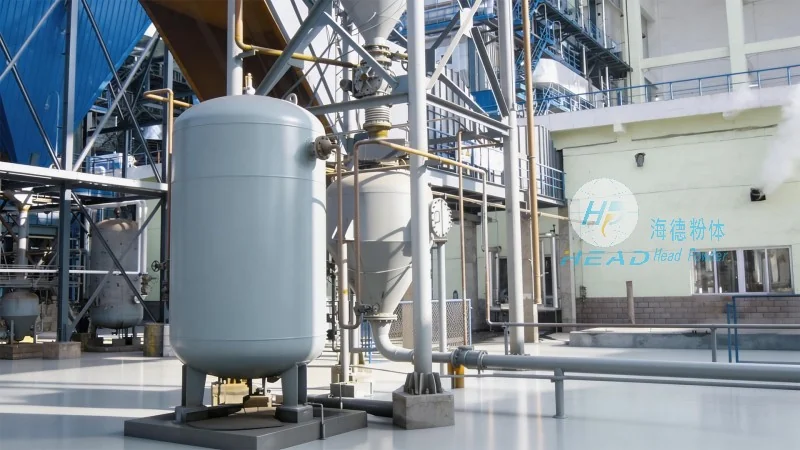
In modern industrial operations, environmental and safety standards are of utmost importance. Bentonite powder pneumatic conveying systems are designed with these considerations in mind. The sealed pipeline system prevents dust emissions, reducing the risk of inhalation by workers and minimizing environmental contamination. The separation unit, equipped with filtration systems, ensures that any airborne particles are captured and contained, adhering to regulatory requirements for air quality. Additionally, the system's operation under controlled pressure or vacuum conditions reduces the risk of accidental spills or leaks, enhancing workplace safety. These features make the system not only efficient but also compliant with contemporary environmental and safety regulations.
Conclusion: The Role of Shandong HeadPowder in Advancing Bentonite Powder Conveying Technology
Shandong HeadPowder Engineering Co., Ltd. plays a pivotal role in advancing the technology and application of bentonite powder pneumatic conveying systems. By leveraging decades of experience and a commitment to innovation, the company has developed systems that meet the demanding requirements of various industries. The principles of efficient air-based transport, combined with the operational characteristics tailored to diverse working scenarios, make these systems a reliable and cost-effective solution for bentonite powder handling. As industries continue to seek more efficient and sustainable material transport solutions, the expertise and products offered by Shandong HeadPowder remain at the forefront of the field, ensuring that bentonite powder can be handled safely, effectively, and with minimal environmental impact.