

Principle and Working Scene Characteristics of Powder Tank Truck Bulk Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design and implementation of advanced bulk material handling solutions. Among their offerings is the powder tank truck bulk pneumatic conveying system, a critical technology for efficiently transporting powders and granules over long distances. This system combines the capabilities of pneumatic transport with the mobility of a tank truck, providing a versatile solution for various industrial applications.
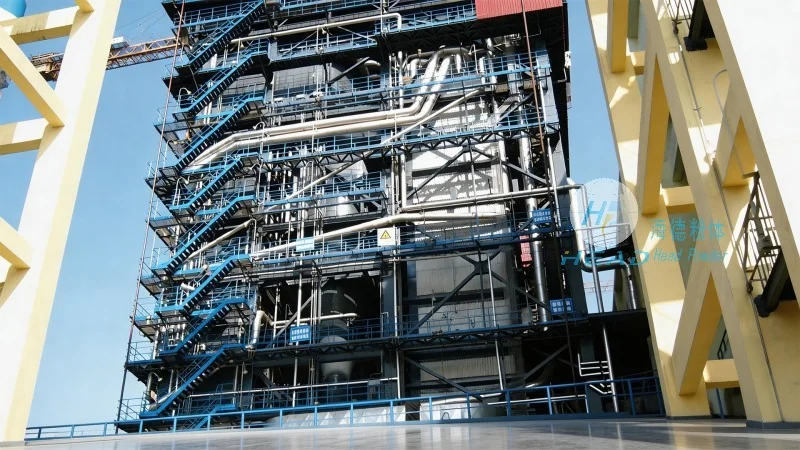
The Fundamental Principle of Pneumatic Conveying in Powder Tank Trucks
The core principle of the bulk pneumatic conveying system in a powder tank truck revolves around the use of compressed air to move dry bulk materials. The system operates by creating a pressure differential between the tank and the discharge point. When the tank is filled with the powder, the air compressor generates high-pressure air that is introduced into the tank. This air flows through the material, lifting and transporting it through the pipeline to the destination. The process is controlled by a series of valves, filters, and pressure regulators to ensure smooth and efficient material flow. The system can handle a wide range of materials, from fine powders like cement and flour to bulk granules such as sugar and chemicals, making it adaptable to diverse industrial needs.
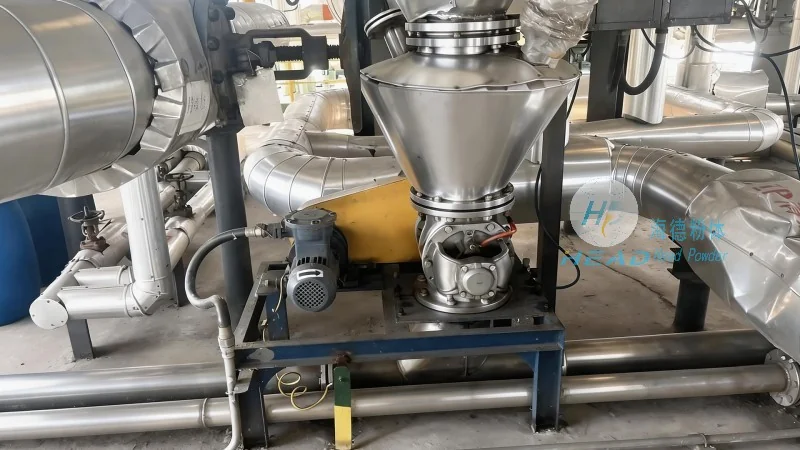
Key Working Scene Characteristics and Applications
The working scene characteristics of the powder tank truck bulk pneumatic conveying system are defined by its mobility and the ability to handle large volumes of material. In industrial settings, this system is often used in scenarios where materials need to be transported from a production facility to a processing plant or a storage site. For example, in the cement industry, the system can transport raw materials or finished cement products from a quarry to a manufacturing plant. In the food processing industry, it can move ingredients like flour or sugar from a warehouse to a production line. The system's flexibility allows it to operate in both indoor and outdoor environments, making it suitable for various operational conditions. Additionally, the system is designed to minimize material degradation and contamination, ensuring that the transported powders remain in optimal condition. This is achieved through features such as air filtration systems and sealed pipelines, which prevent dust and moisture from entering the material stream.
Advantages and Operational Efficiency in Industrial Environments
One of the primary advantages of the bulk pneumatic conveying system in a powder tank truck is its ability to achieve high material throughput with minimal labor. The system operates automatically once set up, reducing the need for manual handling and lowering the risk of workplace accidents. Furthermore, the system is energy-efficient compared to traditional methods like truck loading or conveyor belts, as it uses compressed air to move materials rather than mechanical force. This results in lower operational costs and reduced environmental impact. The system also offers enhanced safety features, such as automatic shut-off valves and pressure relief systems, which protect both the equipment and the personnel operating it. In terms of maintenance, the system is designed for easy access to components, allowing for quick repairs and minimizing downtime. This makes it a reliable choice for continuous industrial operations.
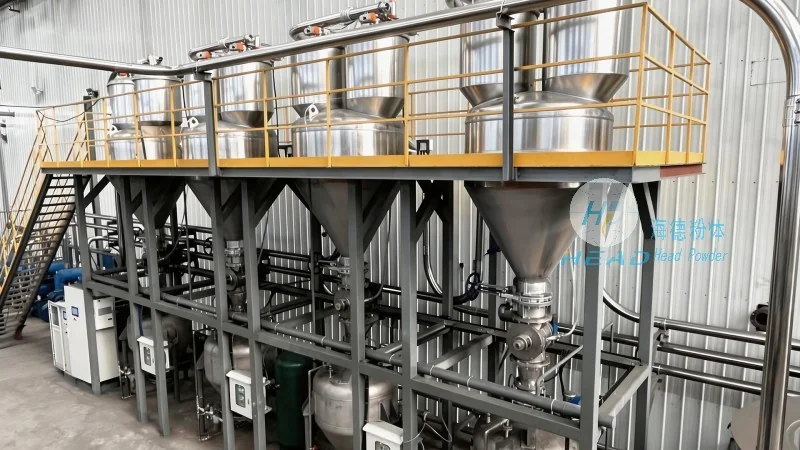
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in bulk material handling to provide effective solutions through the powder tank truck bulk pneumatic conveying system. By combining advanced engineering with practical application, the company ensures that its systems meet the specific needs of various industries. The system's ability to handle diverse materials, operate in different environments, and deliver high efficiency makes it a valuable asset for businesses seeking reliable and efficient material transport solutions. With a focus on quality and customer satisfaction, headpowder continues to innovate and improve its products to meet the evolving demands of the industrial sector.