

Principles and Working Scene Characteristics of Brown Sugar Material Conveying
Understanding the principles and operational characteristics of brown sugar material conveying systems is crucial for optimizing production efficiency in sugar processing facilities. As a leading engineering company, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing advanced material handling solutions tailored to the unique demands of brown sugar production. This article explores the core principles behind these systems and highlights the key working scene characteristics that define their effective application.
The Fundamental Principles of Material Handling in Brown Sugar Production
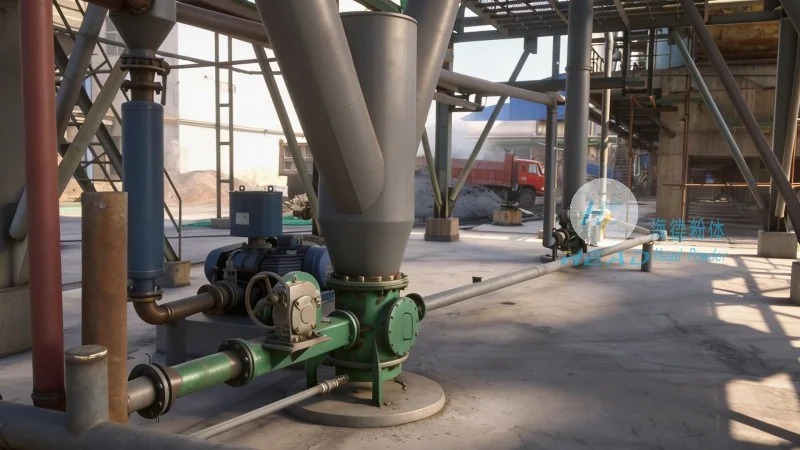
In brown sugar manufacturing, material conveying systems rely on a combination of physical principles to transport raw materials and finished products efficiently. The primary mechanisms include gravitational force, mechanical power, and fluid dynamics, each adapted to handle the specific properties of brown sugar materials such as sugarcane residues, molasses, and crystallized sugar. For instance, belt conveyors utilize mechanical tension and friction to move bulk materials over long distances, while bucket elevators employ centrifugal force to lift materials vertically. These principles are critical for maintaining consistent flow rates and minimizing material degradation during transport. The selection of appropriate conveying equipment depends on factors like material density, moisture content, and the required throughput, ensuring that the system operates within optimal parameters for the brown sugar production process.
Key Working Scene Characteristics and Applications
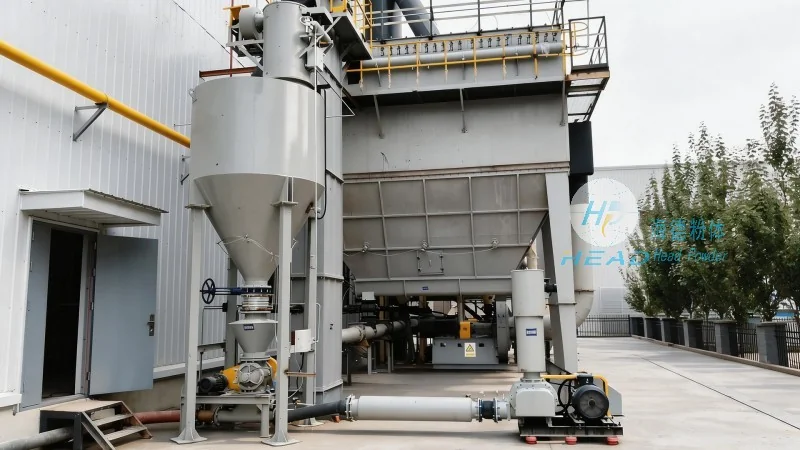
The effectiveness of brown sugar material conveying systems is heavily influenced by the specific working scenes in which they are deployed. In sugar factories, these systems operate in diverse environments, from raw material storage areas to processing lines and packaging stations. One key characteristic is the need for systems that can handle high-volume, continuous flow, as sugar production often involves large-scale processing of sugarcane or sugar beets. For example, in the initial stages of production, raw sugarcane is delivered to the factory and transported via conveyor belts to the crushing and extraction units. This initial conveying stage must be robust enough to handle the heavy, irregularly shaped cane, requiring durable belts and heavy-duty rollers. As the material progresses through the process, it may be converted into molasses or crystallized sugar, each requiring different conveying methods. Molasses, being a viscous liquid, is typically transported using pipelines or screw conveyors, while crystallized sugar, which is granular, is often handled by bucket elevators or pneumatic conveyors. The working scene also includes considerations for environmental conditions, such as temperature and humidity, which can affect material properties and equipment performance. In humid climates, for instance, materials may become sticky, requiring specialized equipment like belt cleaners or lubricated bearings to prevent clogging. Additionally, the need for hygiene and sanitation in food processing facilities means that conveying systems must be designed with easy-to-clean surfaces and minimal dead zones to prevent contamination. These working scene characteristics highlight the importance of customizing material handling solutions to match the specific operational requirements of brown sugar production.
How Shandong HeadPowder Engineering Co., Ltd. Applies These Principles in Practical Operations
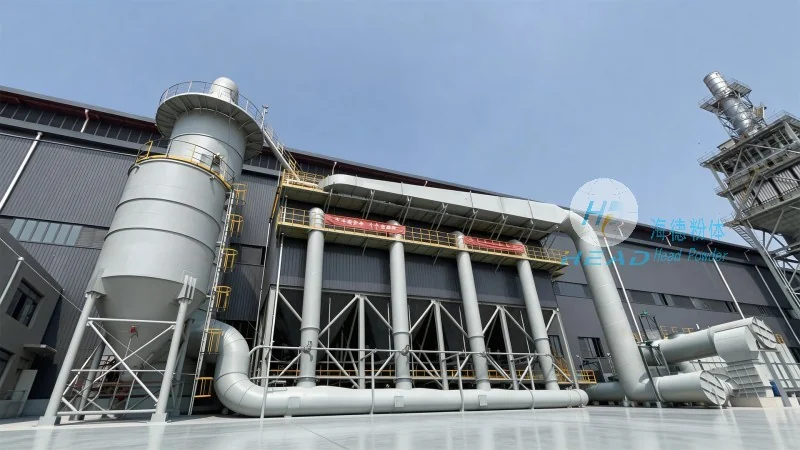
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in mechanical engineering and material science to design and manufacture conveying systems that address the unique challenges of brown sugar production. The company’s approach involves a thorough analysis of the client’s production process, including the type of raw materials, processing stages, and operational environment. By understanding these factors, HeadPowder engineers can select the most appropriate conveying equipment and configure it to meet the specific needs of the facility. For example, in a large-scale sugar factory, the company might design a combination of belt conveyors for horizontal transport and bucket elevators for vertical lifting, ensuring seamless integration between different processing units. The design process also considers maintenance and operational costs, with components selected for durability and ease of replacement. HeadPowder’s team of experienced engineers works closely with clients to develop customized solutions, from initial concept to final installation and commissioning. The company’s commitment to quality is evident in its adherence to industry standards and rigorous testing protocols, ensuring that each conveying system meets the highest performance and safety requirements. Through its practical application of fundamental principles and tailored solutions, Shandong HeadPowder Engineering Co., Ltd. helps sugar manufacturers optimize their material handling processes, improve efficiency, and enhance overall production output. The company’s reputation for reliability and innovation has made it a trusted partner for brown sugar production facilities across China and beyond.