

Principles and Working Scene Characteristics of Fully Automatic Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier of powder handling equipment based in Shandong, China. The company specializes in the design, development, and production of advanced fully automatic powder conveying systems that meet the demands of various industrial sectors. With a strong focus on innovation and precision engineering, headpowder has established itself as a trusted partner for businesses seeking reliable and efficient solutions for powder transportation and processing.
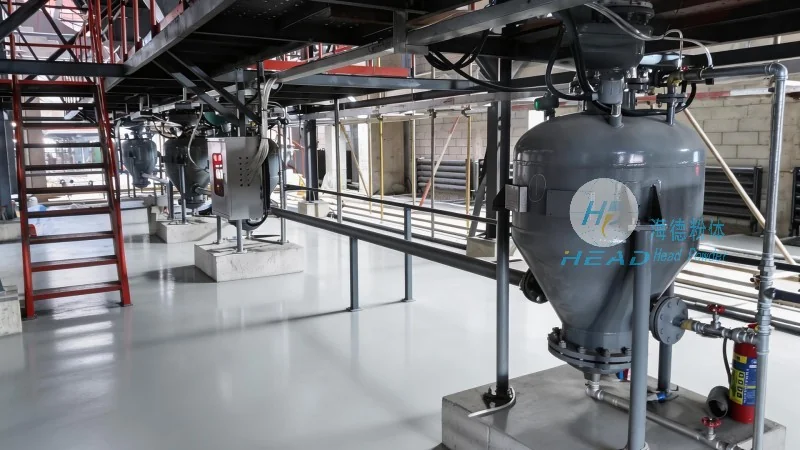
Introduction to Fully Automatic Powder Conveying Systems
A fully automatic powder conveying system is a sophisticated piece of industrial equipment designed to transport bulk powders from one location to another with minimal human intervention. These systems are engineered to handle a wide range of powder types, including fine powders, granules, and bulk materials, while ensuring consistent flow rates, accurate dosing, and safe operation. The core components of such systems typically include a hopper for material storage, a conveyor mechanism (such as screw conveyors, pneumatic systems, or vacuum pumps), control panels with sensors, and automated valves or gates. The integration of these components allows for seamless, continuous operation, reducing downtime and increasing productivity in manufacturing processes.
Principles of Operation for Fully Automatic Powder Conveying Systems
The operation of a fully automatic powder conveying system is based on a combination of mechanical, pneumatic, and electronic principles. The system begins with the material being loaded into the hopper, where it is held until the conveying process is initiated. Sensors, such as level detectors or pressure sensors, monitor the material level and flow conditions, providing real-time data to the control system. The control panel processes this information and activates the conveyor mechanism, which may involve rotating screws, air pressure to move material through pipes, or a combination of both. Automated valves and gates are used to regulate the flow rate and direct the powder to the desired destination, such as a processing unit, storage silo, or packaging line. The system also includes safety features like overload protection, emergency stop buttons, and alarms to prevent accidents and ensure operator safety. By leveraging these principles, the system maintains a stable and controlled flow of powder, minimizing the risk of clogging, spillage, or uneven distribution.

Key Working Scene Characteristics of Fully Automatic Powder Conveying Systems
The working scene characteristics of fully automatic powder conveying systems are tailored to meet the specific requirements of different industrial applications. In the chemical industry, for example, these systems are used to transport reactive powders or hazardous materials, where precision and safety are paramount. The systems are equipped with explosion-proof components and sealed containers to prevent contamination and ensure compliance with safety regulations. In the pharmaceutical industry, the systems are designed to handle sterile powders, with features like HEPA filters and sterile air handling to maintain a clean environment and prevent cross-contamination. The food and beverage industry utilizes these systems for transporting ingredients like flour, sugar, or spices, where hygiene and product purity are critical. The systems are constructed from food-grade materials and are easy to clean and sanitize. In the mining and mineral processing sector, fully automatic powder conveying systems are employed to transport raw materials like ores or minerals from storage to processing plants. The robust design and high capacity of these systems make them suitable for heavy-duty applications, with features like wear-resistant liners and heavy-duty motors to withstand harsh operating conditions. Overall, the working scene characteristics of these systems are characterized by efficiency, reliability, and adaptability, making them indispensable in modern industrial operations.
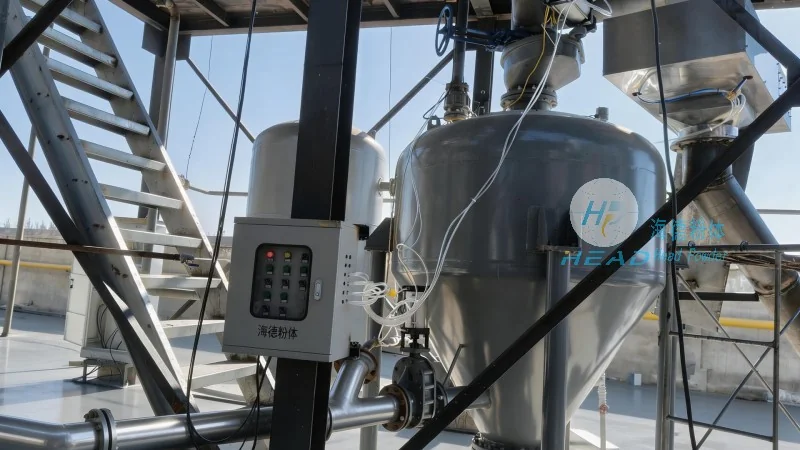
Advantages of Implementing Fully Automatic Powder Conveying Systems
Adopting a fully automatic powder conveying system offers numerous advantages for businesses across various industries. One of the primary benefits is increased productivity and efficiency. By automating the powder handling process, companies can reduce labor costs and minimize downtime caused by manual intervention. The systems operate continuously, ensuring a steady supply of materials to production lines, which leads to higher output and improved profitability. Another key advantage is improved safety and compliance. The automated systems eliminate the need for workers to handle powders manually, reducing the risk of dust inhalation, chemical exposure, or physical injuries. The integrated safety features, such as emergency stop buttons and overload protection, further enhance workplace safety and help companies meet regulatory requirements. Additionally, fully automatic powder conveying systems provide greater accuracy and consistency in material flow. The precise control of flow rates and dosing ensures that the right amount of powder is delivered to the processing unit, reducing waste and improving product quality. The systems also offer better monitoring and data collection capabilities, allowing businesses to track material usage, identify bottlenecks, and optimize their operations. Overall, the implementation of these systems contributes to a more streamlined, efficient, and safe industrial environment.
Conclusion: The Role of Fully Automatic Powder Conveying Systems in Modern Manufacturing
As industries continue to evolve and demand higher standards of efficiency and safety, fully automatic powder conveying systems play a crucial role in modern manufacturing. These systems represent the pinnacle of powder handling technology, combining advanced engineering, automation, and precision to meet the diverse needs of various sectors. By leveraging the principles of mechanical and electronic control, these systems ensure reliable and consistent operation, while their working scene characteristics are tailored to specific industrial requirements. The advantages of implementing such systems, including increased productivity, improved safety, and enhanced product quality, make them a valuable investment for businesses looking to stay competitive in today's market. With the continued innovation in powder handling technology, fully automatic powder conveying systems will likely become even more sophisticated, offering new capabilities and further enhancing their role in industrial operations. For companies seeking to optimize their powder handling processes, partnering with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. can provide the expertise and solutions needed to achieve their operational goals.