

Working Principle and Features of Air-Pneumatic Conveyors for Lightweight Aggregate Materials
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of air-pneumatic conveyors tailored for the transportation of lightweight aggregate materials. This article provides an in-depth exploration of the working principle and key features of these specialized equipment, offering valuable insights for industries relying on efficient material handling solutions.
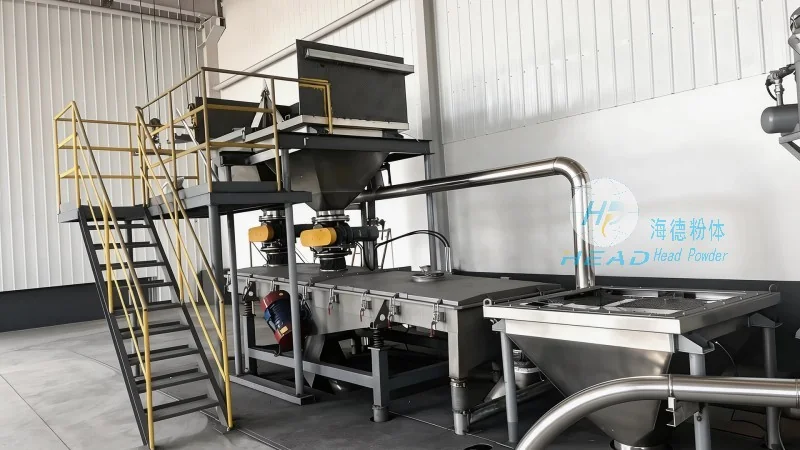
Understanding the Working Principle of Air-Pneumatic Conveyors for Lightweight Aggregates
The air-pneumatic conveyor system for lightweight aggregates operates on the principle of using compressed air to move bulk materials through a pipeline network. At its core, the system comprises a series of components including a blower, hopper, and discharge nozzle, all integrated to facilitate the seamless transfer of materials. The process begins with the lightweight aggregate being loaded into the hopper, where it is then drawn into the pipeline by the suction created by the blower. As the material travels through the pipeline, it is propelled by the airflow, ensuring a continuous and controlled flow. The discharge nozzle at the receiving end regulates the material's release, allowing for precise control over the delivery process. This method eliminates the need for mechanical parts like belts or buckets, reducing maintenance requirements and enhancing operational efficiency.
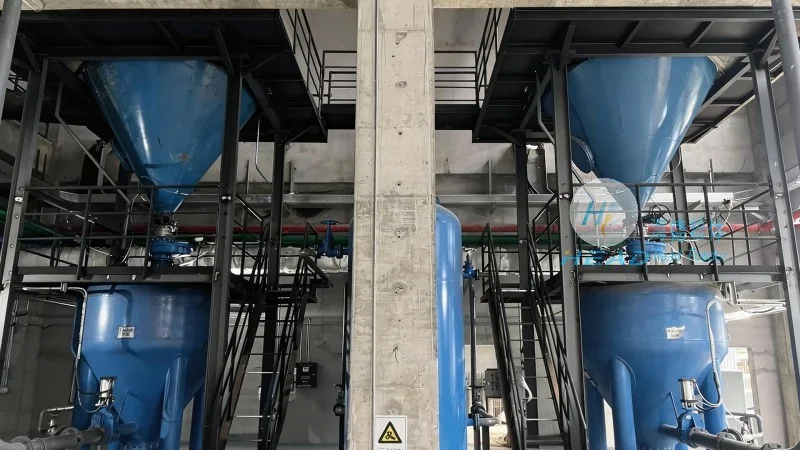
Key Features of Air-Pneumatic Conveyors for Lightweight Aggregate Materials
HeadPowder's air-pneumatic conveyors for lightweight aggregates are designed with several distinctive features that enhance their performance and suitability for various applications. Firstly, the system offers high flexibility in terms of layout, as it can be easily adapted to different plant configurations without the need for extensive structural modifications. The use of flexible hoses or rigid pipelines allows for curved or vertical transport, making it ideal for complex production environments. Secondly, the conveyor is highly efficient in terms of energy consumption, as the compressed air system operates with minimal power input, resulting in lower operational costs over time. Additionally, the system provides excellent material handling capabilities, as it can transport lightweight aggregates with minimal degradation or segregation, preserving the quality of the material. Another notable feature is the low maintenance requirement, as the absence of moving parts reduces the likelihood of mechanical failures and simplifies routine upkeep. The system also ensures a clean and dust-free operation, as the enclosed pipeline design prevents material spillage and dust emissions, contributing to a safer working environment. Furthermore, the air-pneumatic conveyor allows for easy integration with other processing equipment, such as mixers or storage silos, enabling a streamlined production workflow. These features collectively make the air-pneumatic conveyor an optimal choice for industries seeking reliable and efficient material handling solutions for lightweight aggregate materials.
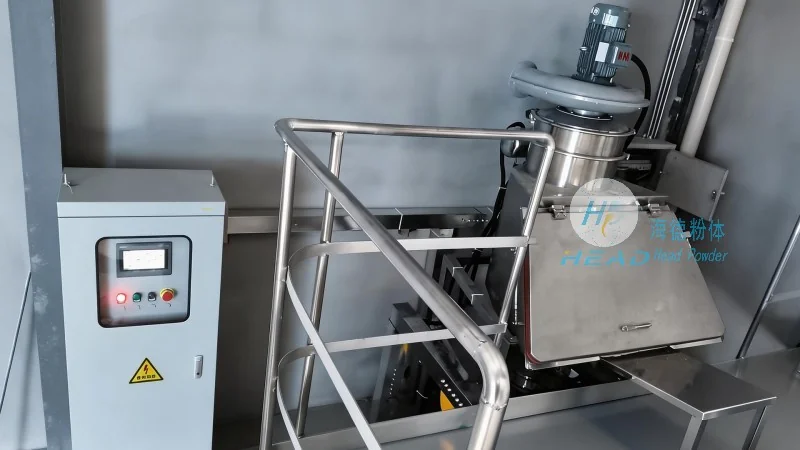
Applications and Benefits in the Construction Industry
The air-pneumatic conveyors developed by HeadPowder find extensive applications in the construction industry, particularly in the production of lightweight concrete and other building materials. The ability to transport lightweight aggregates efficiently and with minimal loss makes these conveyors indispensable in concrete mixing plants and precast concrete facilities. By ensuring a consistent supply of aggregates to the mixing process, the conveyor helps maintain the quality and consistency of the final product. Additionally, the system's flexibility allows for the integration into existing production lines, reducing downtime and enhancing overall productivity. The low maintenance and energy-efficient operation also contribute to cost savings for construction companies, as they can reduce operational expenses and extend the lifespan of the equipment. The dust-free operation is particularly beneficial in construction sites, as it minimizes health hazards and compliance issues related to dust emissions. Overall, the air-pneumatic conveyor for lightweight aggregates offers significant advantages in terms of efficiency, cost-effectiveness, and operational safety, making it a preferred choice for modern construction operations.
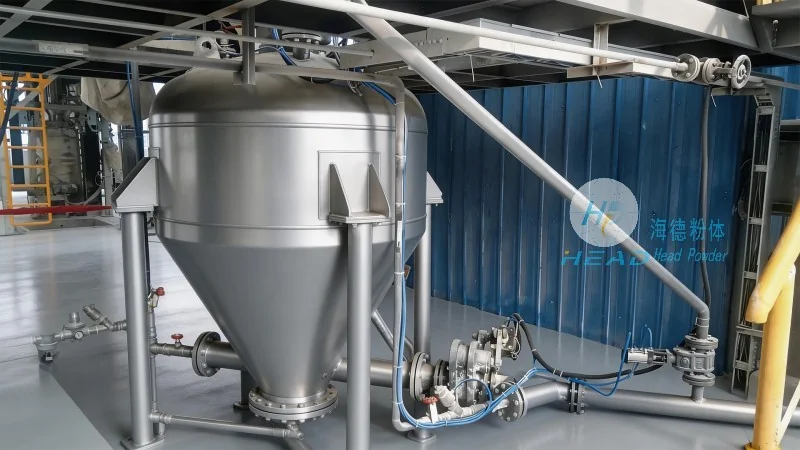
Conclusion
HeadPowder's air-pneumatic conveyors for lightweight aggregate materials represent a sophisticated solution for efficient material handling in various industrial applications. By leveraging the principles of air-pneumatic transport, these systems provide a reliable, flexible, and low-maintenance method for moving lightweight aggregates. The key features, including high efficiency, low energy consumption, and easy integration, make them suitable for diverse production environments. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of industries relying on lightweight aggregate materials. The air-pneumatic conveyor not only enhances operational efficiency but also contributes to cost savings and improved working conditions, solidifying its position as a critical component in modern material handling systems.