

Inert Gas Circulation Pneumatic Conveying Line: Working Principles and Features
Inert gas circulation pneumatic conveying systems represent a sophisticated method for transporting bulk materials, particularly in industries where material purity and process safety are paramount. These systems utilize inert gases, such as nitrogen or carbon dioxide, to create a controlled environment that prevents oxidation or contamination of the conveyed material. The technology is widely applied in sectors like pharmaceuticals, food processing, and chemical manufacturing, where maintaining material integrity is critical.
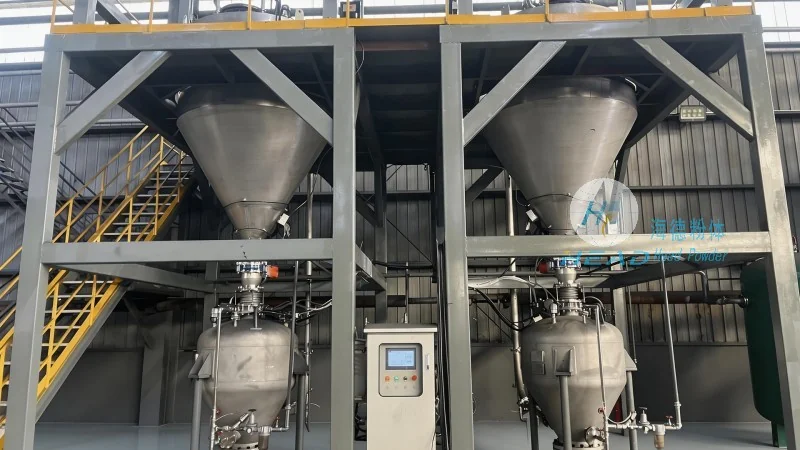
Working Principles of the Inert Gas Circulation Pneumatic Conveying Line
The core operation of an inert gas circulation system involves a closed-loop gas circuit that continuously recirculates the inert gas through the conveying line. The process begins with the material being fed into a hopper or feeder, where it is then drawn into the conveying line by the pressure differential created by the gas flow. The inert gas, typically compressed and filtered, is introduced at the discharge end or through a venturi, ensuring that the material is carried along the pipeline by the gas stream. The system maintains a consistent gas pressure and flow rate, which is crucial for controlling the velocity of the material and preventing blockages or degradation.
Key components of the system include the gas compressor, filtration unit, conveying pipeline, and material separation equipment. The gas compressor pressurizes the inert gas to the required level, while the filtration system removes any contaminants that could affect the material or the system's performance. The conveying pipeline is designed with appropriate diameters and bends to minimize pressure loss and ensure smooth material flow. At the receiving end, a separator or cyclone separates the material from the gas, allowing the gas to be recirculated back to the compressor, thus completing the closed-loop operation.
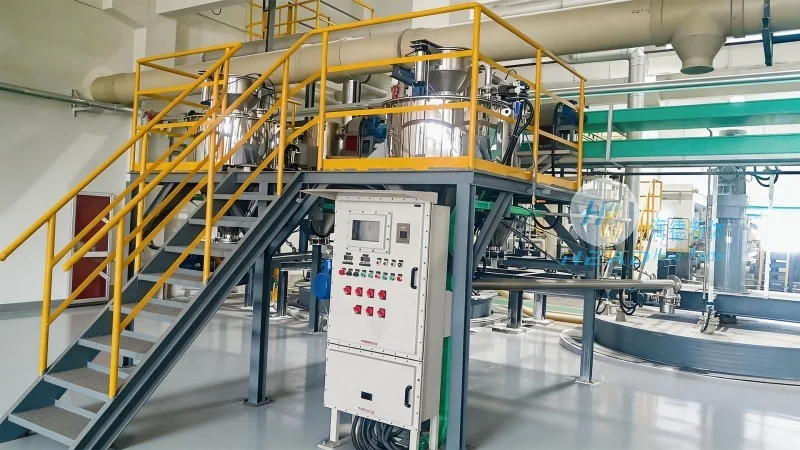
Key Features and Advantages of Inert Gas Circulation Pneumatic Conveying
One of the primary advantages of inert gas circulation systems is their ability to maintain a contamination-free environment, which is essential for sensitive materials. By using inert gases, the system prevents oxidation, moisture absorption, or chemical reactions that could alter the material's properties. This feature makes it ideal for transporting products like pharmaceutical powders, food ingredients, and high-value chemicals where purity is non-negotiable.
Another significant feature is the energy efficiency and cost-effectiveness of the closed-loop system. Since the gas is recirculated rather than vented to the atmosphere, the system reduces energy consumption and operational costs compared to open-loop systems. The recirculation also minimizes waste and environmental impact, aligning with sustainability goals in modern manufacturing.
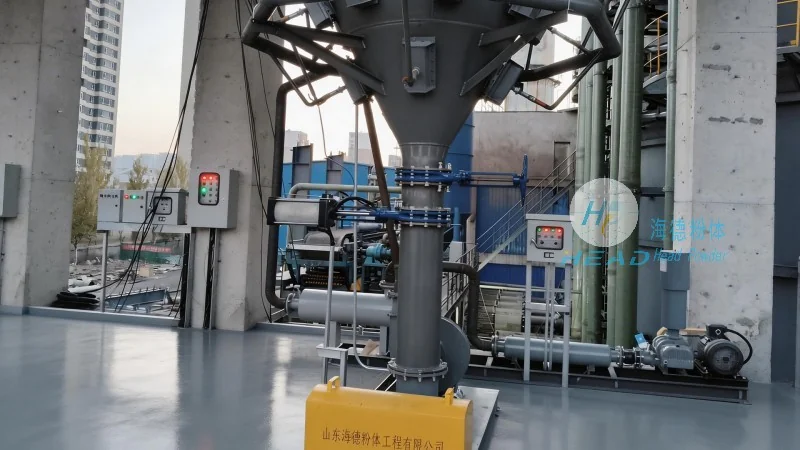
The system's flexibility is another notable characteristic. It can handle a wide range of material types, from fine powders to bulk solids, and can be adapted to various process requirements through adjustments in gas flow rate, pressure, and pipeline configuration. This adaptability makes it suitable for diverse applications, from small-scale laboratory operations to large-scale industrial production lines.
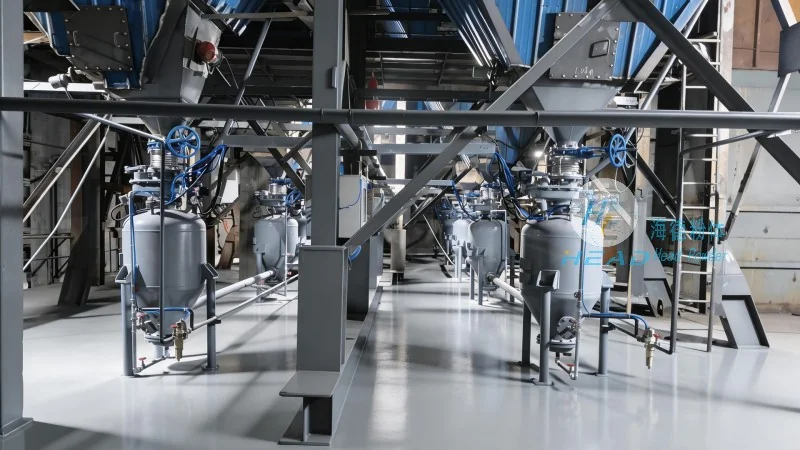
Additionally, inert gas circulation systems offer enhanced safety features. The closed-loop design eliminates the risk of gas leaks or exposure to hazardous materials, and the inert gas itself reduces the risk of fire or explosion in environments where flammable materials are present. This safety aspect is particularly important in industries where compliance with strict safety regulations is mandatory.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing inert gas circulation systems tailored to the specific needs of various industries. With headquarters in Shandong, China, the company leverages decades of experience in material handling technology to deliver high-quality, reliable equipment. HeadPowder's commitment to innovation and customer satisfaction ensures that their systems meet the most stringent industry standards while providing long-term operational efficiency.