

Working Principle and Features of Air-Powered Stone Aggregate Conveying Equipment
For industries dealing with stone aggregates, efficient and reliable material handling is crucial. The air-powered conveying system, as offered by Shandong HeadPowder Engineering Co., Ltd., provides a sophisticated solution for transporting stone aggregates with precision and minimal maintenance. This equipment is designed to handle various types of stone materials, ensuring consistent performance in demanding applications.
Working Principle of the Air-Powered Conveying System
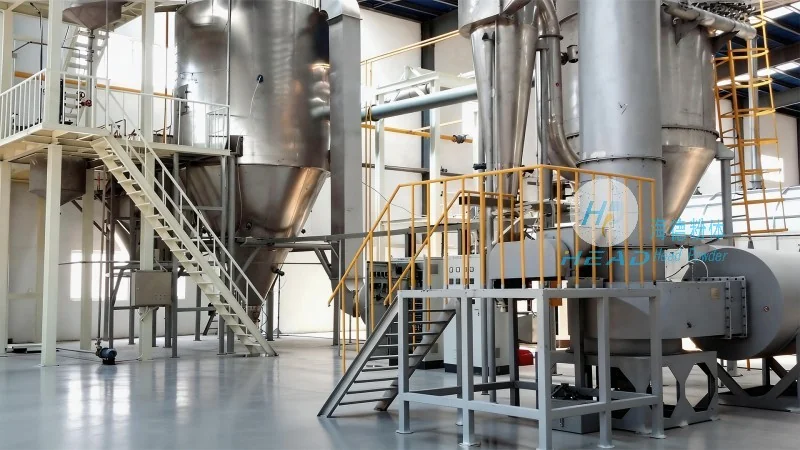
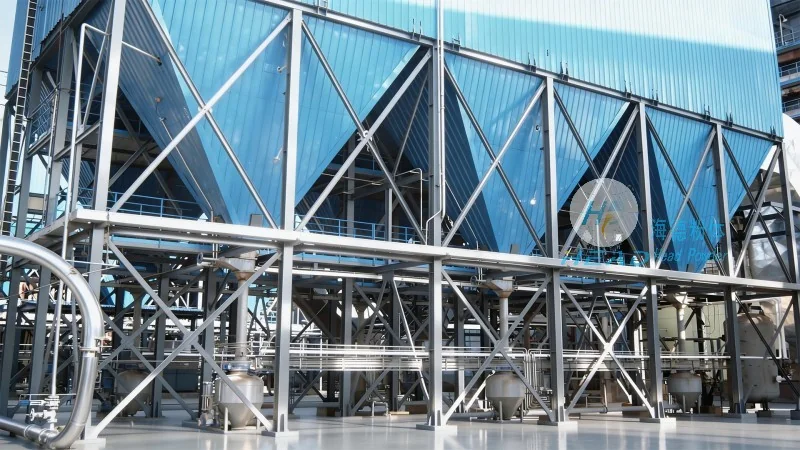
The core of the air-powered stone aggregate conveying equipment lies in its pneumatic transport mechanism. The system operates by using a high-pressure air stream to move the material through a pipeline. As the air flows, it entrains the stone particles, creating a dense phase flow that ensures efficient transportation. The process involves several key components: a blower or compressor to generate the air pressure, a hopper or feeder to introduce the material, and a pipeline network that directs the material to its destination. The air velocity is carefully controlled to maintain the optimal flow rate, preventing material degradation and ensuring smooth operation. This pneumatic method eliminates the need for mechanical components like belts or chains, reducing wear and tear and extending the equipment's service life.
Key Features of the Stone Aggregate Conveying Equipment
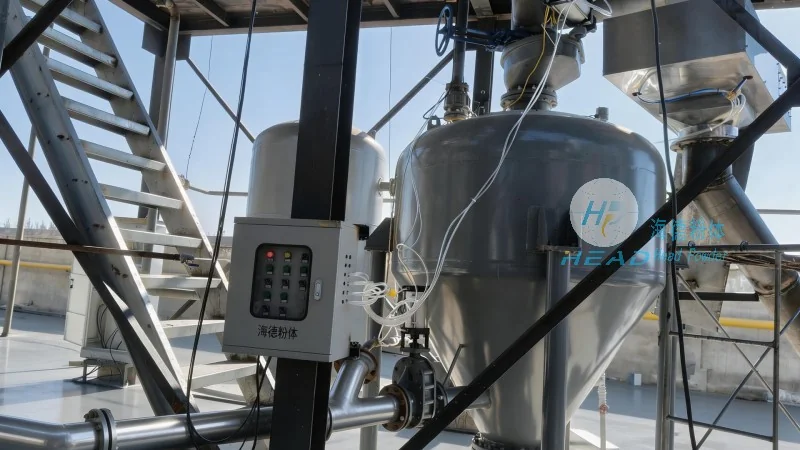
Shandong HeadPowder Engineering Co., Ltd.'s air-powered stone aggregate conveying equipment is distinguished by several advanced features that enhance its performance and usability. Firstly, the system offers high conveying capacity, capable of transporting large volumes of stone aggregates over long distances with minimal energy consumption. The adjustable air pressure and flow rate allow operators to customize the conveying speed according to the material type and application requirements, ensuring flexibility in various production settings. Secondly, the equipment is designed for low maintenance, with components such as the blower and pipeline constructed from durable materials that resist corrosion and abrasion. This reduces downtime and operational costs, making it an economical choice for long-term use. Additionally, the system is equipped with safety features, including pressure relief valves and material flow sensors, to prevent overloading and ensure safe operation. The compact design of the equipment also allows for easy integration into existing production lines, minimizing installation time and space requirements.
Advantages in Industrial Applications
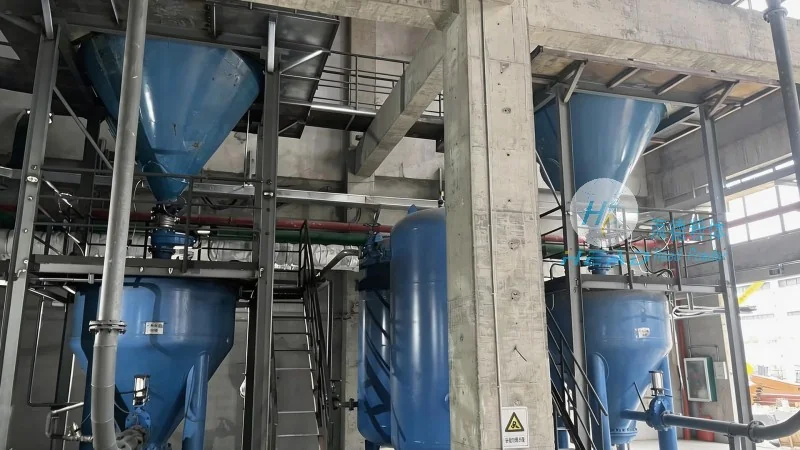
The air-powered stone aggregate conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers significant advantages in industrial applications, particularly in construction and mining sectors. One of the primary benefits is the ability to transport materials in a dust-free environment, which improves workplace safety and reduces the risk of respiratory issues for operators. The pneumatic system also allows for the conveyance of materials through vertical and horizontal paths, providing flexibility in layout design. This is particularly useful in facilities where space is limited or where the material needs to be elevated to different levels. Furthermore, the system's ability to handle a wide range of stone aggregate sizes and types makes it versatile for various projects, from small-scale construction sites to large-scale mining operations. The consistent and reliable performance of the equipment ensures that production processes are not interrupted, leading to increased productivity and reduced operational costs.