

Working Principle and Features of Intelligent Tonne Bag Feeding Station Material Pneumatic Conveying
Intelligent tonne bag feeding stations equipped with pneumatic conveying systems represent a sophisticated solution for material handling in industrial settings. These systems are designed to efficiently transfer bulk materials from large tonne bags into processing equipment, streamlining operations and enhancing productivity. The following sections will explore the working principle and key features of such equipment, providing a comprehensive understanding of its functionality and benefits.
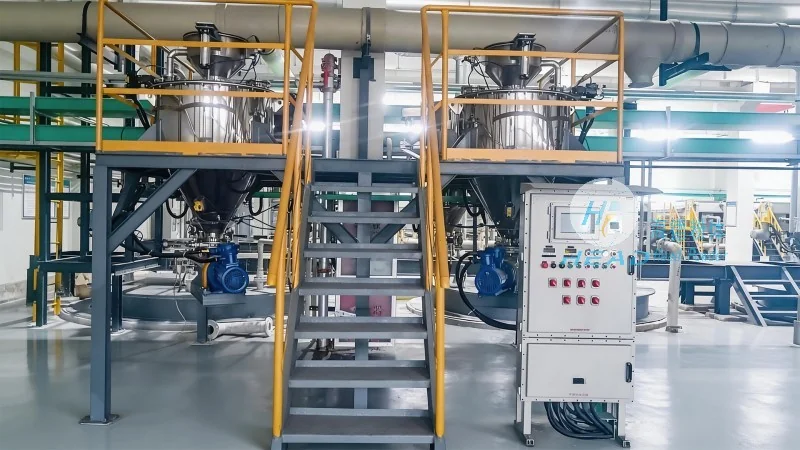
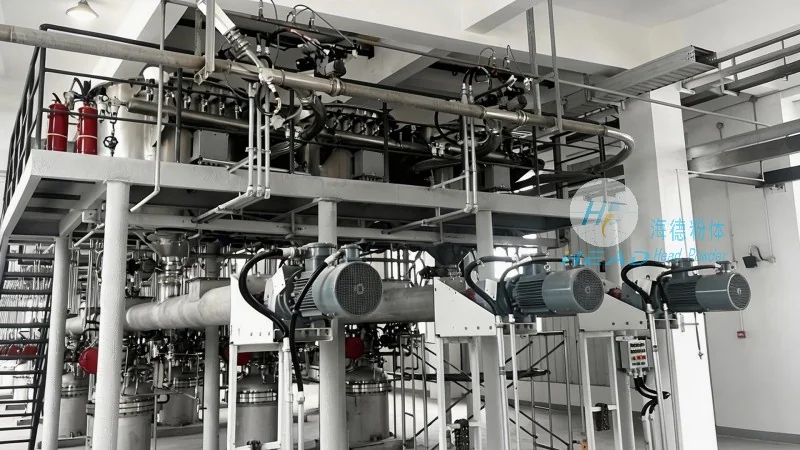
Working Principle of the Intelligent Tonne Bag Feeding Station Pneumatic Conveying Equipment
The core mechanism of the intelligent tonne bag feeding station relies on pneumatic conveying technology, which utilizes compressed air to transport bulk materials. The process typically begins with the placement of a tonne bag onto a specialized feeding platform. A hopper or receiving chamber is then positioned beneath the bag, and a valve system is activated to open the bag's discharge port. Simultaneously, a compressor generates high-pressure air that is directed into the conveying line. As the air flows through the line, it creates a negative pressure or a flow of air that pulls the material from the bag into the hopper. The material is then carried through the pipeline to the processing equipment, such as a mixer or a reactor, where it is used for production. The system may also include a dust collection unit to ensure environmental compliance and maintain air quality. The intelligent aspect of the station often involves automated controls, such as sensors and programmable logic controllers (PLCs), which monitor the bag's weight, the flow rate of material, and the pressure of the air system. These controls help optimize the conveying process, prevent blockages, and ensure consistent material delivery. The entire operation is designed to be seamless and efficient, minimizing manual intervention and reducing the risk of material loss or contamination.
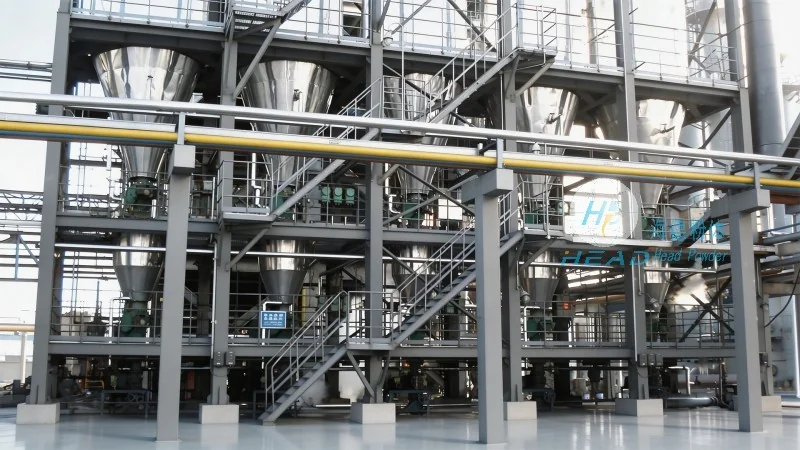
Key Features of the Intelligent Tonne Bag Feeding Station Pneumatic Conveying Equipment
The intelligent tonne bag feeding station offers several notable features that enhance its performance and usability. Firstly, the system is highly automated, with integrated sensors and controls that allow for real-time monitoring and adjustment of the conveying process. This automation reduces the need for manual labor, lowers labor costs, and minimizes human error. Secondly, the equipment is designed for high efficiency, capable of handling large volumes of material quickly and reliably. The use of pneumatic conveying allows for continuous operation, as the material can be fed into processing equipment without interruption, which is crucial for maintaining production schedules. Thirdly, the system is equipped with safety features to protect both personnel and equipment. These may include emergency stop buttons, pressure relief valves, and sensors that detect blockages or leaks, preventing accidents and equipment damage. Additionally, the intelligent station often includes a dust suppression system, which captures and filters airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment. The equipment is also designed for easy maintenance, with accessible components and clear diagnostic indicators that help technicians identify and resolve issues quickly. This reduces downtime and extends the lifespan of the system. Furthermore, the station can be customized to meet specific operational requirements, such as different material types, bag sizes, or conveying distances. This flexibility makes it suitable for a wide range of industrial applications, from chemical processing to food manufacturing. The combination of automation, efficiency, and safety makes the intelligent tonne bag feeding station a valuable asset for any facility that handles bulk materials.
Company Information
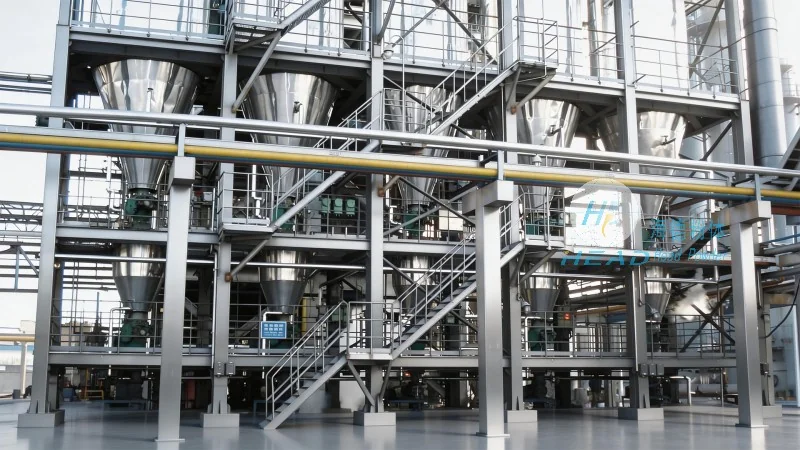
HeadPowder, a leading provider of material handling solutions, specializes in the design, manufacturing, and installation of intelligent tonne bag feeding stations and pneumatic conveying systems. With headquarters in Shandong, China, HeadPowder Engineering Co., Ltd. has established itself as a trusted partner in the industry, delivering high-quality equipment that meets the needs of various sectors. The company's commitment to innovation and customer satisfaction has enabled it to develop advanced solutions that enhance operational efficiency and reduce costs for its clients. HeadPowder's products are engineered to withstand the demands of industrial environments, ensuring durability and reliability over the long term. The company also provides comprehensive after-sales support, including installation, training, and maintenance services, to ensure that customers can maximize the benefits of their equipment. By leveraging its expertise in pneumatic conveying technology, HeadPowder continues to set new standards in material handling, helping businesses improve their productivity and achieve their operational goals.