

Working Principle and Features of Food Additive Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer based in Shandong, China. The company specializes in the research, development, and production of advanced powder conveying systems, particularly those designed for the food additive industry. These systems are engineered to meet the stringent requirements of food processing, ensuring safety, efficiency, and hygiene throughout the powder handling process.
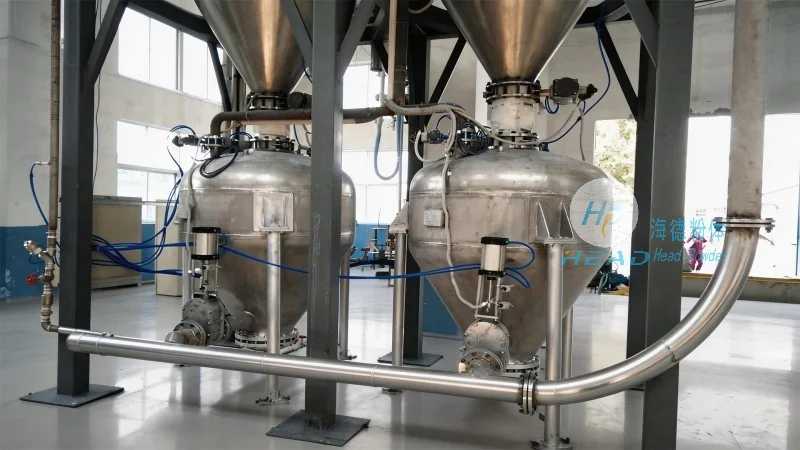
Overview of Food Additive Powder Conveying Systems
Food additive powder conveying systems are essential equipment in the food manufacturing industry. They are responsible for the safe and efficient transportation of various food additives, such as colorants, flavor enhancers, preservatives, and nutritional supplements, from storage to processing lines. The systems must comply with food safety regulations and maintain the integrity of the powder, preventing contamination and degradation. headpowder's systems are designed to address these challenges with innovative solutions tailored to the unique properties of different food additives.
Working Principle of the Powder Conveying System
The core working principle of headpowder's food additive powder conveying system involves the use of a combination of mechanical and pneumatic components to transport dry powders. The system typically starts with a hopper or silo that stores the food additive powder. From there, the powder is fed into a conveyor section, which may include screw conveyors, pneumatic ducts, or a combination of both. The mechanical part, such as a screw or auger, moves the powder along a defined path, while the pneumatic component uses compressed air to create a flow that assists in the transport. This dual approach ensures reliable and consistent powder movement, even for powders with varying flow characteristics. The system is equipped with sensors and controls to monitor the flow rate, pressure, and other critical parameters, allowing for real-time adjustments to maintain optimal performance. The design also incorporates sanitary features, such as stainless steel construction and easy-to-clean components, to meet the high standards of food processing environments.
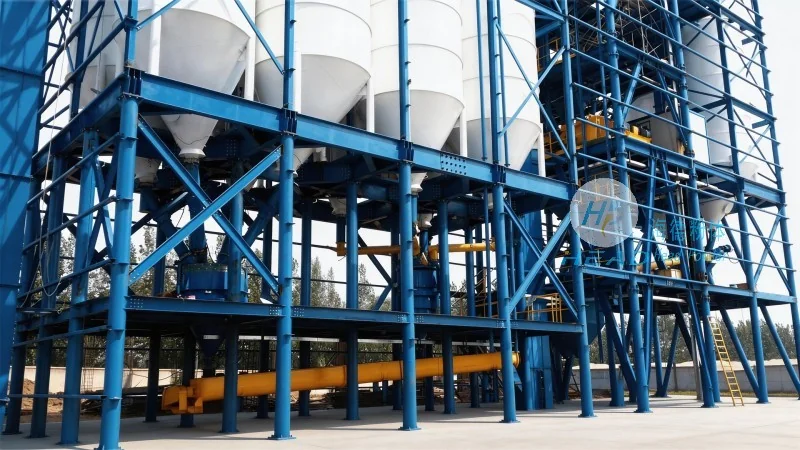
Key Features of the Food Additive Powder Conveying System
headpowder's food additive powder conveying system is characterized by several key features that enhance its performance and usability. Firstly, the system is highly efficient in terms of energy consumption and operational speed, minimizing downtime and maximizing production throughput. The use of advanced materials and engineering ensures durability and long service life, reducing maintenance costs over time. Secondly, the system is designed with hygiene and safety in mind. All components are made from food-grade stainless steel, and the system includes features like air filtration and dust collection to prevent cross-contamination and protect operators from exposure to powders. Thirdly, the system offers flexibility in terms of customization. It can be adapted to handle different types of food additives, from fine powders to bulk materials, and can be integrated with existing production lines without significant modifications. The control system is user-friendly, with intuitive interfaces that allow operators to monitor and adjust settings easily. Additionally, the system is equipped with safety interlocks and emergency stop mechanisms to ensure operator safety during operation. These features collectively make the system a reliable and versatile solution for food additive powder handling in various industrial applications.
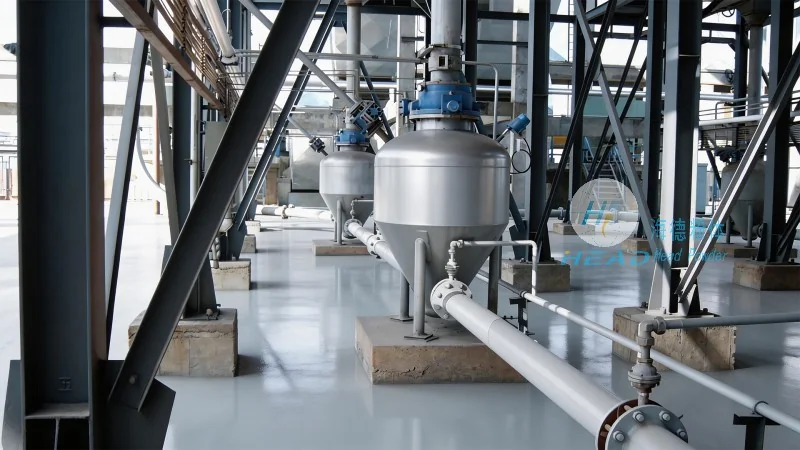
Application and Benefits in Food Processing
The food additive powder conveying system from headpowder is widely used in the food processing industry for its ability to handle a variety of food additives with precision and efficiency. The system is particularly beneficial in applications where consistent powder flow and minimal product loss are critical. For example, in the production of beverages, the system can deliver flavor enhancers and colorants to mixing tanks with exact dosing, ensuring product quality and consistency. In the manufacturing of baked goods, the system can transport preservatives and nutritional supplements to mixing equipment, maintaining the integrity of the ingredients. The system's ability to maintain a sterile environment and prevent contamination makes it suitable for sensitive food products, such as dairy and confectionery items. Overall, the benefits of using headpowder's system include improved production efficiency, reduced labor costs, enhanced product quality, and compliance with food safety regulations. The system's reliability and durability also contribute to lower maintenance and operational costs, making it a cost-effective solution for food manufacturers.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s food additive powder conveying system is a sophisticated piece of equipment designed to meet the demanding requirements of the food processing industry. By combining advanced mechanical and pneumatic technologies with robust engineering and sanitary design, the system ensures efficient, safe, and reliable transportation of food additives. The key features, such as energy efficiency, hygiene, flexibility, and user-friendly controls, make it an ideal choice for food manufacturers seeking to optimize their powder handling processes. With its headquarters in Shandong, China, headpowder continues to innovate and provide high-quality solutions that enhance productivity and product quality in the food industry.