

Working Principle and Features of Dust Powder Conveyors
For industries dealing with bulk materials, efficient and reliable dust powder conveyors are essential for maintaining productivity and safety. This article explores the working principle and key features of dust powder conveyors, highlighting how they enhance material handling processes.
Working Principle of Dust Powder Conveyors
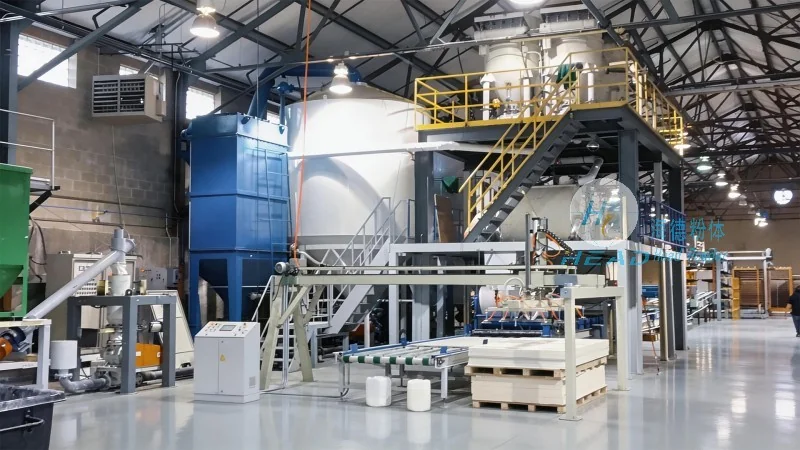
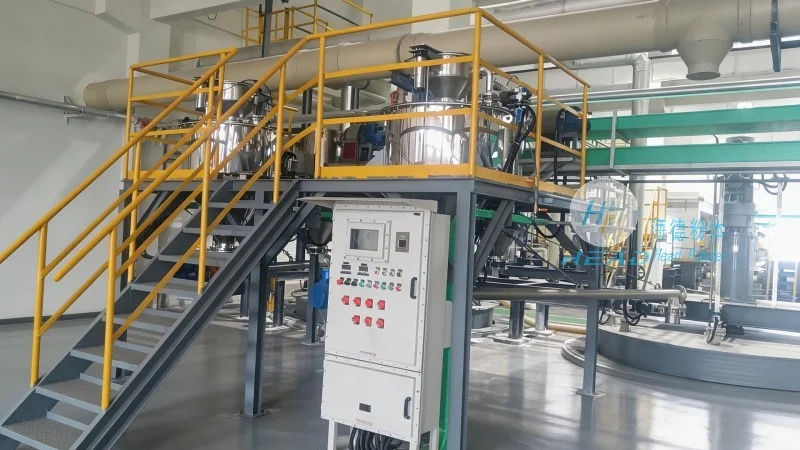
Dust powder conveyors operate on the principle of transporting dry powders and granular materials through a sealed system. The core mechanism involves using air or mechanical force to move the material from the source to the destination. Typically, these systems consist of a hopper, a conveyor tube, and a control unit. The material is fed into the hopper, where it is then drawn into the conveyor tube by a fan or a positive pressure system. As the air flows through the tube, it carries the powder particles along, ensuring a consistent and controlled flow. The design ensures minimal product degradation and contamination, making it suitable for sensitive materials like pharmaceuticals, food products, and chemicals.
Key Features of Dust Powder Conveyors
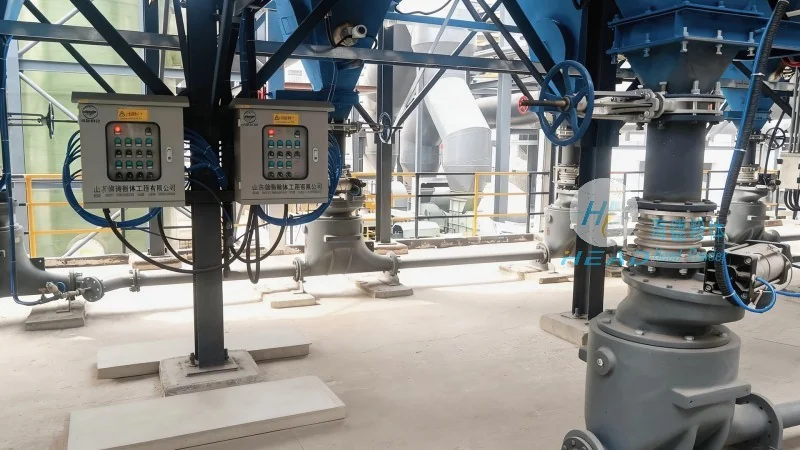
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers dust powder conveyors with several notable features. These include high efficiency in material transfer, low energy consumption, and a compact design that fits into various industrial settings. The conveyors are equipped with advanced control systems that allow for precise regulation of flow rates and pressure, ensuring optimal performance. Additionally, the sealed construction prevents dust emissions, complying with environmental regulations and enhancing workplace safety. The company’s products are designed for durability and easy maintenance, reducing downtime and operational costs for users.
Applications and Benefits
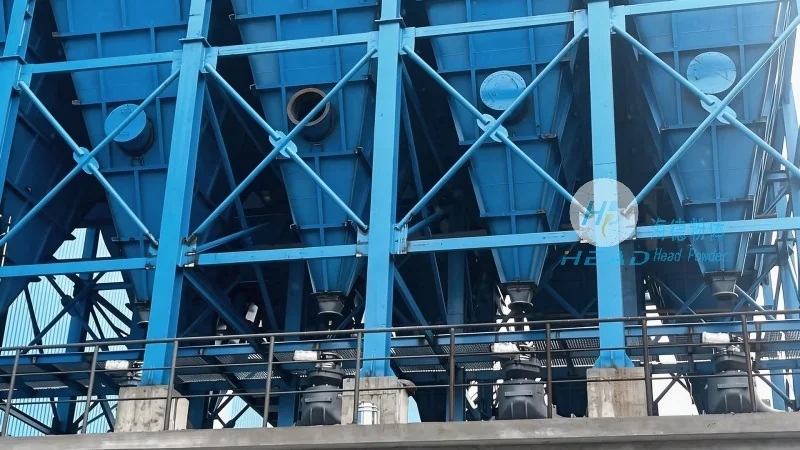
Dust powder conveyors are widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining. Their ability to handle fine powders without clogging or degradation makes them ideal for applications where material integrity is critical. The benefits extend beyond efficiency, as these systems also improve safety by containing dust and reducing the risk of explosions in hazardous environments. By integrating advanced technology and robust engineering, HeadPowder Engineering Co., Ltd. ensures that their conveyors meet the highest standards of performance and reliability, providing long-term value to their clients.