

What is a Wet Ammonium Nitrate Powder Pneumatic Conveying System? And What Are Its Design Principles
Wet ammonium nitrate (WAN) is a critical raw material in the fertilizer industry, and its efficient handling is essential for industrial operations. A wet ammonium nitrate powder pneumatic conveying system is a specialized equipment solution designed to transport this moisture-containing powder safely and effectively. This system plays a vital role in ensuring smooth material flow from storage to processing units, minimizing the risk of dust explosions and operational disruptions. Understanding the design principles behind such a system is crucial for optimizing performance and maintaining compliance with safety standards.
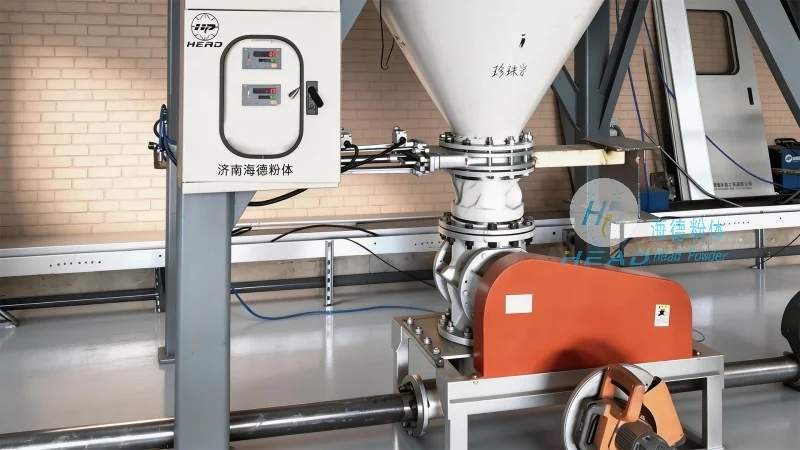
Key Components and Working Principle of the Wet Ammonium Nitrate Pneumatic Conveying System
The wet ammonium nitrate powder pneumatic conveying system typically consists of several key components that work in tandem to achieve efficient material transport. The primary components include a hopper for material storage, a rotary airlock valve to control the flow of powder into the system, a conveying pipeline, a dust collector to capture any airborne particles, and a receiver for the material at the destination. The system operates on the principle of pneumatic conveying, where air is used as the medium to move the powder particles through the pipeline. In this system, the air is often introduced under pressure, creating a flow that carries the wet ammonium nitrate particles from the source to the destination. The design must account for the moisture content in the powder, as this affects the air velocity required for effective transport and the overall system pressure. Proper sizing of the air compressor and pipeline diameter is essential to maintain the desired air velocity and prevent blockages or excessive energy consumption.
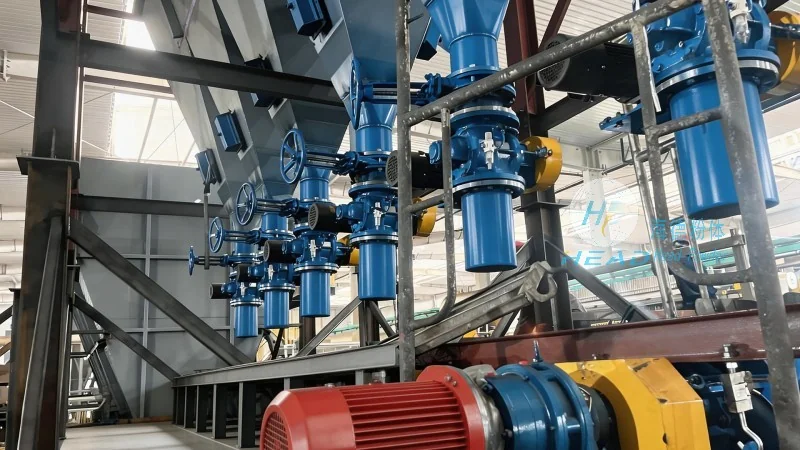
Design Considerations for Safety and Efficiency
When designing a wet ammonium nitrate powder pneumatic conveying system, several factors must be considered to ensure both safety and operational efficiency. Safety is paramount due to the explosive potential of ammonium nitrate dust. The system must incorporate explosion-proof components, such as air compressors and valves, and may include inert gas systems or explosion suppression devices to mitigate risks. Additionally, the design must account for the hygroscopic nature of wet ammonium nitrate, which can lead to caking or blockages in the pipeline. Anti-caking additives or regular cleaning procedures may be incorporated into the system to prevent these issues. From an efficiency standpoint, the system's design aims to minimize energy consumption while maximizing material throughput. This involves optimizing the air velocity, pipeline length, and diameter, as well as using efficient air separation and filtration systems to recover the powder and recycle the air. The use of variable frequency drives (VFDs) for the air compressor can also help adjust the system's performance based on the material flow rate, further enhancing energy efficiency.
Applications and Benefits in Industrial Settings
The wet ammonium nitrate powder pneumatic conveying system is widely used in fertilizer production facilities, where it facilitates the transport of wet ammonium nitrate from storage silos to mixing or granulation units. This system allows for a continuous and controlled flow of material, reducing downtime and improving overall production throughput. By eliminating the need for manual handling or mechanical conveyors, the system also reduces the risk of human error and workplace accidents. Furthermore, the pneumatic conveying process is gentle on the material, preserving its quality and preventing degradation that could occur with other transport methods. The system's ability to handle moisture-containing powders makes it particularly suitable for wet ammonium nitrate, which is prone to clumping or clogging in traditional conveyor systems. Overall, the wet ammonium nitrate powder pneumatic conveying system offers significant advantages in terms of safety, efficiency, and material handling in industrial applications.
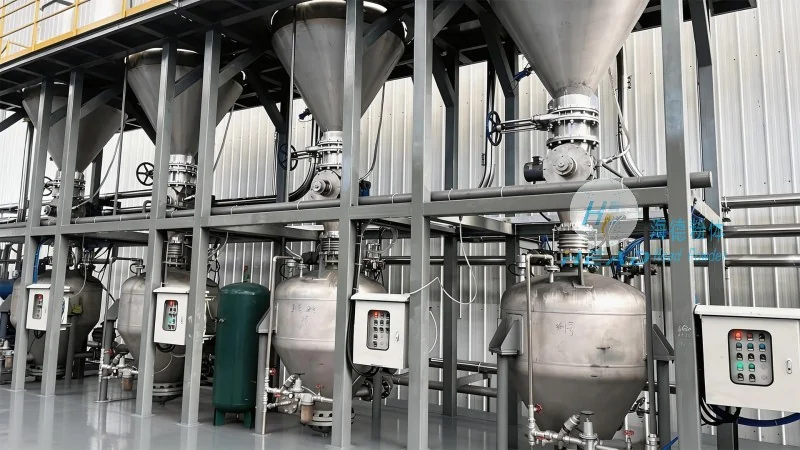
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of specialized powder handling equipment. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the fertilizer and chemical industries. The company specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of its clients, including wet ammonium nitrate powder handling solutions. HeadPowder's team of engineers and technicians leverages advanced technology and extensive industry experience to develop high-quality, reliable equipment that meets the stringent requirements of modern industrial operations. The company's commitment to quality and safety is reflected in its adherence to international standards and rigorous testing protocols. Based in Shandong, China, HeadPowder serves clients globally, providing comprehensive solutions that enhance operational efficiency and ensure compliance with industry regulations. Whether for new installations or system upgrades, HeadPowder offers expert guidance and support to help clients optimize their material handling processes and achieve their business objectives.