

What is a Bin Pump Material Handling System? What is its Design Principle?
Bin pumps, also known as bin discharge valves or pressure vessels, are critical components in bulk material handling systems. These systems are designed to transport dry bulk materials such as powders, granules, and granular substances from storage silos or hoppers to processing equipment, conveying systems, or other destinations. The bin pump material handling system combines the functions of material storage, feeding, and transportation, providing an efficient and reliable solution for industrial material handling applications.
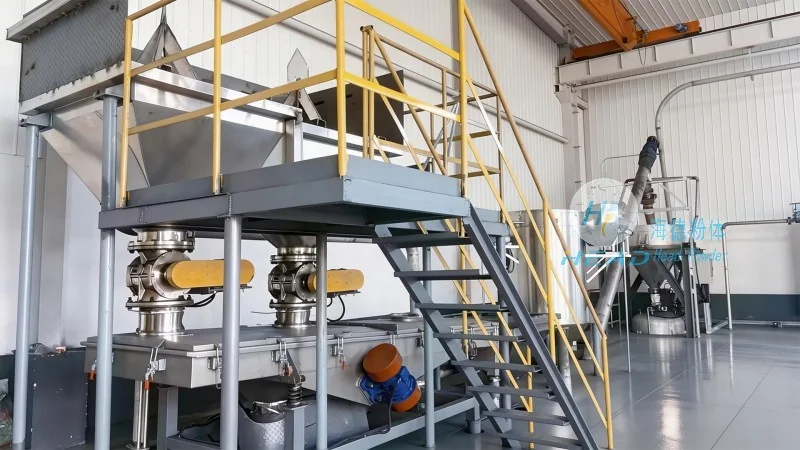
Understanding the Core Components of a Bin Pump System
A typical bin pump material handling system consists of several key components that work in tandem to ensure smooth material flow. The main elements include a hopper or storage silo, a bin pump unit (which houses the pumping mechanism), a control system, and associated piping or conveying equipment. The hopper serves as the storage vessel, while the bin pump unit is responsible for creating the pressure differential needed to move the material. The control system manages the operation of the pump, ensuring safe and efficient material discharge. Each component is engineered to handle specific material characteristics and operational requirements.
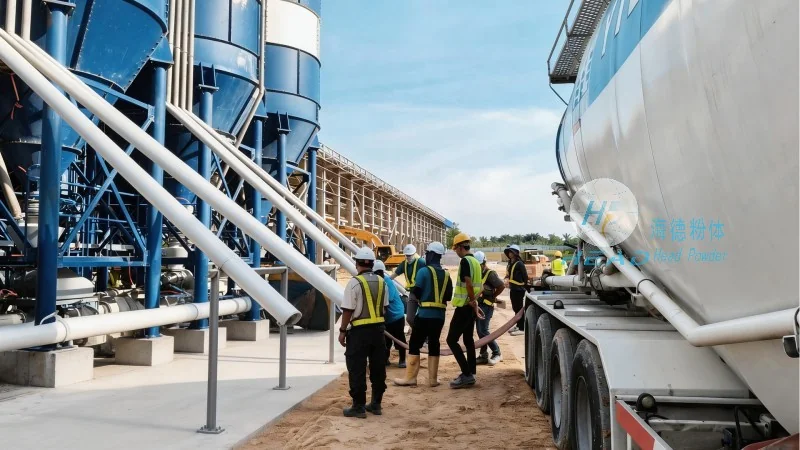
Design Principles of Bin Pump Material Handling Systems
The design of a bin pump material handling system is based on several fundamental principles that ensure optimal performance and reliability. One of the primary principles is the creation of a pressure differential between the hopper and the discharge point. This is achieved by using a diaphragm or piston within the bin pump unit, which alternately compresses and releases the material to generate the necessary pressure. The system is designed to handle a wide range of material densities, flow rates, and particle sizes, making it versatile for various industrial applications. Additionally, the design incorporates features such as wear-resistant materials, to extend the lifespan of the equipment, and safety mechanisms to prevent material blockages or overpressure situations.
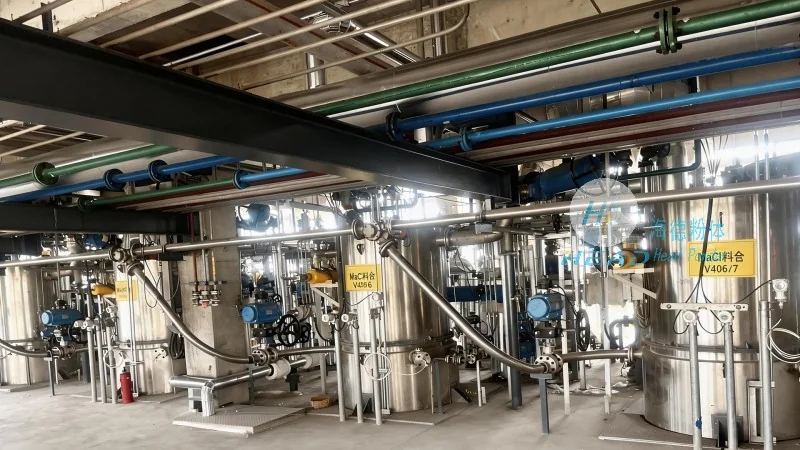
How Bin Pump Systems Operate: A Step-by-Step Explanation
The operation of a bin pump material handling system involves a series of controlled steps that ensure consistent material flow. Initially, the hopper is filled with the bulk material. The control system then activates the bin pump, which starts by compressing the diaphragm or piston, creating a vacuum inside the pump chamber. This vacuum draws the material from the hopper into the chamber. Once the chamber is filled, the control system switches the pump, causing the diaphragm or piston to expand, which forces the material out of the chamber and into the discharge line. This cycle repeats continuously, maintaining a steady flow of material to the destination. The system is designed to operate with minimal maintenance and can handle both low and high flow rates, depending on the specific application requirements.
Applications and Industries That Utilize Bin Pump Systems
Bin pump material handling systems are widely used across various industries due to their efficiency and adaptability. Common applications include the chemical industry for transporting powders and granules, the food processing industry for handling dry ingredients, the pharmaceutical industry for processing raw materials, and the mining industry for transporting bulk ores. These systems are particularly useful in applications where traditional conveyor systems may not be suitable, such as in confined spaces or when handling materials with high moisture content or abrasive properties. The versatility of bin pump systems makes them an essential part of modern industrial material handling solutions.
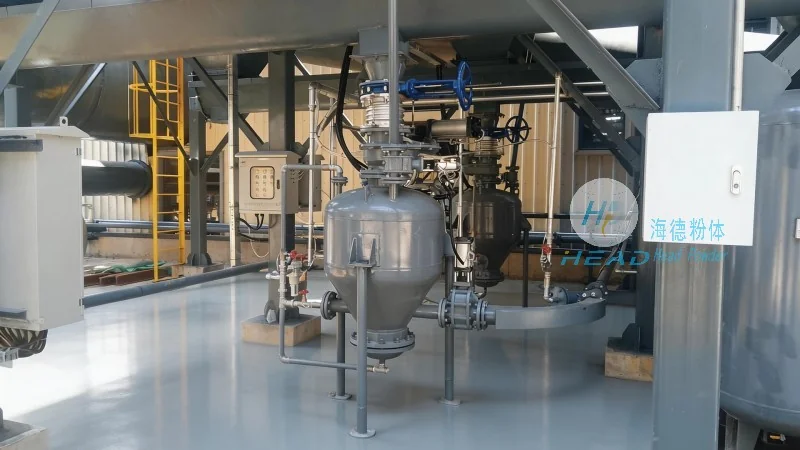
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of bin pump material handling systems. With a strong commitment to quality and innovation, HeadPowder specializes in designing and producing high-performance equipment tailored to the specific needs of industrial clients. The company's products are engineered to meet international standards and are known for their durability, efficiency, and reliability. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their material handling challenges and provide customized solutions that enhance operational efficiency and reduce downtime. The company's headquarters is located in Shandong, China, where it maintains state-of-the-art manufacturing facilities and research centers to ensure continuous improvement in product design and performance.