

Chlorinated Polyethylene Material Handling Conveyor: What It Is and Its Design Principles
Chlorinated polyethylene (CPE) material handling conveyors are specialized industrial systems engineered to transport bulk materials efficiently and safely. These conveyors are constructed using chlorinated polyethylene, a polymer known for its excellent chemical resistance, flexibility, and durability, making them ideal for handling a wide range of materials in various industrial applications. The material's molecular structure, modified by the introduction of chlorine atoms, enhances its resistance to chemicals, UV radiation, and mechanical stress, ensuring long-term performance in demanding environments. This chemical resistance is particularly valuable in industries where materials like acids, solvents, or other aggressive substances are involved, as it prevents the conveyor from degrading or corroding over time.
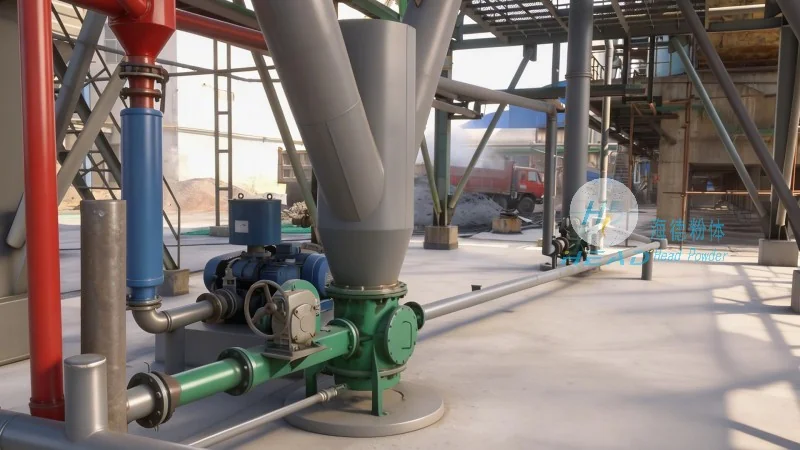
Understanding Chlorinated Polyethylene Material Handling Conveyors
At the core of these conveyors is chlorinated polyethylene, a modified polyethylene polymer where chlorine atoms are introduced into the molecular structure. This modification enhances the material's resistance to chemicals, UV radiation, and mechanical stress, ensuring long-term performance in demanding environments. The material's flexibility and low friction properties also contribute to smooth material flow and reduced wear on components. Additionally, CPE is lightweight yet strong, allowing for the construction of robust conveyor structures that can support heavy loads without excessive material deformation. These characteristics make CPE an ideal choice for material handling systems that require both durability and adaptability.
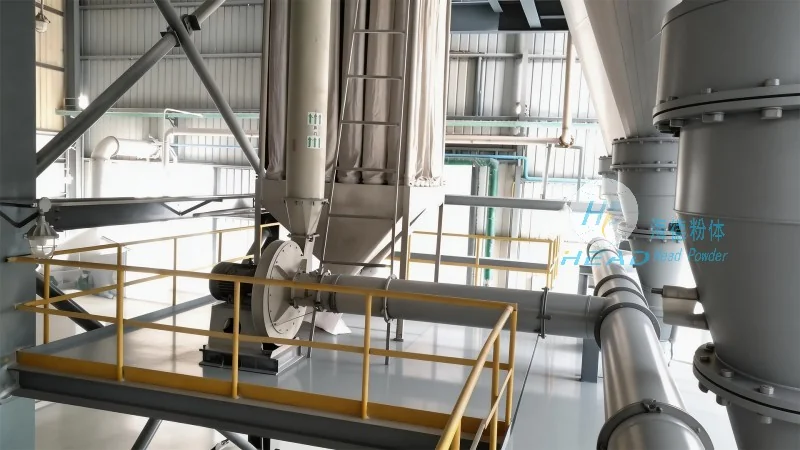
The Design Principles Behind Chlorinated Polyethylene Conveyors
The design of chlorinated polyethylene material handling conveyors follows several key principles to ensure optimal performance and reliability. First, the conveyor's structure is engineered for durability, with components made from CPE to withstand harsh conditions such as exposure to solvents, acids, or high temperatures. The material's inherent flexibility allows for the creation of smooth, continuous surfaces that minimize material buildup and reduce friction, leading to efficient material flow. Second, the system is designed for flexibility, allowing for custom configurations to accommodate different material types, such as powders, granules, or bulk solids. This adaptability is achieved through modular components, including adjustable conveyor lengths, variable incline angles, and interchangeable discharge mechanisms. Third, the conveyor incorporates efficient drive mechanisms and tensioning systems to maintain consistent material transport without excessive energy consumption. Advanced motor control systems, such as variable frequency drives (VFDs), are often integrated to optimize energy usage and reduce operational costs. Additionally, the design emphasizes safety features, including emergency stop buttons, overload protection, and protective guards, to ensure safe operation in industrial settings.
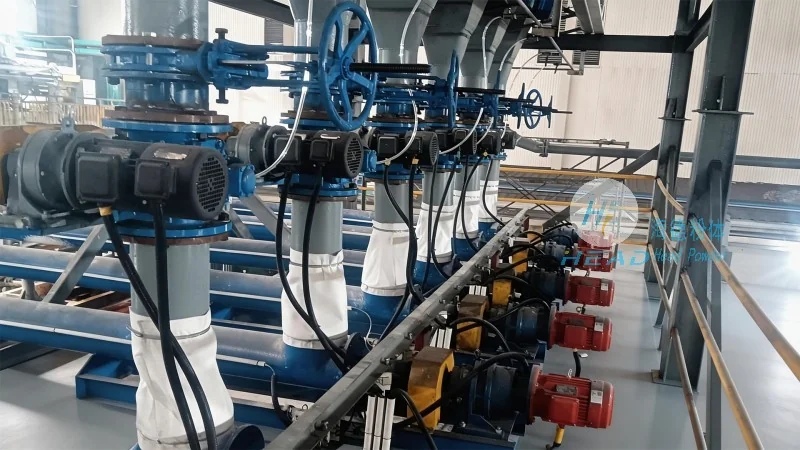
Applications and Benefits of Chlorinated Polyethylene Conveyors
Chlorinated polyethylene material handling conveyors are widely used in industries such as chemical processing, food and beverage, pharmaceuticals, and mining. Their primary benefits include high chemical resistance, which prevents corrosion or degradation when handling aggressive materials. For example, in chemical plants, these conveyors can transport corrosive powders or liquids without suffering damage, extending their service life. Additionally, the material's flexibility allows for curved or inclined designs, enabling efficient vertical or horizontal material transfer. This is particularly useful in facilities where space is limited or where materials need to be moved between different levels. The conveyors also offer low maintenance requirements due to the wear-resistant properties of CPE, reducing downtime and operational costs. Unlike metal or rubber conveyors, CPE components require minimal lubrication and are less prone to wear from abrasive materials, resulting in lower maintenance expenses over the system's lifespan.
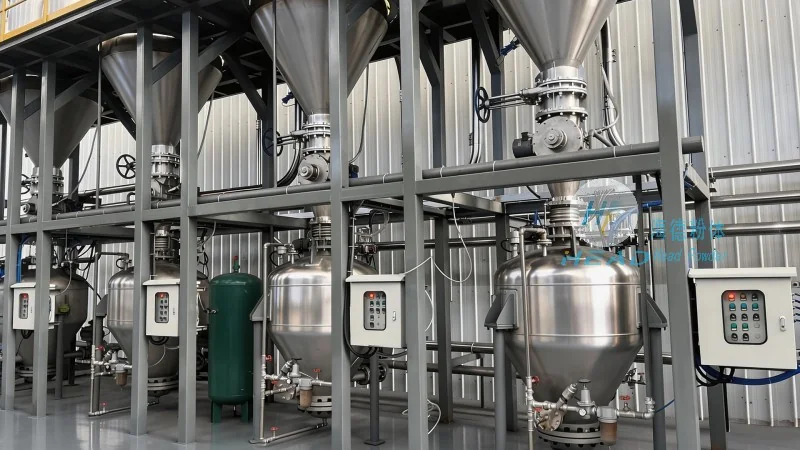
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, production, and installation of high-quality material handling systems. With a focus on innovation and customer satisfaction, the company utilizes advanced materials like chlorinated polyethylene to create durable and reliable conveyors tailored to specific industrial needs. HeadPowder's expertise in material handling technology ensures that their products meet international standards and deliver long-term performance in various applications. The company's manufacturing facilities are equipped with state-of-the-art equipment and adheres to strict quality control processes, ensuring that each conveyor is built to withstand the rigors of industrial use. HeadPowder also provides comprehensive after-sales support, including installation services, maintenance programs, and technical assistance, to ensure that clients can maximize the performance and lifespan of their material handling systems. By combining advanced materials with expert engineering, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for businesses seeking efficient and reliable material transport solutions.