

What Are Pigment Material Handling Equipment? And What Are Their Design Principles?
When it comes to industrial processes that involve the handling and transportation of pigment materials, specialized equipment plays a crucial role in ensuring efficiency, safety, and consistency. Pigment material handling equipment is designed to manage the movement of these materials from storage to processing or application stages. These systems are integral to industries such as coatings, inks, plastics, and pharmaceuticals, where the quality and uniformity of pigment distribution are paramount.
Understanding Pigment Material Handling Equipment
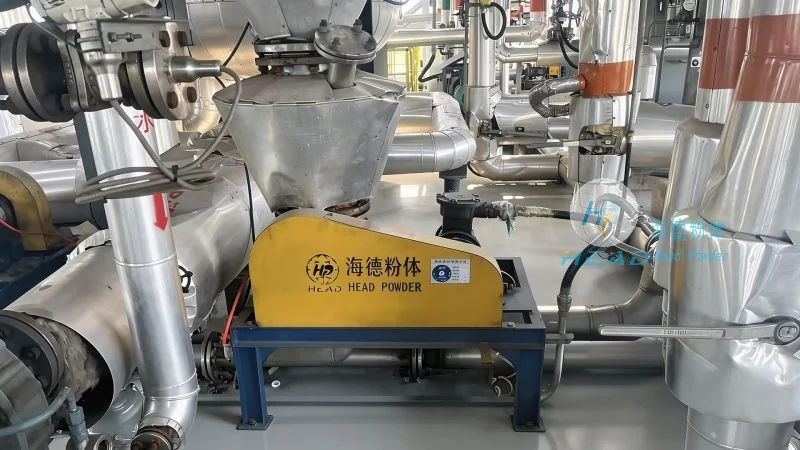
Pigment material handling equipment encompasses a range of machinery and systems engineered to transport, store, and control the flow of pigment powders or granules. The primary goal is to maintain the integrity of the pigment, prevent contamination, and ensure precise dosing for downstream processes. These systems are typically tailored to the specific characteristics of the pigment, including its particle size, density, and flow properties. By using advanced engineering principles, manufacturers like Shandong HeadPowder Engineering Co., Ltd. develop solutions that address the unique challenges of each application.
The Design Principles Behind Pigment Material Handling Equipment
The design of pigment material handling equipment is guided by several key principles to optimize performance and reliability. First, the equipment must ensure minimal product degradation during handling. This involves using materials that are compatible with the pigment, avoiding contamination, and minimizing friction or impact that could affect particle size or color. Second, the system must provide accurate and consistent flow control. This is achieved through the integration of components like feeders, conveyors, and control mechanisms that regulate the rate of material movement. Third, the design emphasizes safety and operational efficiency. Features such as dust suppression systems, enclosed structures, and automated controls help maintain a safe working environment while reducing labor costs and improving throughput.

Key Components and Their Functions
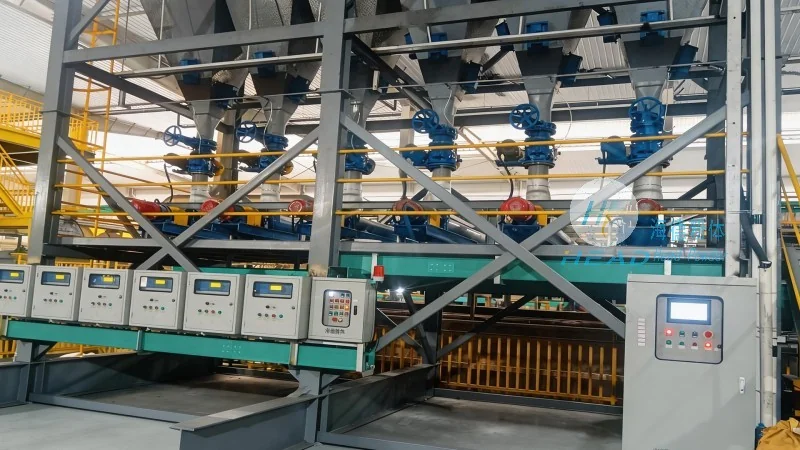
Typical pigment material handling equipment includes several key components, each serving a specific function. The storage hopper or silo is the first stage, where the pigment is stored under controlled conditions to prevent moisture absorption or agglomeration. From the hopper, a feeder, often a rotary or vibratory type, meters the material and feeds it into the conveyor system. The conveyor, which may be a screw, belt, or pneumatic system, transports the pigment to the processing or application point. Control panels and sensors are integrated to monitor flow rates, levels, and other parameters, providing real-time feedback and allowing for adjustments to maintain optimal performance.
Applications and Industries
Pigment material handling equipment is widely used across various industries. In the coatings industry, these systems ensure that pigments are evenly distributed in paint formulations, leading to consistent color and quality. In the printing industry, precise pigment delivery is critical for high-quality inks. The plastics industry relies on these systems to incorporate pigments into resin blends, while the pharmaceutical industry uses specialized equipment to handle pigments in drug formulations, ensuring compliance with regulatory standards. Each application requires tailored equipment to meet specific requirements, such as the need for sterile environments or high-purity materials.
HeadPowder's Expertise in Pigment Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pigment material handling equipment. With a focus on innovation and customer-centric solutions, HeadPowder designs and manufactures systems that meet the diverse needs of industrial clients. The company's expertise lies in understanding the unique properties of different pigments and developing equipment that ensures optimal performance. HeadPowder's products are engineered to enhance efficiency, reduce downtime, and improve product quality. By leveraging advanced technology and rigorous testing, HeadPowder delivers reliable solutions that help clients achieve their operational goals.