

What is a Multi-Hopper Pneumatic Conveyor? Exploring Its Design Principles
For industries dealing with bulk materials, the multi-hopper pneumatic conveyor stands as a versatile and efficient solution for transporting powders, granules, and other dry substances. This equipment is designed to handle a wide range of materials, from fine powders to larger granules, making it a critical asset in sectors such as pharmaceuticals, food processing, and chemical manufacturing. The system operates by using compressed air to create a pressure differential that propels material through a network of pipes, ensuring smooth and controlled movement without the need for mechanical components like belts or chains.
Understanding the Core Components and Functionality
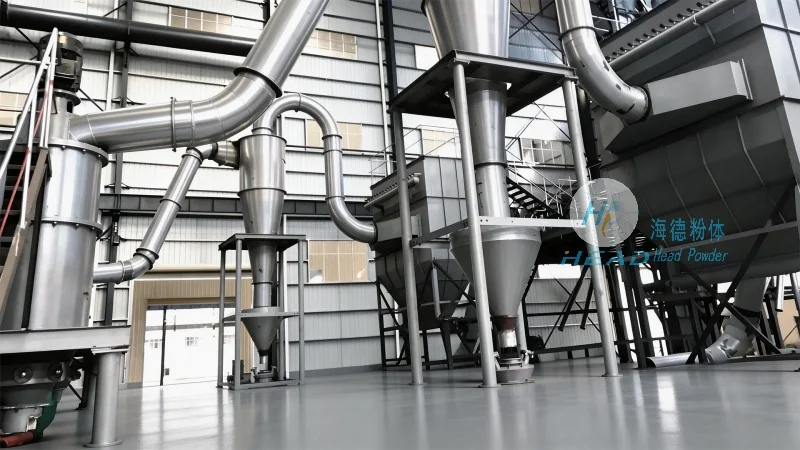
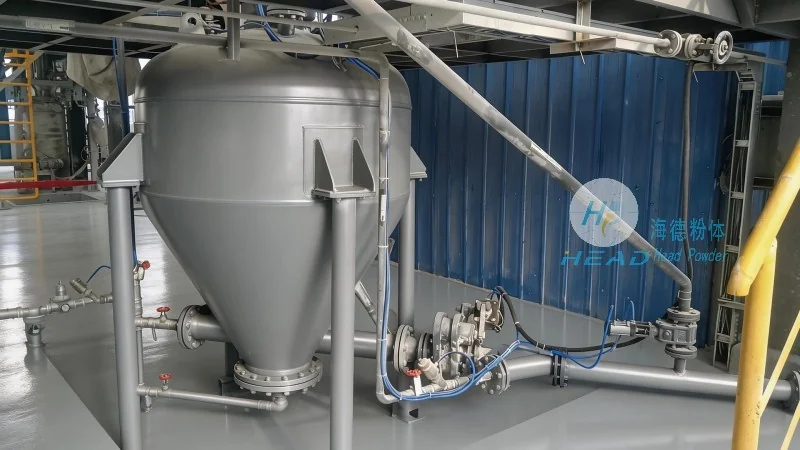
The multi-hopper system typically consists of several key components, including a hopper for material storage, a blower or compressor to generate the air flow, and a series of conveying pipes connected to the hoppers. Each hopper is equipped with a valve to control the release of material, allowing for precise dosing and batching. The design ensures that material is drawn from the hoppers and transported to the discharge point, where it can be further processed or stored. This modular approach enables flexibility in system configuration, as additional hoppers can be added to accommodate varying production needs.
Design Principles Behind Efficient Material Handling
The design principles of a multi-hopper pneumatic conveyor focus on optimizing material flow, energy efficiency, and system reliability. The use of compressed air as the primary motive force minimizes mechanical wear and reduces maintenance requirements compared to traditional conveyor systems. The pressure differential created by the blower ensures consistent material transport, even with varying material densities or particle sizes. Additionally, the system is designed to handle different material characteristics, such as moisture content or abrasive properties, by selecting appropriate hopper materials and air filtration systems. This adaptability makes the multi-hopper conveyor suitable for diverse industrial applications.
Practical Applications and Industry-Specific Benefits
Multi-hopper pneumatic conveyors are widely used in various industries due to their ability to handle different materials and process requirements. In pharmaceutical manufacturing, for example, the system can transport raw materials like powders and granules to production lines while maintaining strict hygiene standards. In food processing, the equipment ensures that ingredients are transported safely and efficiently, without cross-contamination. The system's ability to handle both small and large batches makes it ideal for batch production processes, where precise control over material flow is essential. Furthermore, the compact design of the multi-hopper conveyor allows for installation in limited spaces, making it suitable for facilities with space constraints.
Why Choose a Multi-Hopper System from Shandong HeadPowder Engineering Co., Ltd.
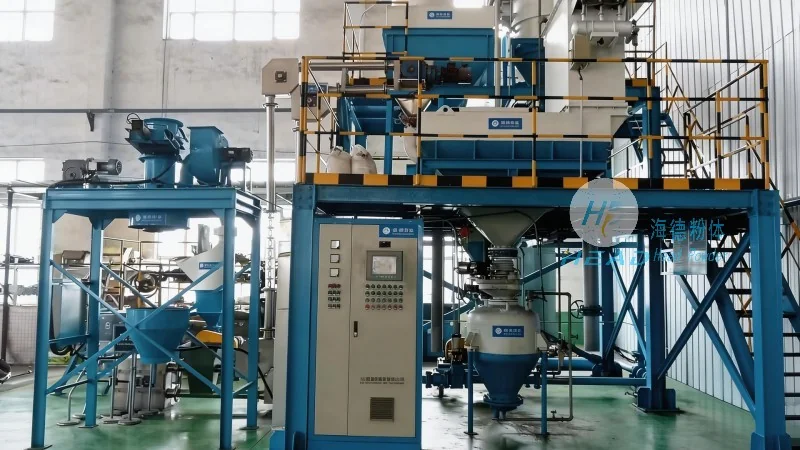
When considering a multi-hopper pneumatic conveyor, partnering with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. is crucial for ensuring quality and performance. The company specializes in designing and manufacturing custom multi-hopper systems tailored to specific industrial needs. With a focus on durability and efficiency, their products are built using high-quality materials and advanced engineering techniques. The company's commitment to customer satisfaction is evident in their comprehensive support, including system design, installation, and maintenance services. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages local expertise and resources to deliver reliable and cost-effective solutions for material handling challenges. Their experience in the industry ensures that customers receive systems that meet their exact requirements, whether for new installations or upgrades to existing facilities.