

What is an Intelligent Centralized Powder Conveying System Equipment? What are its Design Principles
For industries dealing with bulk powder handling, the efficiency and reliability of material transport systems are critical factors in operational success. Among the advanced solutions available, the intelligent centralized powder conveying system stands out as a sophisticated technology designed to streamline the movement of powders across various production stages. This article explores the essence of such equipment and delves into its underlying design principles, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. have integrated cutting-edge technology to meet the demands of modern industrial processes.
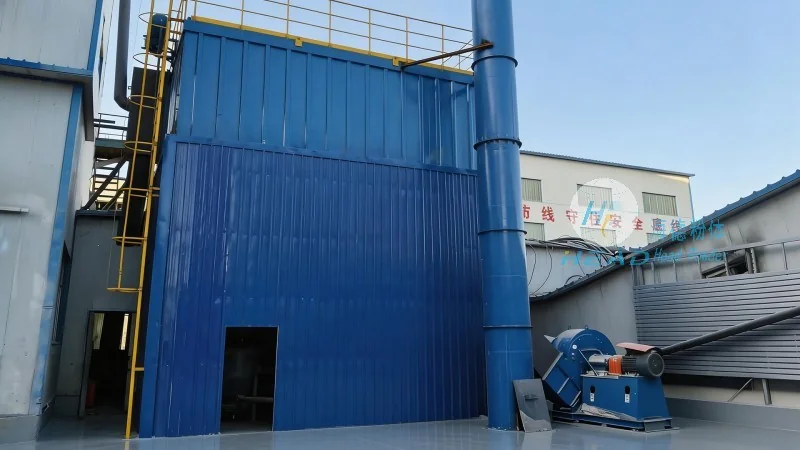
Understanding the Intelligent Centralized Powder Conveying System
The intelligent centralized powder conveying system is a comprehensive solution engineered to manage the transportation, storage, and distribution of powders within industrial settings. Unlike traditional, decentralized systems that often require multiple individual components, this centralized approach consolidates control and functionality into a single, integrated unit. The system typically comprises several key components, including a central control unit, multiple conveying lines, storage silos, and advanced sensors for real-time monitoring. Each component works in harmony to ensure seamless and efficient powder handling, reducing downtime and enhancing overall productivity.
Key Design Principles Behind the System
The design of the intelligent centralized powder conveying system is guided by several fundamental principles aimed at optimizing performance and reliability. One of the primary principles is modularity, which allows for flexibility in system configuration. This means the system can be scaled up or down based on the specific needs of the facility, accommodating varying production volumes and powder types. Another crucial principle is automation, where the system operates with minimal human intervention. Advanced control algorithms and machine learning capabilities enable the equipment to adjust parameters in real-time, responding to changes in demand or material characteristics without manual adjustments.
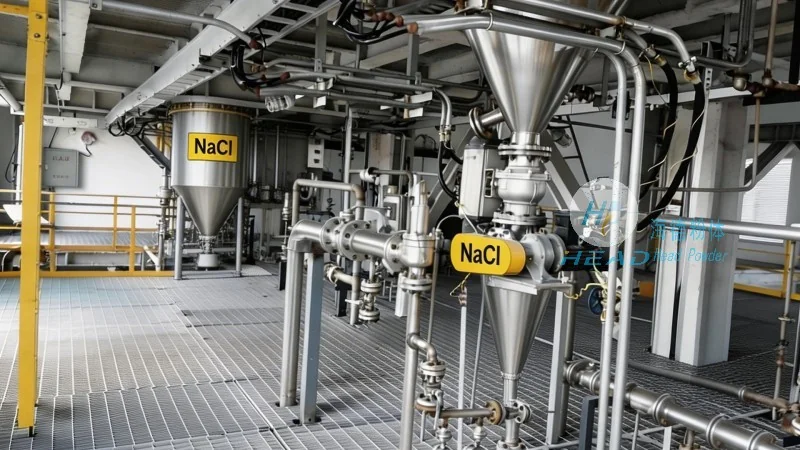
Furthermore, the system adheres to principles of energy efficiency and sustainability. By optimizing the flow of powders and reducing unnecessary movements, the equipment minimizes energy consumption. This not only lowers operational costs but also aligns with environmental regulations and corporate sustainability goals. The integration of smart sensors and data analytics is another key design principle, providing operators with actionable insights into system performance. These data-driven approaches help in predictive maintenance, allowing for proactive repairs and reducing unexpected failures.
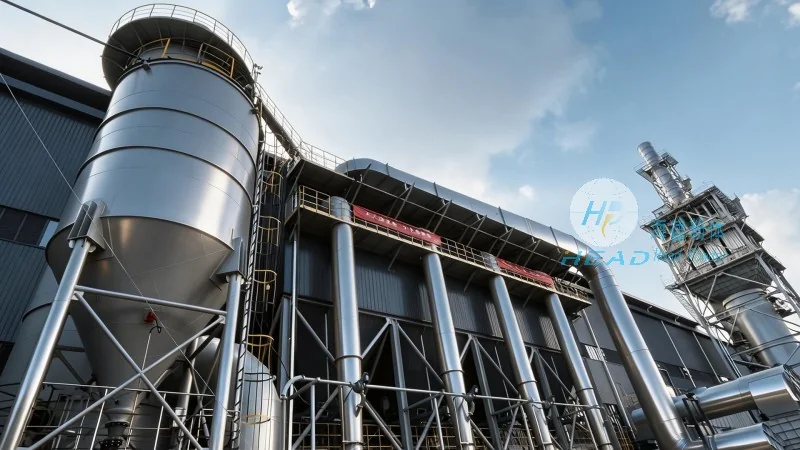
Advantages of Implementing This System
Adopting an intelligent centralized powder conveying system offers numerous benefits to industrial operations. Firstly, it significantly enhances operational efficiency by centralizing control and reducing the complexity of managing multiple conveying lines. This leads to faster response times to production changes and improved coordination between different stages of the manufacturing process. Secondly, the system improves safety by minimizing the risk of dust explosions and other hazards associated with powder handling. Advanced safety features, such as automatic shut-off mechanisms and real-time monitoring of dust levels, contribute to a safer working environment.
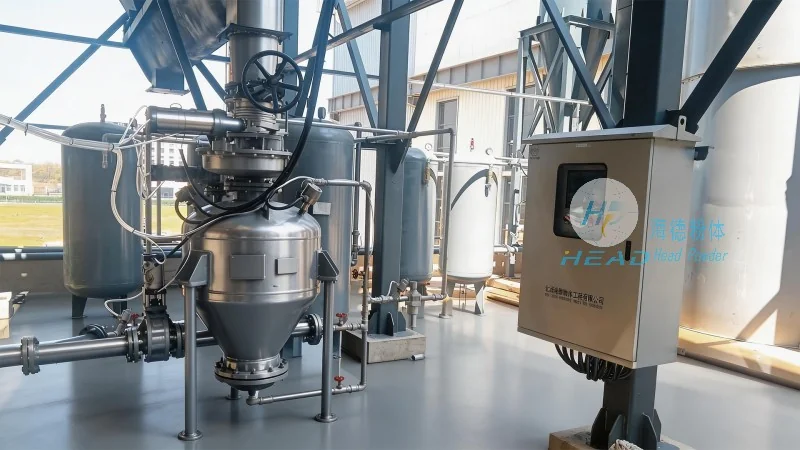
Thirdly, the system provides cost savings through reduced maintenance and operational expenses. The modular design and automated operation lower labor costs, as fewer personnel are needed to manage the system. Additionally, the energy-efficient design reduces long-term operational costs, making it a financially viable investment for industrial facilities. For companies like Shandong HeadPowder Engineering Co., Ltd., which specializes in the design and manufacturing of such systems, the intelligent centralized powder conveying system represents a benchmark in modern powder handling technology, combining innovation with practicality to meet the evolving needs of the industry.
Conclusion
In conclusion, the intelligent centralized powder conveying system is a sophisticated piece of equipment that addresses the complex challenges of bulk powder handling in modern industries. Its design, rooted in principles of modularity, automation, and sustainability, ensures high performance, reliability, and safety. By integrating advanced technology and smart controls, this system not only improves operational efficiency but also contributes to cost savings and environmental responsibility. As industries continue to seek more efficient and sustainable solutions, the intelligent centralized powder conveying system remains a critical component in the advancement of powder handling technology. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in its development and implementation, the future of bulk powder transport is undoubtedly moving towards more intelligent and centralized systems.