

What is a Rice Husk Ash Powder Conveying Equipment? And What Are Its Design Principles?
What is a Rice Husk Ash Powder Conveying Equipment? And What Are Its Design Principles?
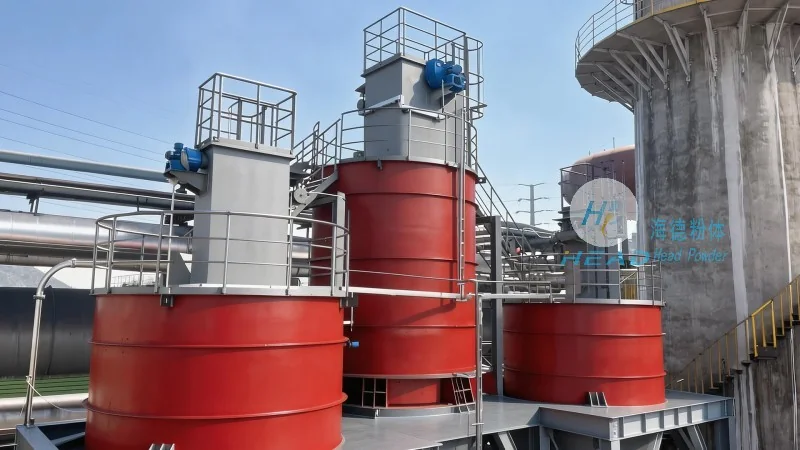
Introduction to Rice Husk Ash Powder Conveying Equipment
This equipment is specifically designed for the efficient transport of rice husk ash powder, a byproduct commonly generated in biomass energy and agricultural processing industries. The system is engineered to handle fine powders with high precision, ensuring minimal loss and optimal flow control. As a critical component in material handling, this equipment enhances productivity and operational efficiency in facilities dealing with rice husk ash.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the development and production of advanced powder conveying solutions. With years of experience in the industry, the company has established itself as a trusted provider of high-quality equipment tailored to meet the unique needs of clients in various sectors. The company's commitment to innovation and customer satisfaction drives its continuous improvement in product design and performance.
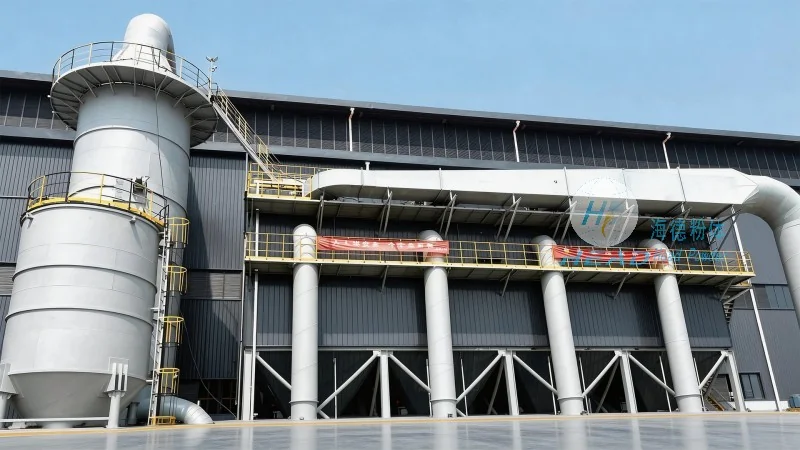
Understanding the Core Function of the Equipment
The primary function of the rice husk ash powder conveying equipment is to move bulk powders from one location to another within industrial settings. This process involves the use of specialized mechanisms such as pneumatic or mechanical systems that ensure the material is transported safely and efficiently. The equipment is designed to handle the unique properties of rice husk ash, including its fine particle size and potential for dust generation, by incorporating features that maintain air quality and prevent material degradation.
Design Principles Behind the Powder Conveying System
The design of the powder conveying system follows several key principles to ensure optimal performance. These include maintaining consistent air pressure and flow rates to achieve smooth material transport, using appropriate materials for components that come into contact with the powder to prevent contamination, and integrating safety features to protect operators and the environment. The system is also engineered for easy maintenance and scalability, allowing it to adapt to changing production demands.
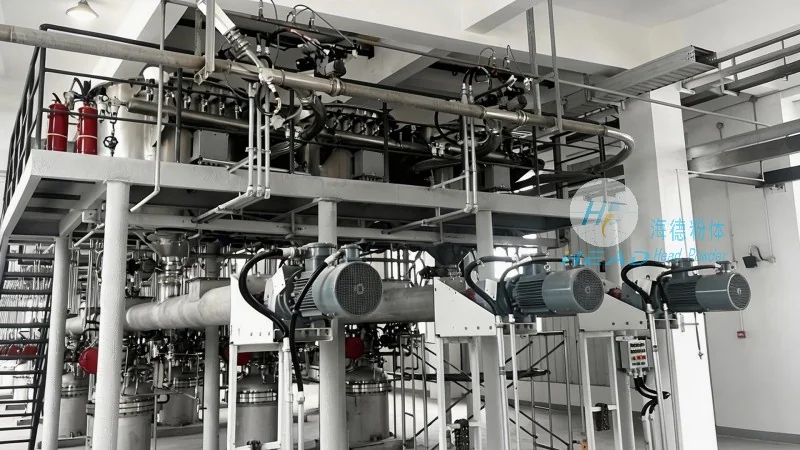
Key Components and Their Roles in Efficient Transport
Several key components work together to ensure the efficient operation of the powder conveying equipment. These include the hopper, which serves as the storage and feeding unit; the conveyor line, which transports the powder through the system; and the control system, which monitors and adjusts the flow rate. Additionally, filters and dust collection systems are integrated to manage air quality and comply with environmental regulations. Each component is carefully selected and designed to work in harmony, ensuring the overall system operates at peak efficiency.

Application Scenarios and Practical Benefits
The rice husk ash powder conveying equipment is widely used in various industrial applications, including biomass power plants, agricultural processing facilities, and material recycling operations. Its practical benefits include reduced labor costs, improved safety by minimizing manual handling, and enhanced product quality through consistent material flow. The equipment also contributes to environmental sustainability by ensuring the efficient use of rice husk ash, a renewable resource, in industrial processes.
Conclusion and Company Contact Information
In conclusion, the rice husk ash powder conveying equipment is a vital tool for industries dealing with fine powders, offering efficient and reliable transport solutions. HeadPowder, with its expertise and commitment to quality, provides cutting-edge equipment that meets the demands of modern industrial operations. For more information or inquiries, please contact Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China.