

What Are Gray Bin Material Handling Equipment? And What Are Their Design Principles?
Gray bin material handling equipment is a specialized type of machinery designed to transport bulk materials within industrial and processing facilities. These systems are commonly used in industries such as cement production, mining, and chemical processing, where large volumes of powders or granules need to be moved efficiently and safely. The equipment typically operates by feeding materials from a storage bin or hopper into a conveyor system, which then transports the material to the desired location. This process is crucial for maintaining smooth production workflows and ensuring that materials are handled with minimal dust generation and contamination.
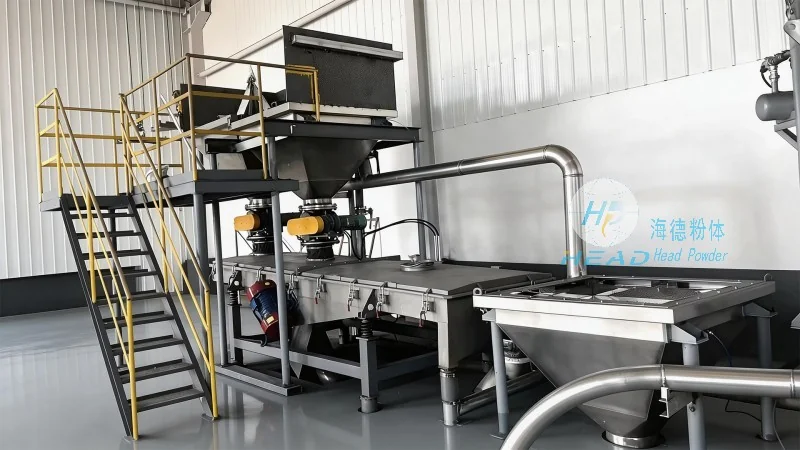
Understanding the Core Components of Gray Bin Material Handling Equipment
The design of gray bin material handling equipment involves several key components that work together to ensure reliable operation. The primary components include the storage bin or hopper, which holds the bulk material; a feeding mechanism, such as a rotary valve or screw feeder, that controls the flow of material from the bin; a conveyor system, which may consist of a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the material characteristics and application requirements; and a control system that monitors and regulates the entire process. Each component is engineered to handle the specific properties of the material being transported, such as its density, moisture content, and flowability. For example, in cement plants, the equipment must be able to handle high-density materials like clinker and limestone without clogging or damaging the system. The feeding mechanism is often designed with anti-stick features to prevent material buildup, while the conveyor system may use special materials or coatings to prevent abrasion from the abrasive nature of the material.
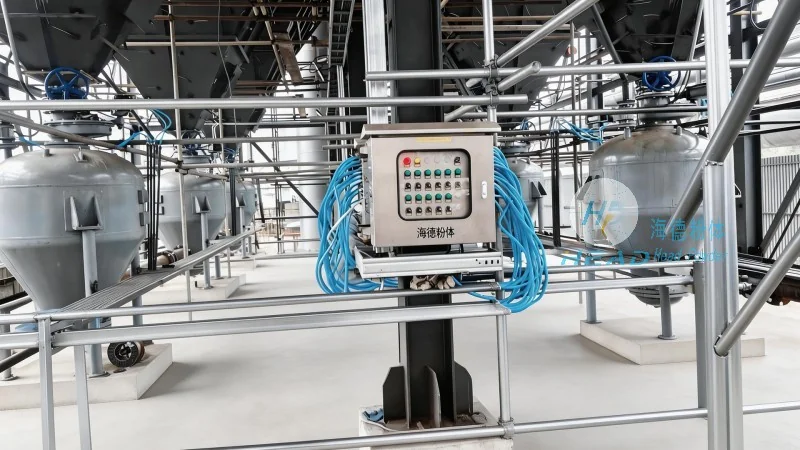
The Design Principles Behind Gray Bin Material Handling Equipment
The design principles of gray bin material handling equipment are centered on efficiency, reliability, and safety. Efficiency is achieved through the use of optimized conveyor systems that minimize energy consumption while maximizing material throughput. The control system plays a critical role in this, as it can adjust the speed of the conveyor or the rate of material feeding based on real-time production demands. Reliability is ensured by incorporating durable materials and robust construction, as the equipment is often exposed to harsh operating conditions, including high temperatures, dust, and vibrations. Safety features are also integral, with designs that prevent accidental release of material and reduce the risk of dust explosions. For instance, many systems include explosion-proof components and dust collection systems to maintain a safe working environment. The design also considers the need for easy maintenance and cleaning, as regular upkeep is essential to prevent system downtime and maintain performance. This includes features like removable parts and easy access to the conveyor components for inspection and cleaning.
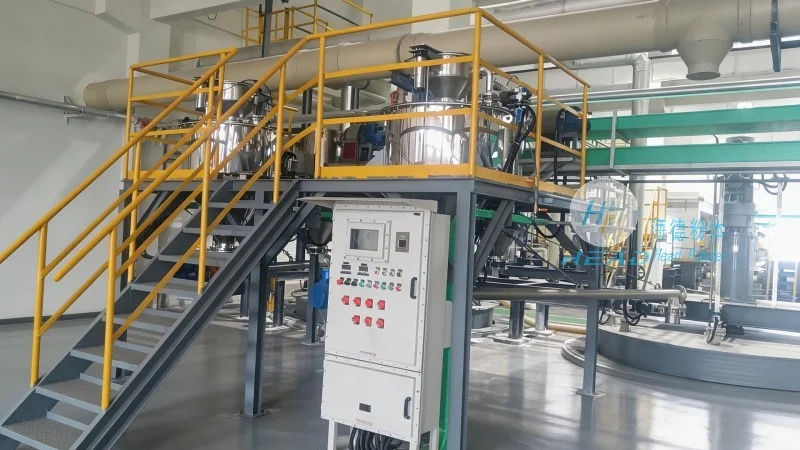
Applications and Industries That Utilize Gray Bin Material Handling Equipment
Gray bin material handling equipment is widely used across various industries due to its versatility and ability to handle a wide range of bulk materials. In the cement industry, it is used to transport raw materials like limestone and clay from storage bins to the kiln, as well as to move finished cement products from the grinding mill to storage silos. In mining operations, the equipment is used to transport ore from the mine to processing facilities, where it is crushed and processed. The chemical industry also relies on these systems to transport powders and granules used in the production of chemicals, pharmaceuticals, and fertilizers. The equipment is also used in food processing facilities to handle ingredients like flour, sugar, and grains, where hygiene and contamination control are critical. In all these applications, the equipment is designed to meet the specific requirements of the industry, including regulatory standards for material handling and safety.
Advantages of Using Gray Bin Material Handling Equipment
There are several advantages to using gray bin material handling equipment in industrial settings. One of the primary advantages is the ability to handle large volumes of bulk materials efficiently, which reduces labor costs and increases production throughput. The equipment also helps to minimize material waste by reducing spillage and loss during transportation. Additionally, the systems are designed to be energy-efficient, which can lead to lower operating costs over time. The use of automated control systems also improves operational consistency and reduces the risk of human error. Another advantage is the ability to handle a wide range of materials, from fine powders to coarse granules, without the need for multiple pieces of equipment. This versatility makes the equipment a cost-effective solution for many industrial applications. Furthermore, the equipment is designed to be durable and long-lasting, with a service life that can extend for many years with proper maintenance. This reduces the need for frequent replacements and lowers the total cost of ownership.
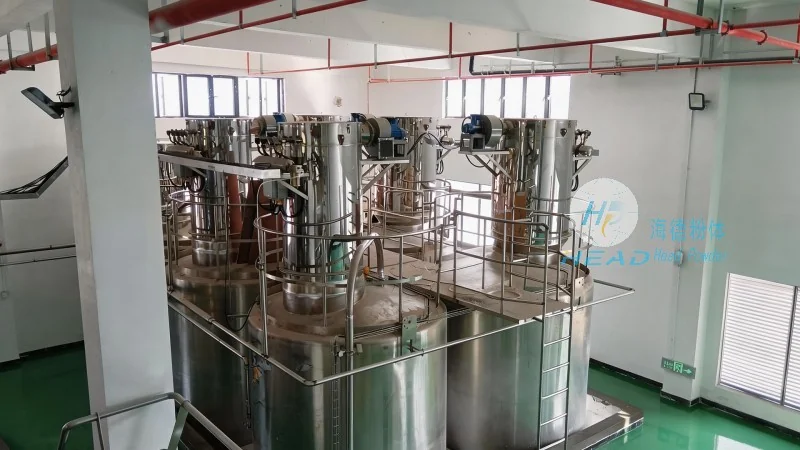
Conclusion and Company Overview
Gray bin material handling equipment is a critical component of modern industrial operations, providing efficient and reliable transportation of bulk materials. The design principles behind these systems focus on optimizing performance, ensuring safety, and maintaining durability. The equipment is used across a wide range of industries, including cement, mining, and chemical processing, where it plays a vital role in maintaining smooth production workflows. The advantages of using such equipment include increased efficiency, reduced waste, and lower operating costs. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality gray bin material handling equipment tailored to the specific needs of various industries. With a focus on quality and innovation, the company provides solutions that enhance productivity and safety in industrial settings. Located in Shandong, China, HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for businesses seeking reliable material handling solutions.