

What is a Coal Fly Ash Powder Conveying Machine? And What Are Its Design Principles?
Coal fly ash, a byproduct of coal combustion in thermal power plants, is a fine powder that requires efficient and reliable transportation systems for handling and utilization. The coal fly ash powder conveying machine, also known as a pneumatic or mechanical conveyor system, is specifically designed to handle this fine particulate material with precision and efficiency. This equipment plays a crucial role in the industrial processes of power generation, construction, and environmental management, ensuring that coal fly ash is transported safely and effectively from its source to processing or disposal sites.
Key Design Principles of Coal Fly Ash Powder Conveying Machines
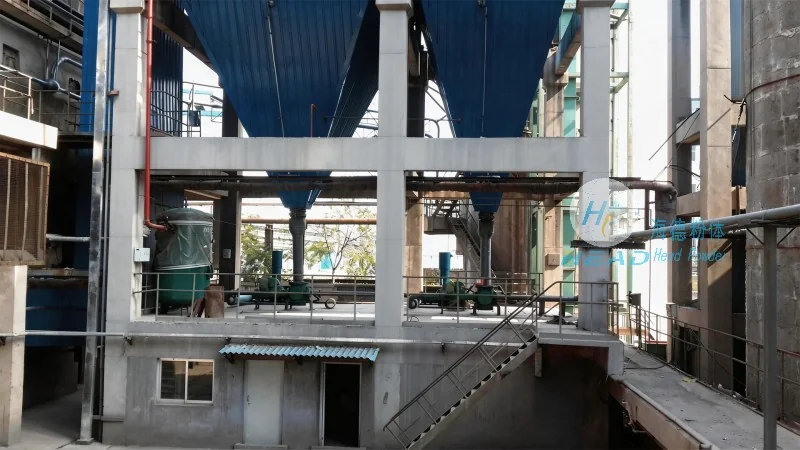
The design of a coal fly ash powder conveying machine is built upon several fundamental principles to address the unique challenges posed by this material. First, the machine must be capable of handling the high dust content and fine particle size of coal fly ash, which can cause clogging and wear if not properly managed. Engineers incorporate features such as robust hopper designs, anti-clogging valves, and specialized material handling components to prevent blockages and ensure consistent flow. Second, the system is engineered for durability and low maintenance, as coal fly ash can be abrasive and corrosive to metal surfaces. Materials like stainless steel, wear-resistant coatings, and high-quality seals are commonly used to extend the lifespan of the equipment. Third, the conveying system is designed to minimize air leakage and maintain consistent pressure, which is critical for maintaining the flow of fine powders. This is achieved through airtight connections, proper sealing mechanisms, and efficient air distribution components. Additionally, the design considers the need for easy cleaning and maintenance, with features like removable hopper sections and accessible internal components that allow for quick inspections and repairs.
How Coal Fly Ash Powder Conveying Machines Work
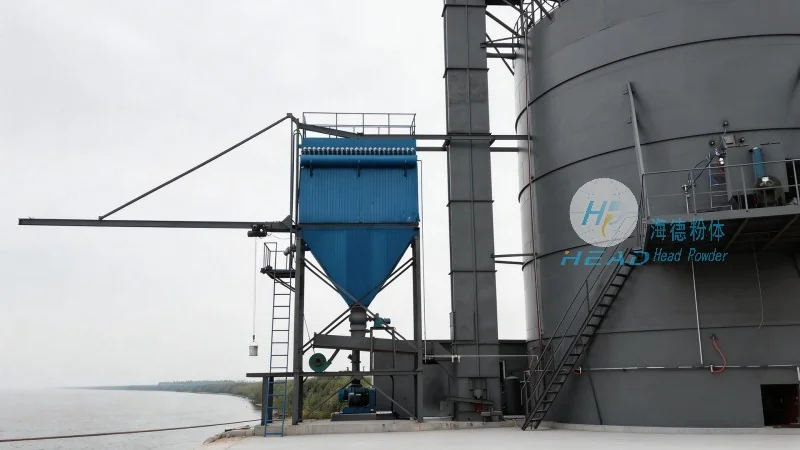
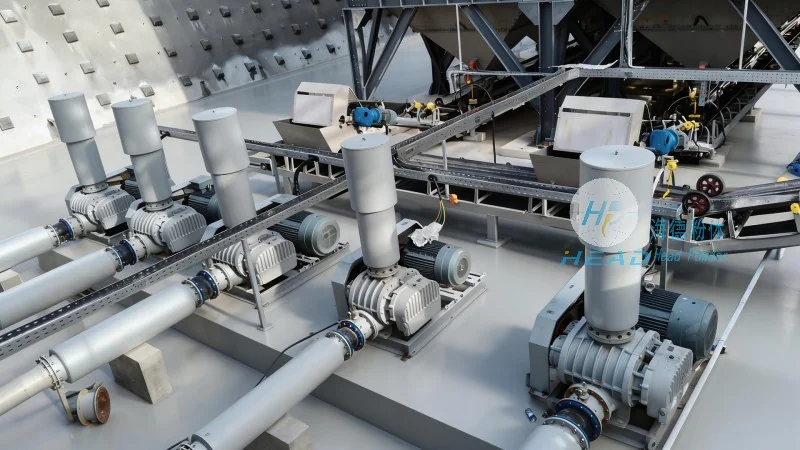
The operation of a coal fly ash powder conveying machine typically involves a combination of pneumatic and mechanical components, depending on the specific application and material characteristics. The most common type is the positive displacement blower or rotary lobe pump, which generates the necessary pressure to move the powder through the system. The process begins with the coal fly ash being fed into a hopper, where it is stored and prepared for transport. From the hopper, the material is drawn into the conveying line by the air pressure generated by the blower. The air and powder mixture travels through a series of pipes or ducts, with the powder suspended in the air stream. As the mixture moves through the system, it may pass through expansion chambers or cyclone separators to separate any larger particles or moisture, ensuring a consistent and clean flow. The final stage involves the discharge of the coal fly ash at the destination point, where it can be further processed or stored. The entire system is controlled by a programmable logic controller (PLC) or other automation systems, which monitor pressure, flow rates, and other parameters to optimize performance and prevent issues such as overloading or clogging.
Applications and Benefits of Coal Fly Ash Powder Conveying Machines
Coal fly ash powder conveying machines are widely used in various industrial applications due to their versatility and efficiency. In the power generation industry, these machines are essential for transporting coal fly ash from the boiler to storage silos or disposal sites, ensuring that the material is handled safely and in compliance with environmental regulations. In the construction industry, coal fly ash is often used as a supplementary cementitious material in concrete production, and the conveying machines facilitate the transport of this material from storage to mixing plants. Additionally, the equipment is used in environmental management applications, such as the treatment of ash from waste incineration facilities, where it is necessary to transport the fine powder to recycling or disposal sites. The benefits of using a coal fly ash powder conveying machine include improved safety by reducing manual handling of the material, increased efficiency by minimizing downtime and maintenance, and cost savings through reduced labor and equipment wear. The system also helps to maintain a clean and dust-free environment by containing the powder within the conveying line, preventing airborne particles from contaminating the workplace or surrounding areas.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial powder handling equipment, including coal fly ash powder conveying machines. With headquarters in Shandong, China, the company has established itself as a trusted partner for businesses in the power, construction, and environmental sectors. HeadPowder specializes in designing and manufacturing high-quality, reliable equipment that meets the specific needs of its clients. The company's team of engineers and technicians has extensive experience in powder handling technology, ensuring that each product is engineered to deliver optimal performance and durability. HeadPowder's commitment to quality and customer satisfaction is reflected in its rigorous testing processes, comprehensive after-sales support, and adherence to international standards. By leveraging advanced manufacturing techniques and continuous innovation, HeadPowder provides solutions that help its clients improve operational efficiency, reduce costs, and enhance safety in their powder handling processes. The company's products are widely recognized for their reliability, efficiency, and adaptability, making them a preferred choice for industries that require consistent and effective transportation of fine powders like coal fly ash.