

What is Potassium Carbonate Fertilizer Powder Conveying? And What Are Its Design Principles?
As a critical component in modern agricultural practices, potassium carbonate fertilizer plays a vital role in enhancing crop yields and improving soil health. The efficient handling and transportation of this fine powder are essential for optimizing the supply chain and ensuring consistent product quality. This article explores the concept of potassium carbonate fertilizer powder conveying and delves into the underlying design principles that enable effective material transport.
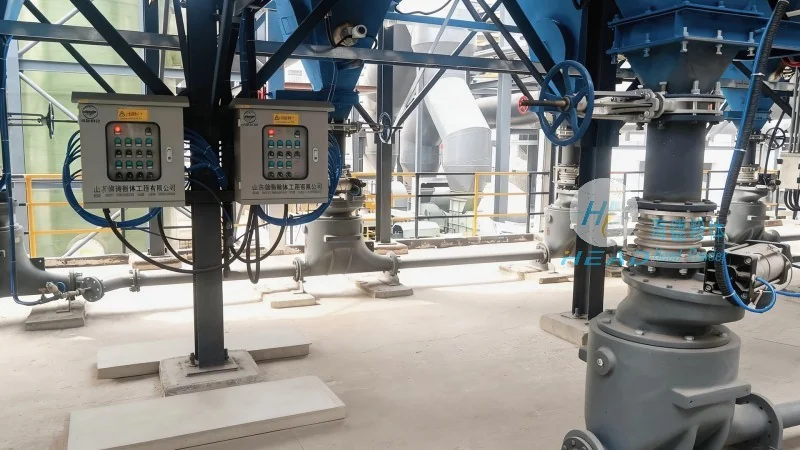
Key Aspects of Potassium Carbonate Fertilizer Powder Conveying
Potassium carbonate fertilizer, also known as potash, is a white crystalline powder widely used in agriculture due to its high potassium content. Conveying this material requires specialized equipment and systems to prevent caking, segregation, and loss of product integrity. The process involves the movement of the fine powder from storage silos or production lines to processing facilities, storage areas, or application sites. Effective powder conveying systems must address challenges such as particle size variability, moisture sensitivity, and the need for gentle handling to maintain product quality.
Design Principles for Efficient Powder Conveying Systems
The design of a potassium carbonate fertilizer powder conveying system is based on several fundamental principles aimed at maximizing efficiency, minimizing product degradation, and ensuring safe operation. These principles include:
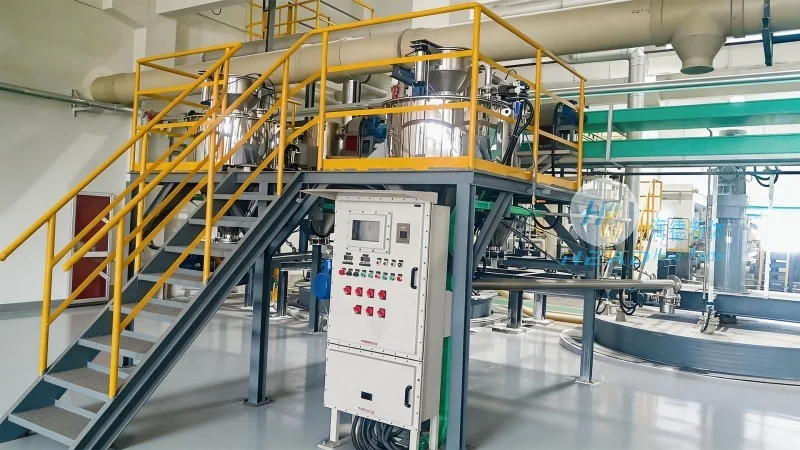
- Material Compatibility: The equipment and components used in the conveying system must be compatible with potassium carbonate fertilizer. This includes selecting materials that resist corrosion, such as stainless steel or specialized coatings, to prevent contamination and maintain product purity.
- Gentle Handling: Since potassium carbonate is a fine powder, the conveying system must employ low-shear mechanisms to avoid particle breakage or agglomeration. This is crucial for preserving the granular structure and ensuring consistent nutrient content in the final product.
- Airflow Management: Air is often used as a medium for pneumatic conveying, which involves transporting the powder through a pipeline using compressed air. Proper airflow management is essential to maintain consistent flow rates and prevent blockages or pressure drops that could lead to system inefficiencies.
- Control and Automation: Modern powder conveying systems incorporate advanced control systems and automation to monitor flow rates, pressure, and other critical parameters. This allows for real-time adjustments and ensures optimal performance under varying operating conditions.
Components of a Typical Powder Conveying System
A standard potassium carbonate fertilizer powder conveying system typically consists of several key components, each playing a specific role in the material transport process:
- Feed Hopper: The feed hopper is responsible for storing and feeding the potassium carbonate powder into the conveying system. It is designed to maintain a consistent material level and prevent overfilling or underfilling, which could affect flow rates.
- Pneumatic Conveying Line: The main component of the system, the pneumatic conveying line transports the powder using compressed air. This line is usually made of stainless steel or other corrosion-resistant materials to withstand the chemical properties of the fertilizer.
- Control Valves and Regulators: These components regulate the flow of air and powder through the system, ensuring smooth and controlled operation. They help maintain consistent pressure and flow rates, preventing issues such as clogging or excessive pressure buildup.
- Receiver Tank: The receiver tank collects the conveyed powder at the destination point. It is equipped with a discharge valve and may include a dust collection system to prevent environmental contamination and maintain workplace safety.
- Dust Collection System: To comply with environmental regulations and ensure workplace safety, a dust collection system is often integrated into the conveying line. This system captures any airborne particles and filters them before releasing clean air back into the environment.
HeadPowder: Expert in Potassium Carbonate Fertilizer Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing advanced powder conveying solutions for the agricultural industry. With years of experience in the field, HeadPowder has developed innovative systems tailored to the unique challenges of handling potassium carbonate fertilizer. The company's expertise lies in designing and manufacturing equipment that meets the highest standards of efficiency, reliability, and safety.
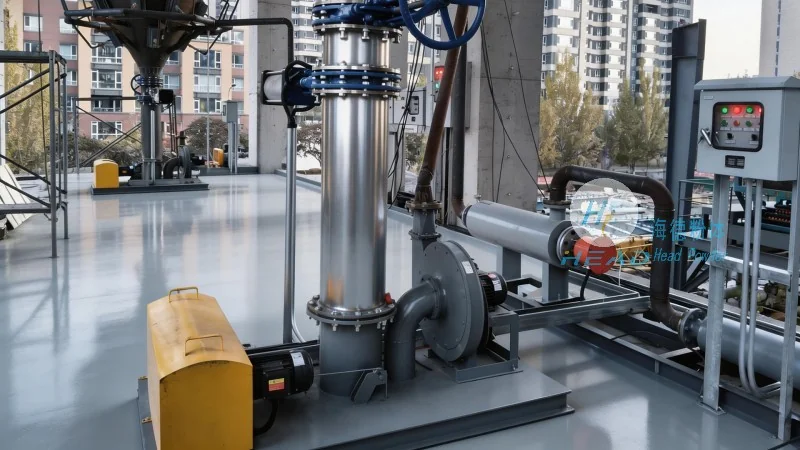
HeadPowder's team of engineers and technicians works closely with clients to understand their specific requirements and develop customized powder conveying systems. Whether for small-scale agricultural operations or large industrial facilities, HeadPowder offers solutions that optimize material transport while minimizing downtime and maintenance costs. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking reliable fertilizer handling solutions.
Located in Shandong, China, HeadPowder leverages its local expertise and manufacturing capabilities to deliver high-quality products and services to clients worldwide. By combining advanced technology with practical engineering, HeadPowder ensures that its powder conveying systems are not only efficient but also durable and cost-effective. The company's focus on innovation and customer needs has enabled it to stay at the forefront of the industry, providing solutions that meet the evolving demands of modern agriculture.