

What is Mobile Powder Handling? And Its Design Principles
Mobile powder handling systems represent a specialized category of industrial equipment designed to transport bulk powders from one location to another using vehicles equipped with integrated conveying mechanisms. These systems are essential in various industries, including food processing, pharmaceuticals, and chemical manufacturing, where the efficient and safe movement of powders is critical to operational efficiency and product quality.
Understanding Mobile Powder Handling Systems
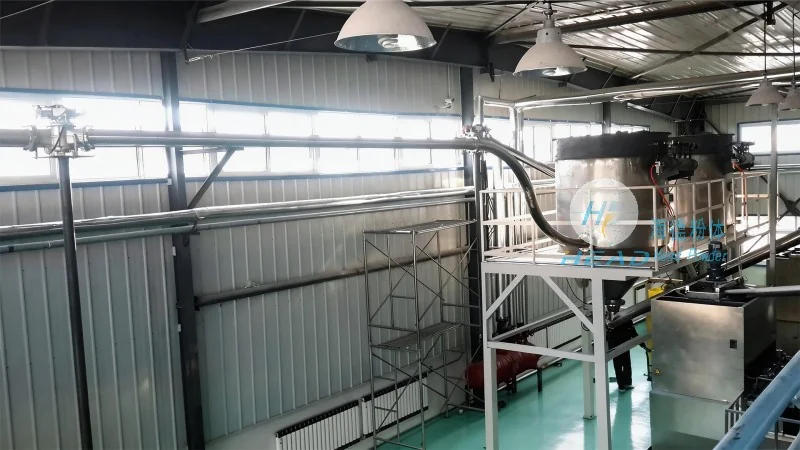
At its core, a mobile powder handling system combines the mobility of a vehicle with the functionality of a powder conveying system. Unlike stationary systems, these units are designed to be transported to different work sites, providing flexibility in operations. The primary components typically include a hopper for material storage, a conveyor system (such as a screw or pneumatic conveyor) for transporting the powder, and a control panel for operation. The vehicle itself may be a truck, trailer, or specialized transport unit, depending on the application and the volume of material being handled.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of mobile powder handling solutions. With a focus on innovation and customer-centric design, the company has established itself as a trusted partner in the industry. HeadPowder's products are engineered to meet the specific needs of various applications, ensuring reliability, efficiency, and safety in powder transport operations. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center.
Key Design Principles of Mobile Powder Handling Systems
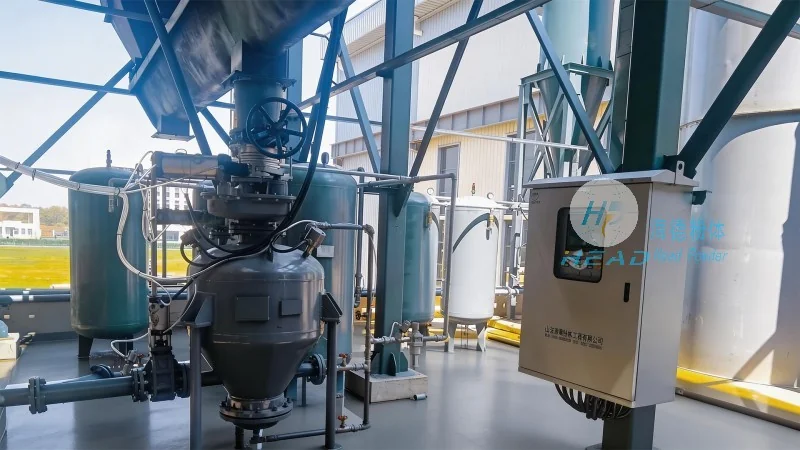
The design of mobile powder handling systems involves several critical principles aimed at optimizing performance, safety, and durability. One of the primary considerations is the selection of appropriate materials for the hopper and conveyor components. These parts must be resistant to corrosion, abrasion, and the specific properties of the powder being handled, such as moisture content or chemical reactivity. For example, stainless steel is commonly used for food-grade applications, while specialized alloys may be employed for handling aggressive chemicals.
Another crucial design principle is the integration of the conveying mechanism with the vehicle's structure. The system must be securely mounted to ensure stability during transport and operation. This includes considerations for load distribution, vibration control, and the ability to withstand the stresses of moving over different terrains. The control system is also a key design element, as it must provide precise control over the flow rate, pressure, and direction of the powder, while also incorporating safety features like overload protection and emergency stop mechanisms.
Applications and Operational Benefits
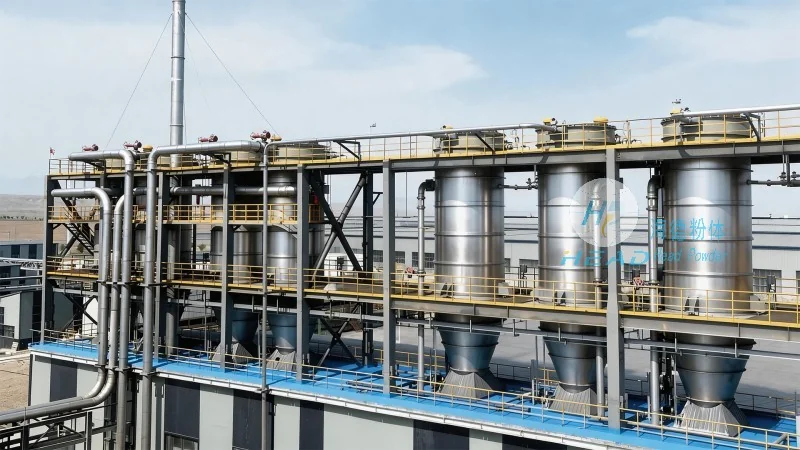
Mobile powder handling systems are widely used in industries where the need to move powders between different processing stages or locations is frequent. In food processing, for instance, these systems can transport ingredients such as flour, sugar, or spices from storage to production lines. In pharmaceutical manufacturing, they are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the powder is moved in a controlled and sterile environment. The benefits of using mobile systems include increased operational flexibility, reduced downtime for material transport, and improved safety by minimizing manual handling of powders.
Conclusion
Mobile powder handling systems are a vital component of modern industrial operations, offering a flexible and efficient solution for transporting bulk powders. The design principles behind these systems, including material selection, structural integration, and advanced control systems, are critical to their performance and reliability. Companies like Shandong HeadPowder Engineering Co., Ltd. play a key role in developing and supplying these systems, helping businesses in various industries to enhance their operational capabilities and maintain high standards of product quality and safety.