

What is a Coffee Pneumatic Conveying System Device? What are its Design Principles?
Coffee processing facilities often rely on specialized equipment to handle the transportation of coffee beans efficiently and safely. Among these, the coffee pneumatic conveying system device stands out as a critical component for managing the flow of raw coffee beans from storage to processing stages. This system utilizes air pressure to move materials, offering a non-contact, hygienic method that is particularly valuable in the food industry, where maintaining product integrity and preventing contamination is paramount.
Understanding the Coffee Pneumatic Conveying System
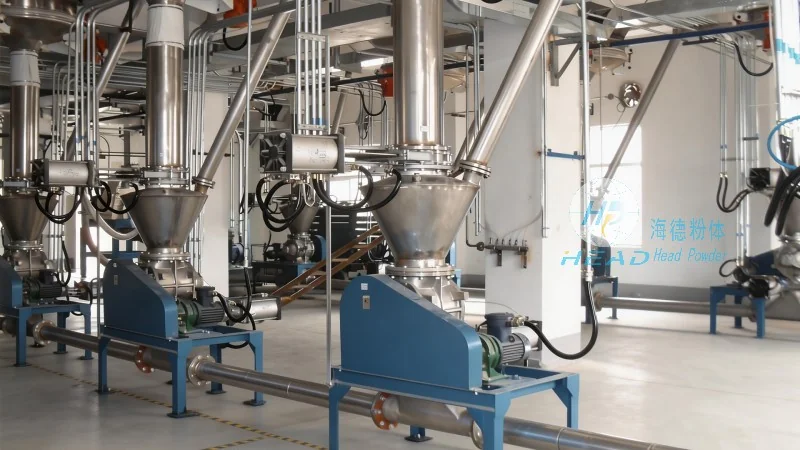
The coffee pneumatic conveying system device is designed to transport coffee beans through a network of pipes using compressed air. This technology eliminates the need for mechanical components like belts or chains, reducing wear and tear and minimizing the risk of product damage. The system typically includes a hopper for material storage, a blower or air compressor to generate the necessary airflow, and a series of pipes that guide the beans to the processing unit. At the receiving end, a separator or cyclone separates the coffee beans from the air stream, allowing for clean and efficient collection.
Key Design Principles of the Coffee Pneumatic Conveying System
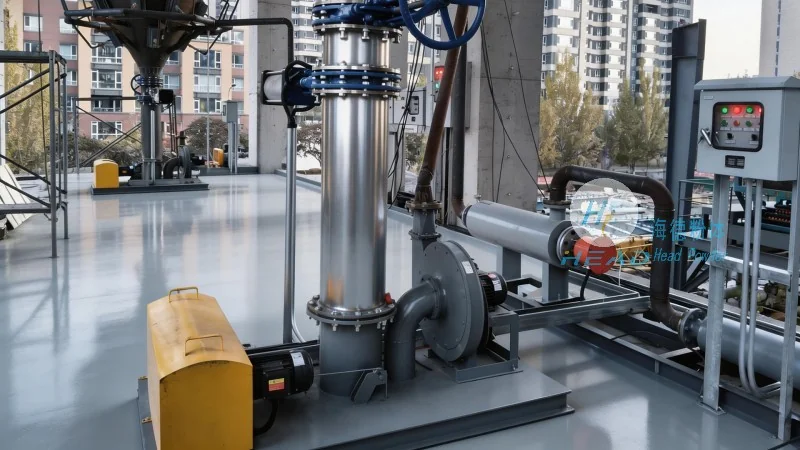
The design of a coffee pneumatic conveying system device is governed by several fundamental principles to ensure optimal performance and reliability. First, the system must maintain a consistent air pressure and flow rate to prevent blockages or uneven material transport. This is achieved through the use of appropriately sized pipes and blower systems that match the volume of coffee beans being handled. Second, the system incorporates features to minimize particle separation and ensure that the coffee beans remain intact during transport. This includes the use of smooth, non-abrasive pipe interiors and gentle bends that reduce friction and impact. Third, the design prioritizes hygiene and ease of cleaning, which is essential in food processing environments. Components such as the hopper and separator are often made from stainless steel and designed with smooth surfaces to facilitate thorough sanitation.
Role of Shandong HeadPowder Engineering Co., Ltd. in Coffee Processing Equipment
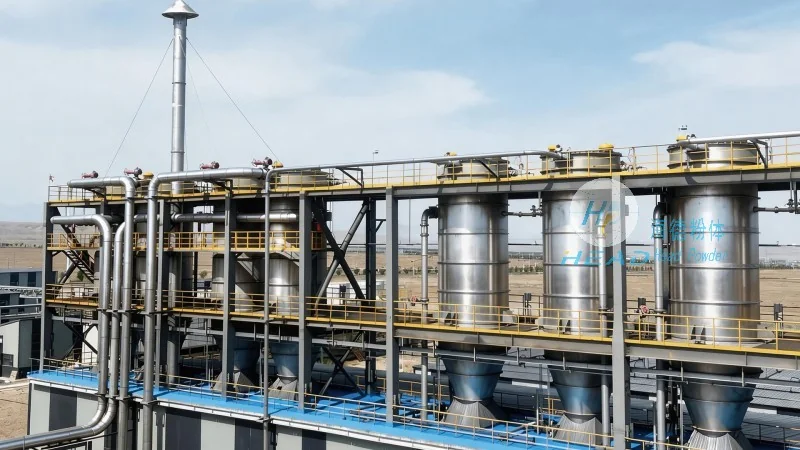
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in engineering solutions for the food and powder processing industries. With operations based in Shandong, China, the company has extensive experience in designing and manufacturing pneumatic conveying systems tailored to the unique needs of coffee processing facilities. HeadPowder’s expertise lies in integrating advanced design principles with practical application, ensuring that their coffee pneumatic conveying system devices are both efficient and durable. The company’s commitment to quality and customer satisfaction is reflected in their adherence to industry standards and continuous innovation in equipment technology.
Benefits of Using a Coffee Pneumatic Conveying System
Implementing a coffee pneumatic conveying system device in a coffee processing plant offers numerous advantages. Primarily, it enhances operational efficiency by reducing the time and labor required for material handling. The system’s ability to transport coffee beans over long distances without the need for manual intervention streamlines production processes. Additionally, the hygienic nature of pneumatic conveying minimizes the risk of contamination, which is critical for maintaining product quality and meeting regulatory standards. The system also reduces energy consumption compared to traditional mechanical conveying methods, contributing to cost savings and environmental sustainability. Furthermore, the non-contact design prevents the introduction of foreign particles or contaminants into the coffee beans, preserving their flavor and aroma.
Conclusion
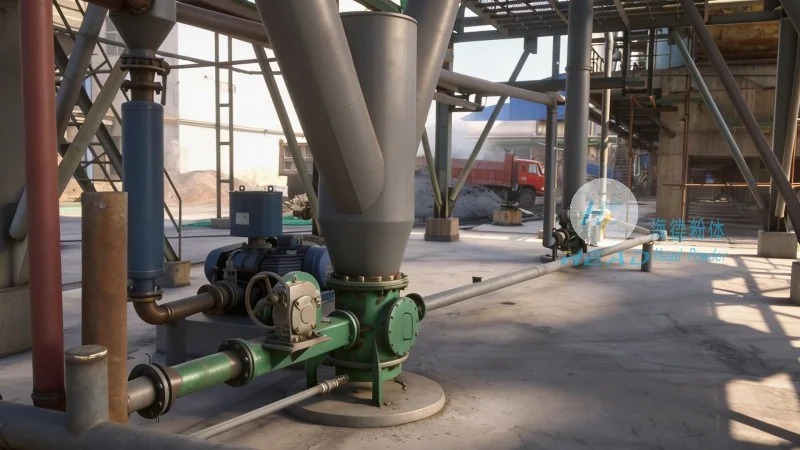
In summary, the coffee pneumatic conveying system device is a sophisticated piece of equipment that plays a vital role in modern coffee processing. Its design principles, centered on efficient air flow, material integrity, and hygiene, ensure reliable operation in food processing environments. Companies like Shandong HeadPowder Engineering Co., Ltd. contribute to the industry by providing high-quality, customized solutions that meet the specific demands of coffee production. By understanding the core design principles and benefits of such systems, coffee processing facilities can optimize their operations and maintain the highest standards of product quality.