

What is a Tonne Bag Unloading Station Pneumatic Conveying System Equipment? What is its Design Princ
For industrial facilities dealing with bulk material handling, efficient and reliable equipment is crucial. The tonne bag unloading station pneumatic conveying system equipment is a specialized solution designed to streamline the process of handling large quantities of bulk materials from tonne bags. This system integrates advanced engineering principles to ensure safe, effective, and automated material transfer, making it an essential component in modern material handling operations.
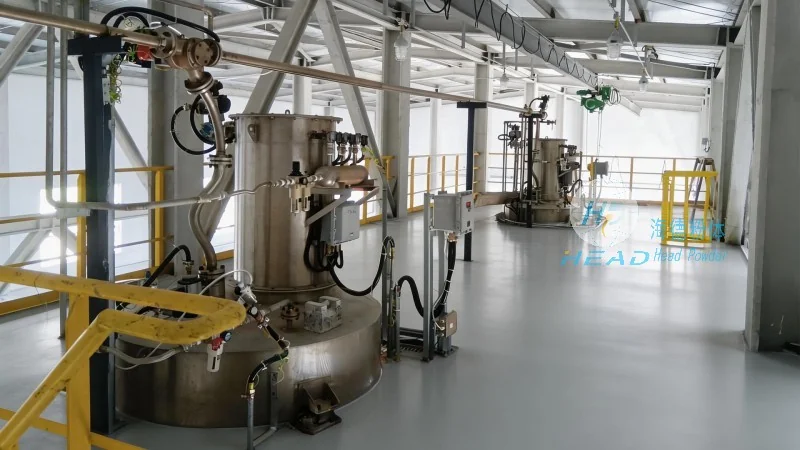
Key Components of the Tonne Bag Unloading Station Pneumatic Conveying System
The system comprises several critical components that work in harmony to achieve optimal performance. At the core is the unloading station, which is equipped with a hopper and a pneumatic conveying unit. The hopper is designed to receive the tonne bag, and the pneumatic conveying system uses air pressure to transport the material from the hopper to the storage or processing area. Other key components include the bag opening mechanism, which safely and efficiently opens the tonne bag without damaging the material inside, and the material feed system that ensures a consistent flow of material into the conveying line.
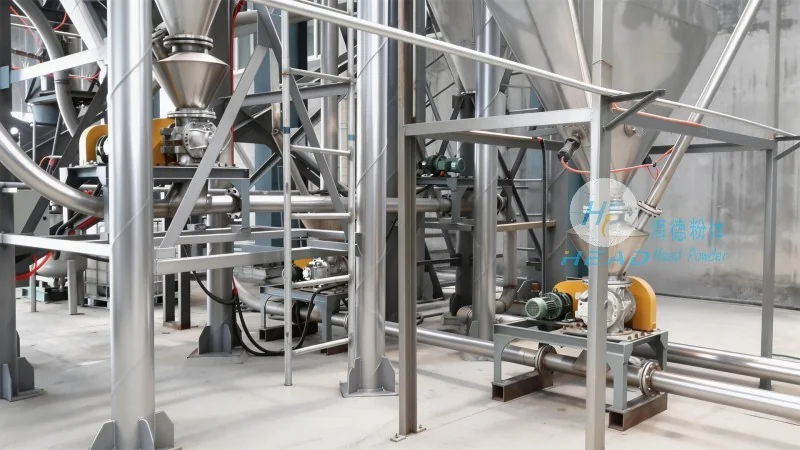
Design Principles Behind the Tonne Bag Unloading Station Pneumatic Conveying System
The design of this system is guided by several fundamental principles aimed at maximizing efficiency, safety, and durability. One of the primary principles is the use of positive pressure pneumatic conveying, which ensures that the material is transported under controlled air pressure, minimizing material degradation and ensuring a clean transfer process. Another key principle is the integration of automated controls, which allow for real-time monitoring and adjustment of the system parameters, such as air pressure and flow rate, to maintain optimal performance. The system also incorporates robust material handling components, such as high-quality hoppers and conveying pipes, which are designed to withstand the rigors of continuous operation and handle a wide range of bulk materials, including powders, granules, and pellets.
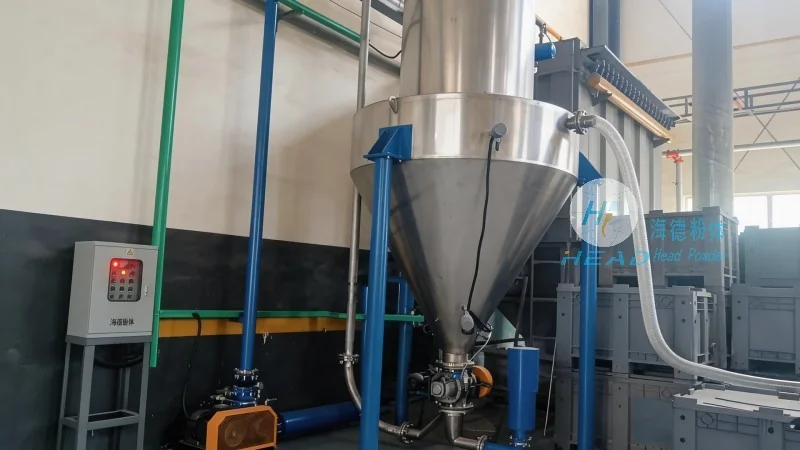
Advantages of the Tonne Bag Unloading Station Pneumatic Conveying System
Implementing a tonne bag unloading station pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly improves operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing downtime. Secondly, the system enhances safety by eliminating the need for workers to handle heavy tonne bags manually, reducing the risk of injuries and accidents. Thirdly, the system ensures a clean and hygienic transfer of materials, which is particularly important for food and pharmaceutical industries where contamination control is critical. Additionally, the system is highly versatile and can be customized to handle various types of bulk materials, making it suitable for a wide range of applications.

Application Scenarios and Industries
The tonne bag unloading station pneumatic conveying system is widely used in various industries that rely on bulk material handling. Common applications include the chemical industry, where it is used to handle chemicals and raw materials; the food and beverage industry, where it is used to process ingredients and finished products; the pharmaceutical industry, where it is used to handle active pharmaceutical ingredients (APIs) and other sensitive materials; and the mining industry, where it is used to transport minerals and ores. The system is also suitable for other industries, such as agriculture and construction, where bulk materials need to be efficiently transferred from storage to processing areas.