

What is a Sulfamethanamine Pneumatic Conveyor? What is its Design Principle?
Sulfamethanamine, a widely used ammonium sulfate fertilizer, is often transported using pneumatic conveyors. These systems are integral to industrial and agricultural operations, providing an efficient method for moving bulk materials. A pneumatic conveyor operates by utilizing air pressure to transport material through a pipeline, offering advantages such as reduced dust generation, minimal mechanical wear, and the ability to cover long distances without complex infrastructure. This technology is particularly valuable for handling materials like sulfamethanamine, which requires careful handling to maintain its quality and effectiveness.
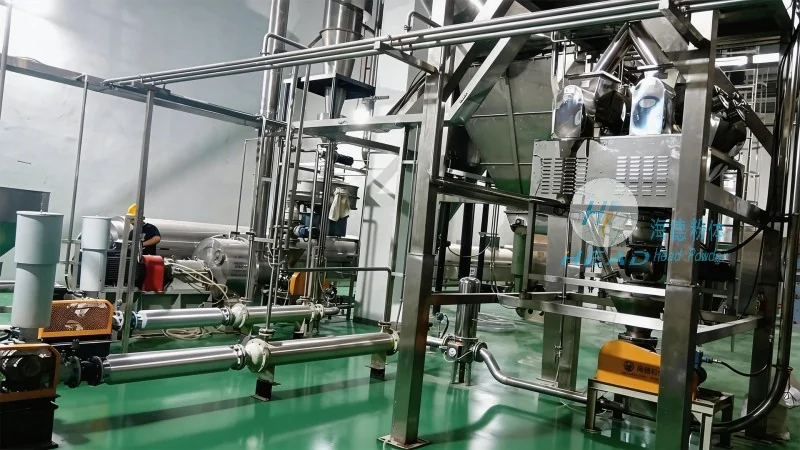
Design Principles of Sulfamethanamine Pneumatic Conveyors
The design of a sulfamethanamine pneumatic conveyor is built on several critical principles to ensure optimal performance and reliability. First, the system must accommodate the specific physical properties of ammonium sulfate, including its particle size distribution, density, and flow characteristics. Engineers design the hopper, feeder, and pipeline to handle these parameters, ensuring smooth material transfer. Second, the air pressure system is a core component; it must generate sufficient force to move the material while maintaining energy efficiency. This involves selecting the appropriate blower or compressor, which provides the right air volume and pressure to achieve consistent transport. Third, the conveyor's layout is carefully planned to minimize blockages and ensure consistent flow. The use of bends, elbows, and expansion joints in the pipeline is calculated to prevent material buildup and maintain a smooth operation. Additionally, safety features such as pressure relief valves and dust collection systems are integrated to protect both the equipment and the environment from potential hazards.
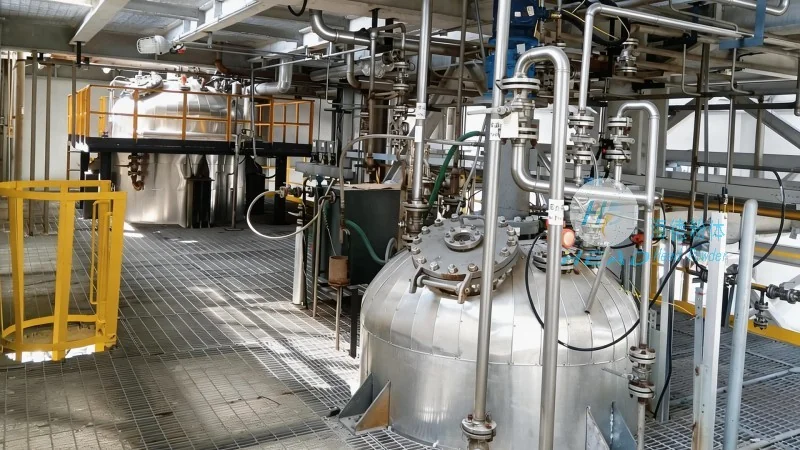
HeadPowder: Your Trusted Manufacturer and Supplier
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading provider of industrial equipment, specializing in pneumatic conveyors for bulk material handling. With decades of experience in the industry, HeadPowder has established itself as a trusted partner for clients in agriculture, chemical processing, and other sectors. The company's commitment to quality and innovation ensures that its products meet the highest standards of performance and durability. HeadPowder's team of skilled engineers and technicians work closely with clients to understand their unique requirements and deliver tailored solutions. The company's manufacturing facilities are equipped with advanced technology and rigorous quality control measures, guaranteeing that every product is built to last. HeadPowder's reputation is built on its ability to deliver reliable, efficient, and cost-effective conveyors that enhance operational efficiency and reduce downtime for its clients.
Key Features and Benefits of Sulfamethanamine Pneumatic Conveyors by HeadPowder
HeadPowder's sulfamethanamine pneumatic conveyors are engineered with several key features that enhance functionality and user experience. One of the primary benefits is the ability to transport materials in a dust-free environment, which is crucial for preserving product quality and ensuring worker safety. The conveyor's design minimizes material degradation and loss, maintaining the integrity of the sulfamethanamine throughout the transport process. Another significant advantage is the system's flexibility, allowing seamless integration into existing production lines or use as a standalone unit. The conveyors are also designed for easy installation and maintenance, with modular components that can be replaced or upgraded as needed. HeadPowder's products are constructed from durable materials and robust components, capable of withstanding the harsh conditions of industrial environments. The system is energy-efficient, reducing operational costs for clients while maintaining high performance. Additionally, the compact design saves valuable space in facilities, making it suitable for both large-scale and small-scale operations. Advanced control systems enable precise monitoring and adjustment of the conveyor's operation, ensuring optimal performance at all times.
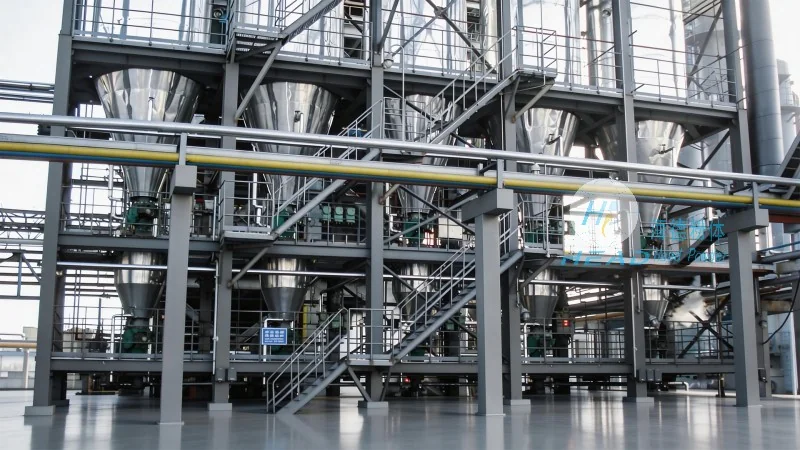
Applications and Use Cases
Sulfamethanamine pneumatic conveyors are widely utilized in various industries, with a strong presence in the agricultural sector for fertilizer distribution. They are also employed in chemical processing plants where bulk materials need to be transported between different stages of production. The system's capacity to handle large volumes of material efficiently makes it ideal for high-demand applications. In addition, the conveyors are used in food processing and pharmaceutical industries where maintaining product purity is paramount. The versatility of the system allows it to be adapted for different materials and applications, making it a valuable asset for any operation requiring bulk material transport. HeadPowder's solutions are tailored to meet the specific needs of each client, ensuring that the conveyor system is optimized for their unique operational requirements.