

What is a cement particle pneumatic conveyor? What are its design principles?
A cement particle pneumatic conveyor is an advanced industrial system engineered to transport bulk cement and other fine particulate materials through a sealed pipeline using compressed air. This technology revolutionizes material handling by eliminating the need for mechanical components like belts or screws, offering a dust-free, efficient, and flexible solution for various industrial applications. The system typically comprises several key components: a material hopper for storage, a high-efficiency blower or air compressor to generate the necessary airflow, a pipeline network that transports the cement particles, and a control system to regulate the conveying process. By utilizing air as the conveying medium, the system ensures minimal product degradation, reduces operational costs through lower maintenance requirements, and enhances workplace safety by containing dust and particles within the system.
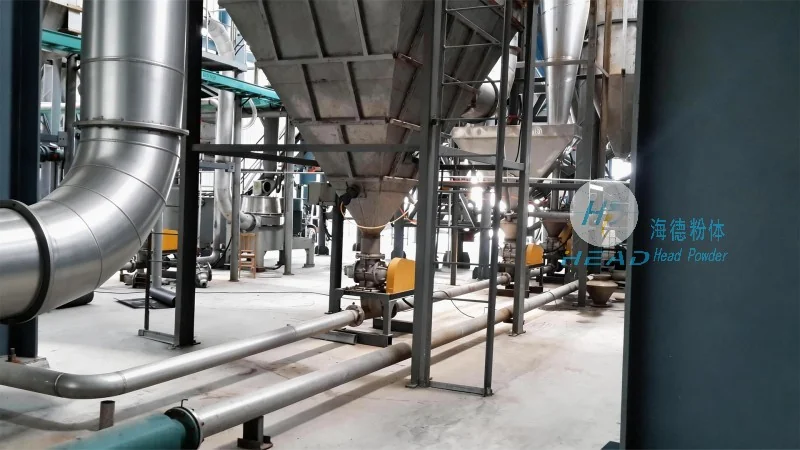
Key Design Principles of Cement Particle Pneumatic Conveyors
The design of a cement particle pneumatic conveyor is guided by several critical principles to ensure optimal performance, reliability, and efficiency. First, the system must maintain a consistent and sufficient airflow to overcome the resistance of the material particles in the pipeline. This is achieved through the use of high-performance blowers that can generate the required pressure and volume of air, often ranging from low to high pressure depending on the material characteristics and conveying distance. Second, the pipeline design is paramount, as it must be sized appropriately to handle the specific properties of the cement particles, such as their size distribution, density, and moisture content. The pipeline is typically constructed from materials like stainless steel or corrosion-resistant plastic to prevent degradation and ensure durability under harsh operating conditions. Third, the system incorporates advanced control mechanisms to regulate the flow rate and pressure, allowing for precise control over the conveying process. These controls may include pressure sensors, flow meters, and variable frequency drives that adjust the blower speed in real-time based on the system’s operational status. Additionally, the design considers the need for dust collection and filtration systems to maintain air quality and comply with environmental regulations, ensuring that the system operates in an environmentally friendly manner. By integrating these principles, the conveyor ensures efficient, reliable, and safe transportation of cement particles, minimizing downtime and maximizing productivity.
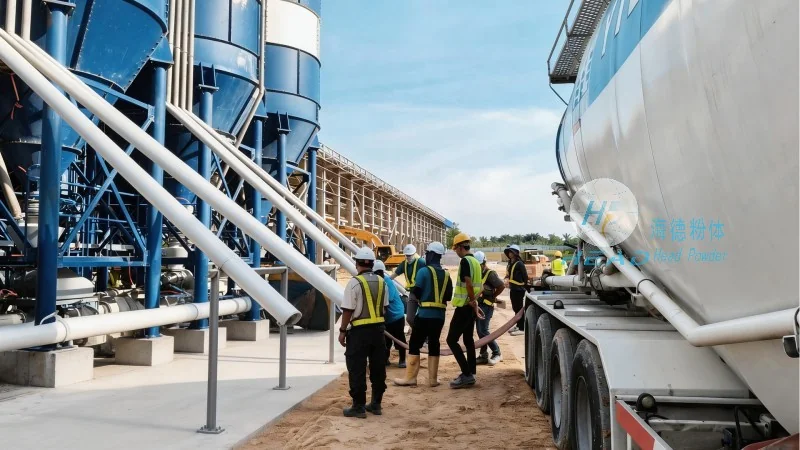
Applications and Benefits in Cement Industry
Cement particle pneumatic conveyors are extensively utilized in the cement industry for a range of applications, from raw material transport to finished product delivery. In raw material handling, the system efficiently transports limestone, clay, and other raw materials from storage silos to grinding mills, ensuring a continuous and uninterrupted supply. This process is critical for maintaining the production line’s efficiency and reducing bottlenecks. For finished product delivery, the conveyor transports packaged or bulk cement to storage facilities, distribution centers, or construction sites, reducing the need for manual handling and minimizing product damage. The benefits of using pneumatic conveyors in cement processing are significant: improved operational efficiency through automated material handling, reduced labor costs due to fewer manual operations, enhanced safety by containing dust and particles within the system, and lower environmental impact by minimizing dust emissions. The flexibility of the system allows for easy integration into existing production lines and can be adapted to different plant layouts and operational requirements, making it a versatile solution for various industrial needs.
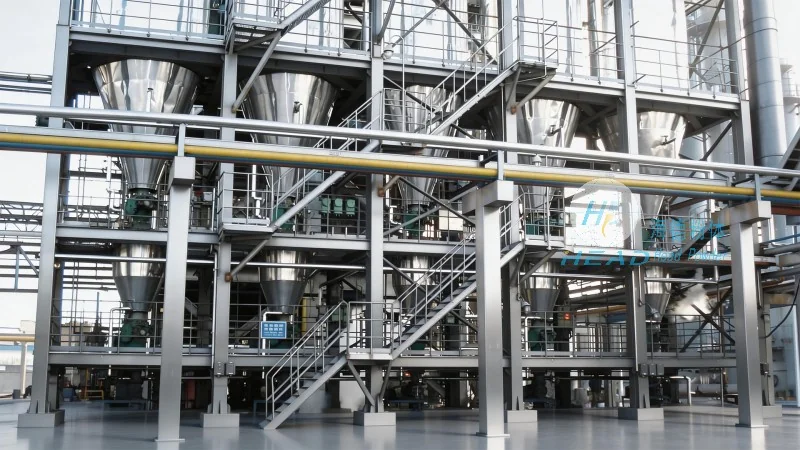
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a prominent manufacturer and supplier of industrial material handling equipment, specializing in cement particle pneumatic conveyors. With its headquarters located in Shandong, China, HeadPowder has built a strong reputation as a trusted partner for businesses in the cement and related industries. The company focuses on designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of its clients. HeadPowder’s products are recognized for their durability, efficiency, and reliability, meeting the stringent requirements of modern industrial operations. The company’s commitment to innovation and customer satisfaction has enabled it to serve a diverse clientele, including small-scale cement producers and large-scale industrial facilities. HeadPowder operates a state-of-the-art manufacturing facility equipped with advanced technology and a skilled workforce, ensuring that its products meet the highest standards of quality and performance. The company continues to invest in research and development to enhance its product line and stay competitive in the market, providing customized solutions that address the unique challenges faced by its clients. HeadPowder’s expertise in pneumatic conveying technology has made it a leader in the industry, offering reliable and efficient solutions for material handling in the cement sector.