

What is Organic Fertilizer Pneumatic Conveying Equipment? An Introduction to the Structure and Princ
Organic fertilizer pneumatic conveying equipment is a specialized system designed to handle and transport bulk organic materials efficiently. This technology is crucial in the agricultural and fertilizer industries, enabling the safe and reliable movement of organic fertilizers from storage to processing or application sites. The equipment operates on the principle of pneumatic conveying, utilizing air flow to transport powders or granules through a pipeline network.
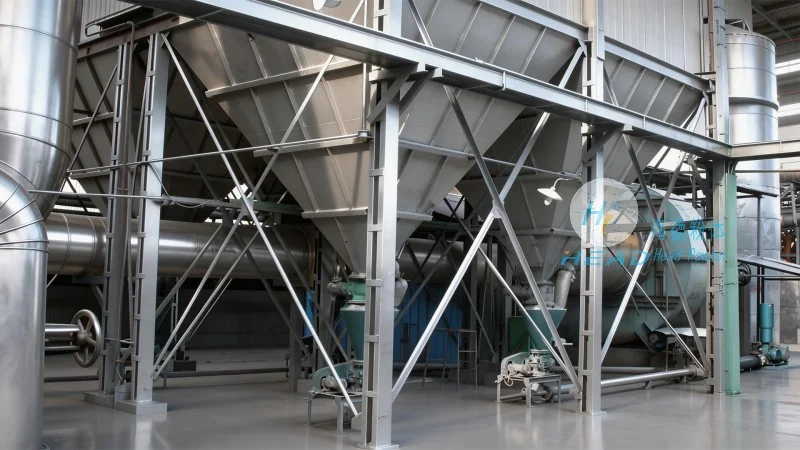
Key Components and Structure of Pneumatic Conveying Systems
The core structure of organic fertilizer pneumatic conveying equipment typically includes several essential components that work in tandem to ensure smooth operation. The main parts are the material hopper, which holds the organic fertilizer; the air compressor or blower that generates the necessary air pressure; the conveying pipeline, which transports the material; and the control system that regulates the flow and pressure. Additionally, the system may incorporate components such as rotary valves, filters, and dust collectors to manage material flow and maintain air quality.
Working Principle of Pneumatic Conveying
The operation of organic fertilizer pneumatic conveying equipment relies on the creation of a pressure differential within the conveying line. The air compressor draws in ambient air and compresses it, increasing the air pressure inside the pipeline. As the organic fertilizer is introduced into the hopper, it is drawn into the pipeline by the moving air stream. The air and material mixture travels through the pipeline to the discharge point, where the material is separated from the air and collected. The air is then filtered and recycled back into the system, minimizing waste and energy consumption.
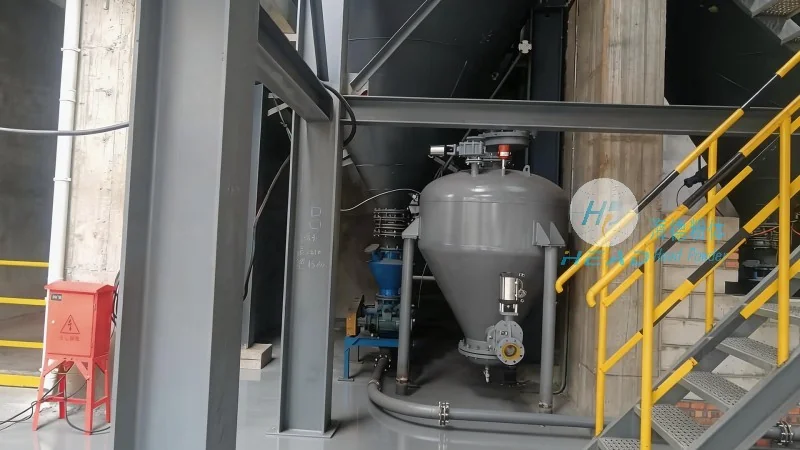
Advantages of Pneumatic Conveying for Organic Fertilizers
Compared to traditional mechanical conveying methods, organic fertilizer pneumatic conveying offers several advantages. It provides a dust-free and hygienic environment, which is critical for maintaining the quality of organic fertilizers. The system also allows for continuous and automated operation, reducing labor costs and increasing productivity. Furthermore, pneumatic conveying can handle a wide range of particle sizes and moisture contents, making it versatile for various organic fertilizer types. The equipment is also relatively compact, saving space in processing facilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder handling and conveying solutions. With headquarters located in Shandong, China, the company specializes in designing and producing customized pneumatic conveying systems tailored to the specific needs of the fertilizer industry. HeadPowder's expertise lies in integrating cutting-edge technology with practical engineering solutions to deliver reliable and efficient equipment for organic fertilizer processing and transportation.
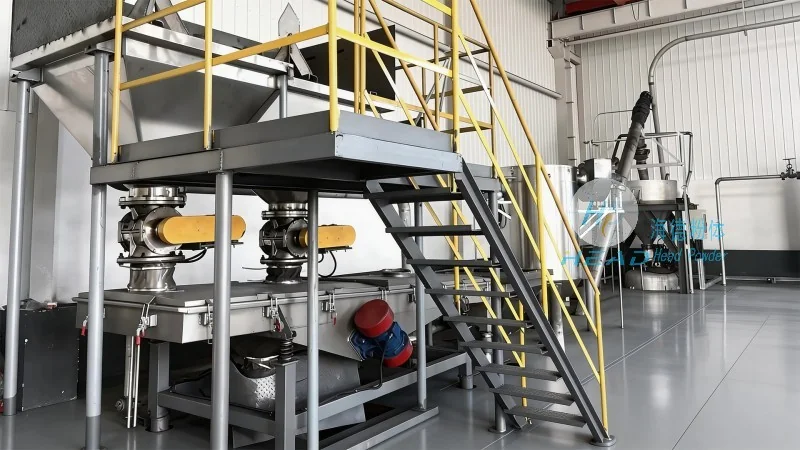
Customization and Application in Fertilizer Production
Organic fertilizer pneumatic conveying equipment from headpowder is designed to meet the diverse requirements of fertilizer manufacturers. The systems can be customized in terms of capacity, material handling capabilities, and integration with existing production lines. Whether for small-scale organic fertilizer production or large industrial facilities, the equipment ensures consistent and efficient material transport. The company's engineering team works closely with clients to understand their operational needs and develop solutions that enhance productivity while maintaining product quality and safety standards.
Quality Assurance and Maintenance
HeadPowder places a strong emphasis on quality assurance throughout the manufacturing process. All components of the pneumatic conveying systems are manufactured using high-quality materials and undergo rigorous testing to ensure durability and performance. The company provides comprehensive maintenance and support services to ensure the long-term reliability of the equipment. Regular maintenance, including filter cleaning and component inspections, is recommended to maintain optimal operation and extend the lifespan of the system.