

Coke Powder Pneumatic Conveying Technology: Principles, Applications, and Development Trends
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for coke powder. This technology is crucial in modern industrial processes, enabling efficient and safe material transport. The following sections explore the fundamental principles, practical applications, and emerging trends in coke powder pneumatic conveying.
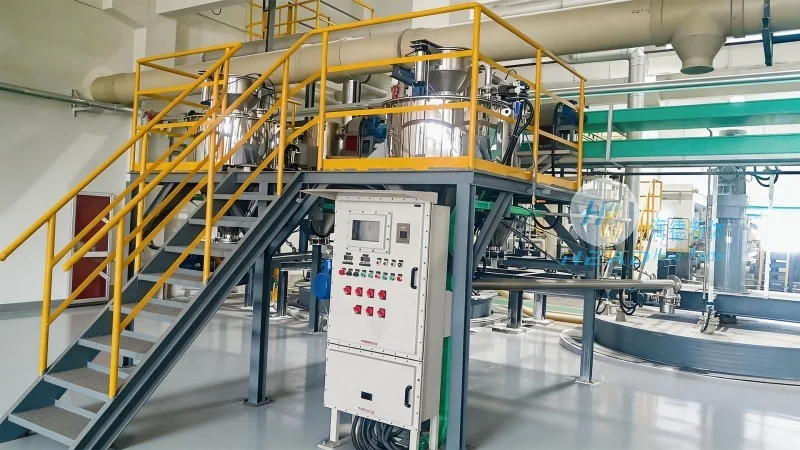
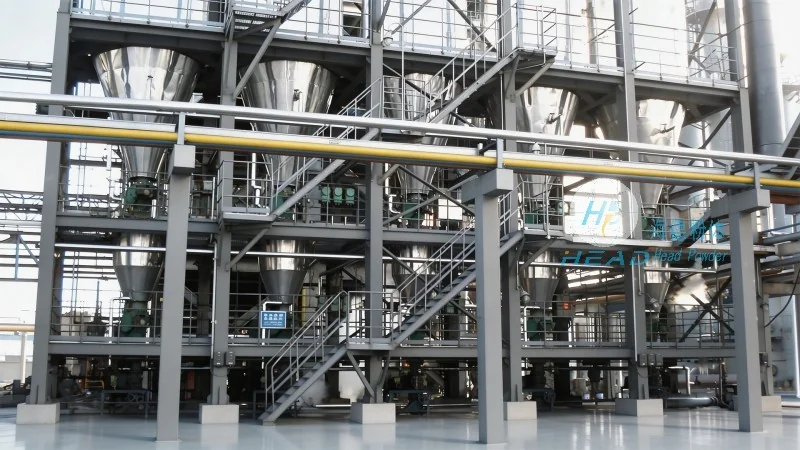
Principles of Pneumatic Conveying for Coke Powder
The core principle of pneumatic conveying involves transporting solid particles, such as coke powder, using a gas stream. This method relies on the interaction between the gas flow and the powder particles to achieve movement. There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use high-velocity air to suspend particles, suitable for long-distance and high-capacity transport. Dense-phase systems, on the other hand, employ lower velocities and higher pressure to move particles in a more compact state, reducing the risk of product degradation and equipment wear. The choice between these systems depends on factors like the particle size, moisture content, and required transport distance. For coke powder, which typically has a relatively uniform particle size and moderate moisture levels, both systems can be effective, but dense-phase often offers advantages in preserving product quality and minimizing system wear.
Applications in Industrial Settings
Coke powder pneumatic conveying technology is widely applied across various industrial sectors. In the steel industry, it is essential for transporting coke from storage facilities to blast furnaces, where it serves as a key fuel and reducing agent. The efficiency of the conveying system directly impacts the productivity and energy consumption of the blast furnace operation. Additionally, in chemical and petrochemical plants, coke powder is used as a raw material for producing carbon black and other chemicals. The ability to handle large volumes of coke powder safely and reliably enhances the overall operational efficiency of these facilities. Another application is in the construction industry, where coke powder is used as a raw material for cement production. The pneumatic conveying system ensures that the coke powder is delivered to the mixing plants without contamination or loss, maintaining product quality. HeadPowder's expertise in customizing conveying systems to meet specific industrial requirements has made them a trusted partner for companies in these sectors.
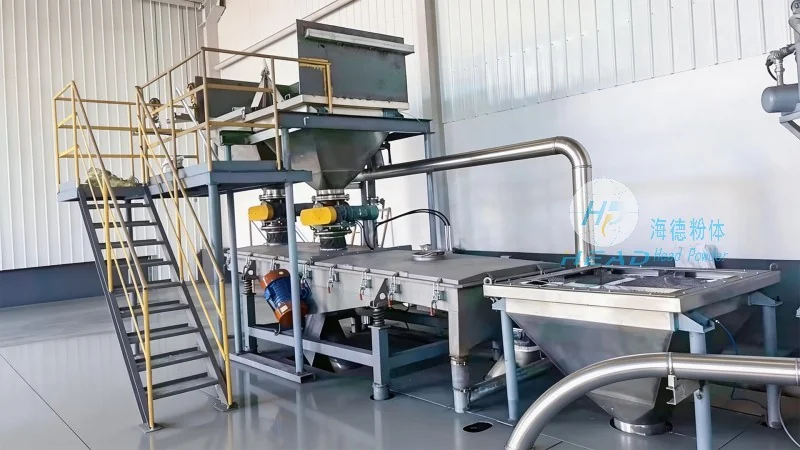
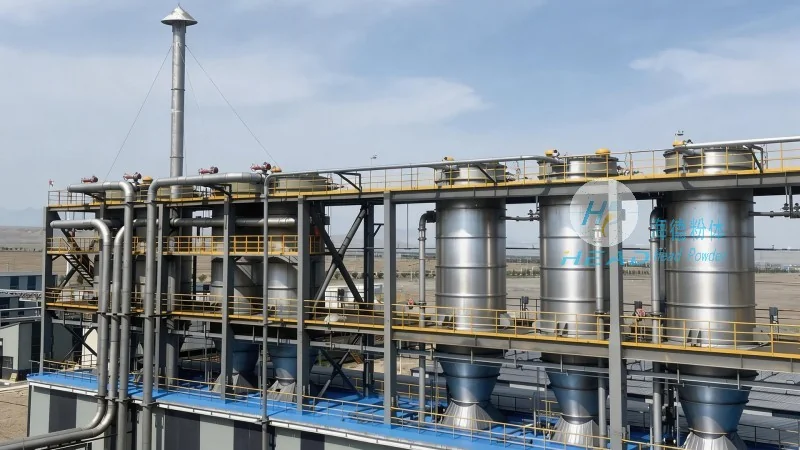
Development Trends and Future Prospects
The field of coke powder pneumatic conveying is continuously evolving, driven by technological advancements and the need for more efficient, sustainable, and reliable systems. One significant trend is the integration of automation and control systems. Modern pneumatic conveying systems now incorporate advanced sensors and control algorithms to monitor flow rates, pressure, and particle concentration in real-time. This allows for precise control and optimization of the conveying process, reducing energy consumption and minimizing downtime. Another trend is the development of more energy-efficient systems. Innovations such as variable-speed drives and optimized air flow designs help reduce the overall energy consumption of the conveying process. For example, using variable-frequency drives to adjust the air flow based on the actual demand can lead to significant energy savings. Additionally, the use of high-efficiency filters and dust collection systems improves the environmental performance of the conveying systems, reducing emissions and improving workplace safety. The adoption of sustainable materials and processes is also a key trend. Companies are increasingly focusing on reducing the environmental impact of their operations, and pneumatic conveying systems can contribute to this by minimizing the need for manual handling and reducing waste. HeadPowder is at the forefront of these developments, continuously investing in research and development to introduce new technologies and solutions that meet the evolving needs of the industry. The company's commitment to innovation and customer satisfaction has positioned them as a leader in the field of coke powder pneumatic conveying technology.