

[Borax Pneumatic Conveying Technology: Principles, Applications, and Development Trends]
HeadPowder, a leading enterprise in the field of material handling solutions, specializes in advanced pneumatic conveying systems tailored for borax processing. This article explores the fundamental principles, practical applications, and evolving trends in borax pneumatic conveying technology, providing insights into efficient material transport and processing methods.
Principles of Borax Pneumatic Conveying
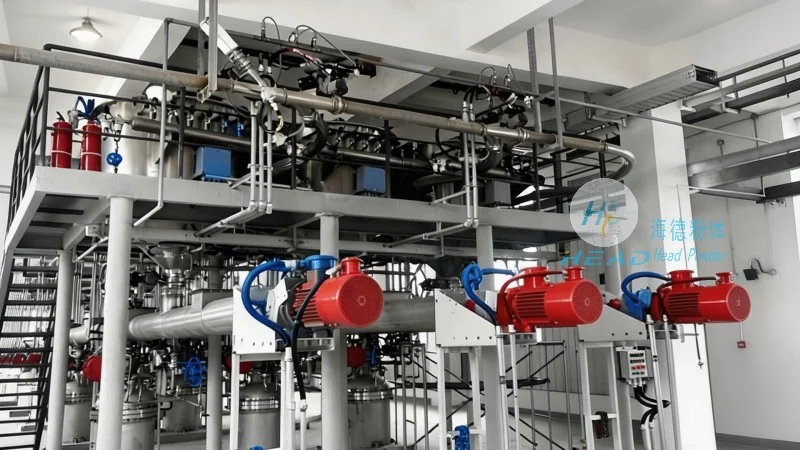
Borax pneumatic conveying technology relies on the movement of solid particles (borax) suspended in a gas stream, typically air or other suitable gases. The process can be categorized into two main types: pressure and vacuum (suction) systems. In pressure systems, compressed air is used to push the material through a pipeline, while vacuum systems utilize a vacuum to draw the material from a source. The key principles involve maintaining optimal gas velocity to prevent particle settling or blockages, ensuring consistent flow rates, and controlling pressure differentials to achieve efficient transport. Factors such as particle size, density, and moisture content significantly influence the design and operation of the conveying system, requiring precise engineering to achieve reliable performance.
Applications in Borax Processing
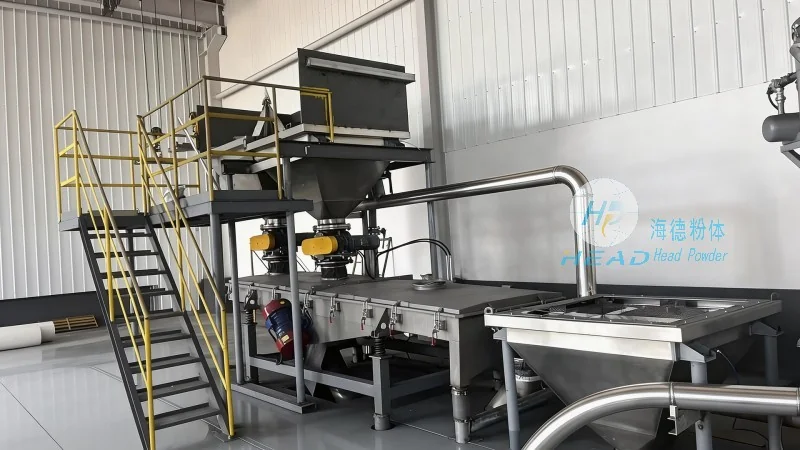
Borax, a white crystalline salt with chemical formula Na₂B₄O₇·10H₂O, is widely used in various industries including glass manufacturing, detergents, and pharmaceuticals. Pneumatic conveying systems are critical for handling borax in these applications due to its hygroscopic nature and the need for clean, dust-free transport. For instance, in glass production, borax is used as a flux to lower the melting point of silica, and pneumatic conveyors ensure precise dosing and minimal contamination. In detergent manufacturing, borax is incorporated into formulations, and efficient conveying systems maintain product integrity and prevent caking. The technology also supports bulk handling in mining and chemical processing facilities, where large volumes of borax need to be transported between storage, processing, and packaging stages. HeadPowder’s expertise in customizing conveying solutions ensures that borax is handled safely and efficiently, meeting industry standards for purity and consistency.
Development Trends and Innovations
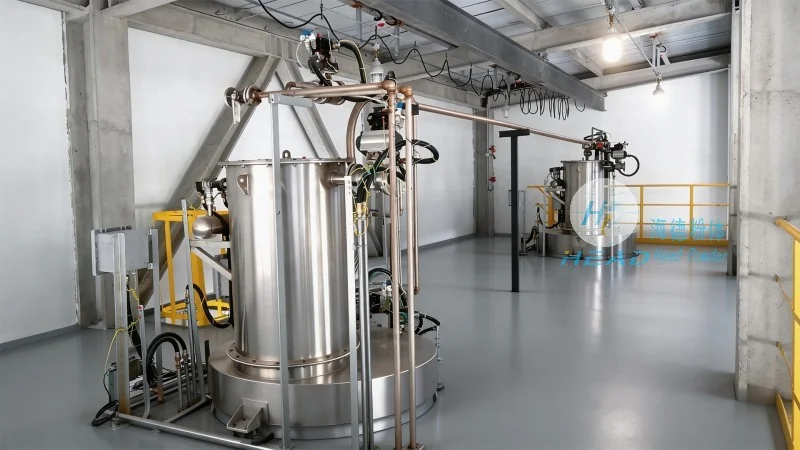
The borax pneumatic conveying industry is continuously evolving to address challenges such as energy efficiency, environmental compliance, and process automation. Recent advancements include the integration of advanced control systems that optimize air pressure and flow rates, reducing energy consumption and improving system reliability. High-efficiency cyclone separators and filter systems are now standard in modern conveying equipment, ensuring minimal dust emissions and compliance with environmental regulations. Additionally, the adoption of intelligent monitoring technologies allows real-time tracking of material flow, enabling predictive maintenance and reducing downtime. Sustainable practices are also gaining importance, with companies like Shandong HeadPowder Engineering Co., Ltd. focusing on developing eco-friendly solutions that minimize waste and energy use. The trend toward modular and scalable systems enables flexibility in adapting to changing production demands, while maintaining high performance standards. As borax continues to be a vital raw material in multiple sectors, the development of robust and efficient pneumatic conveying technologies remains a priority for industry stakeholders.
Conclusion
HeadPowder, based in Shandong, China, remains at the forefront of borax pneumatic conveying technology, offering tailored solutions that enhance operational efficiency and product quality. By understanding the principles of pneumatic transport, leveraging advanced applications, and embracing emerging trends, businesses can optimize their borax handling processes. The company’s commitment to innovation and customer-centric design ensures that borax is transported safely, reliably, and in compliance with industry requirements, supporting the growth and sustainability of borax-dependent industries worldwide.